Hydraulic Pistons, Piston Rods & Barrels
Hydraulic cylinder components in series: chrome-plated and ground piston rods, pistons, honed barrels with welded clevis eyes, and complete cylinders to your drawing.
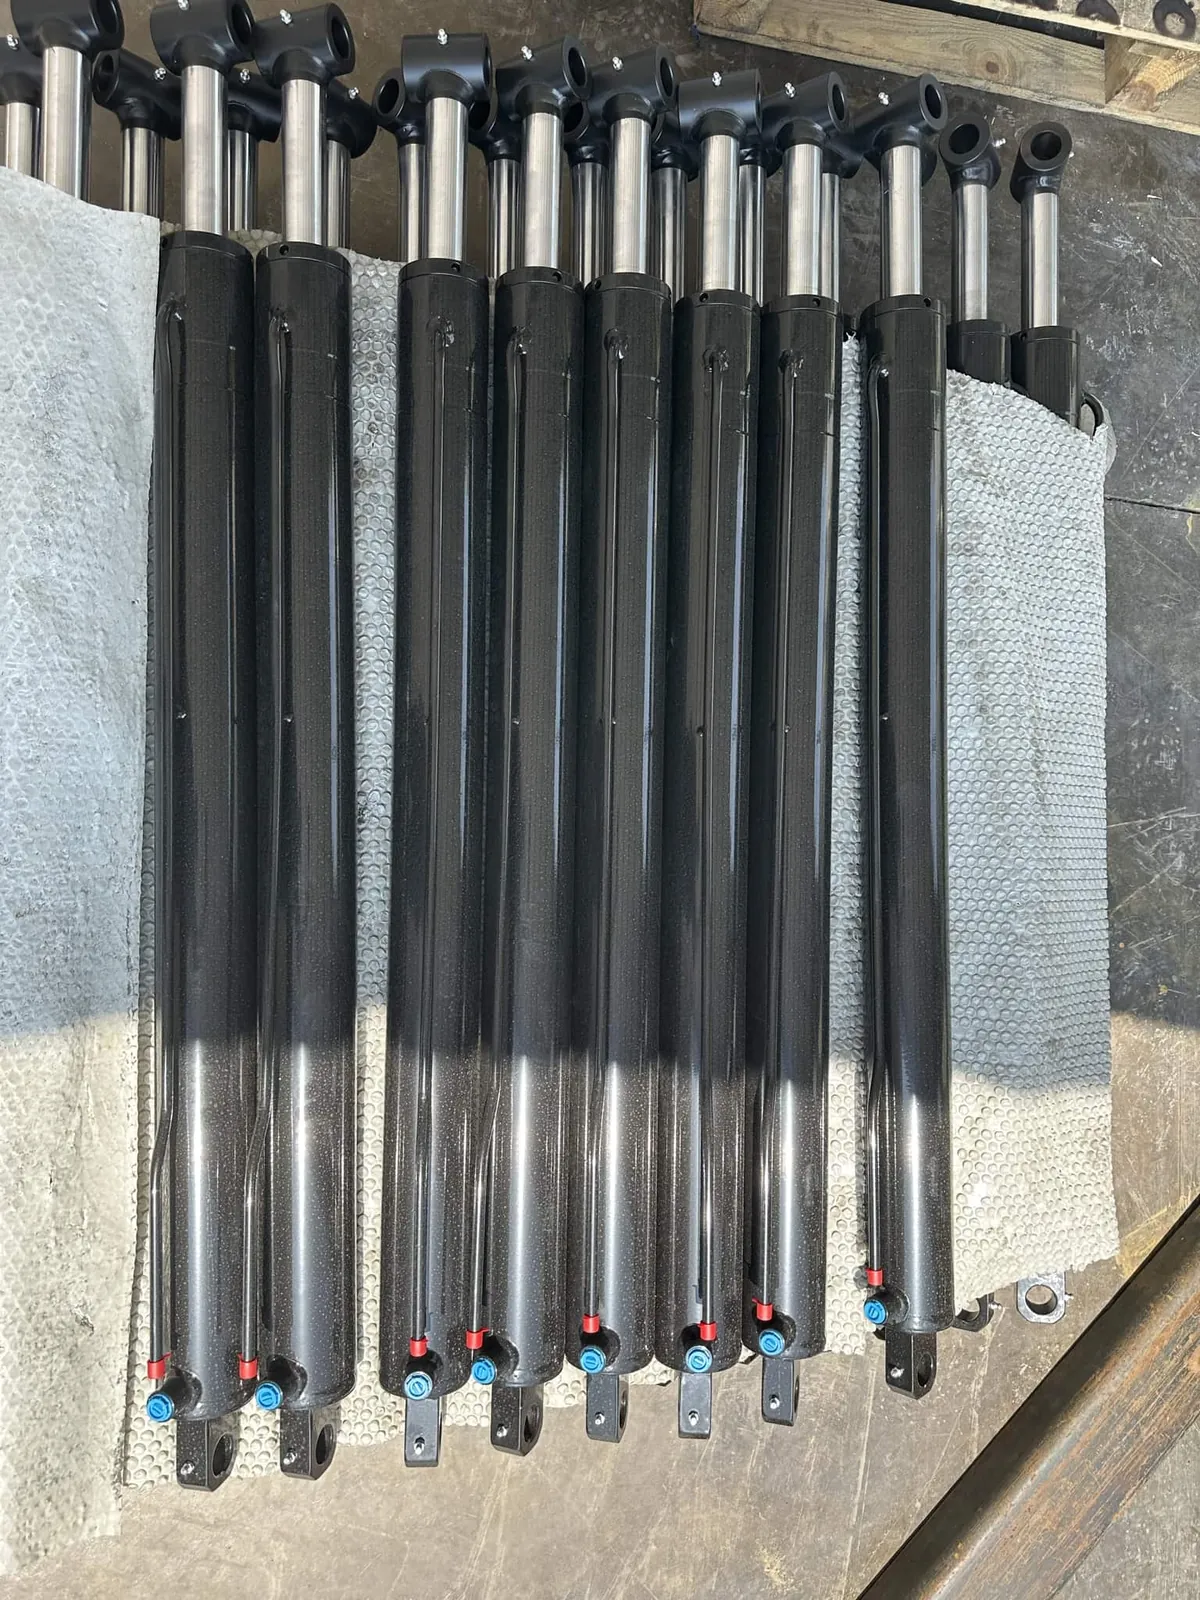
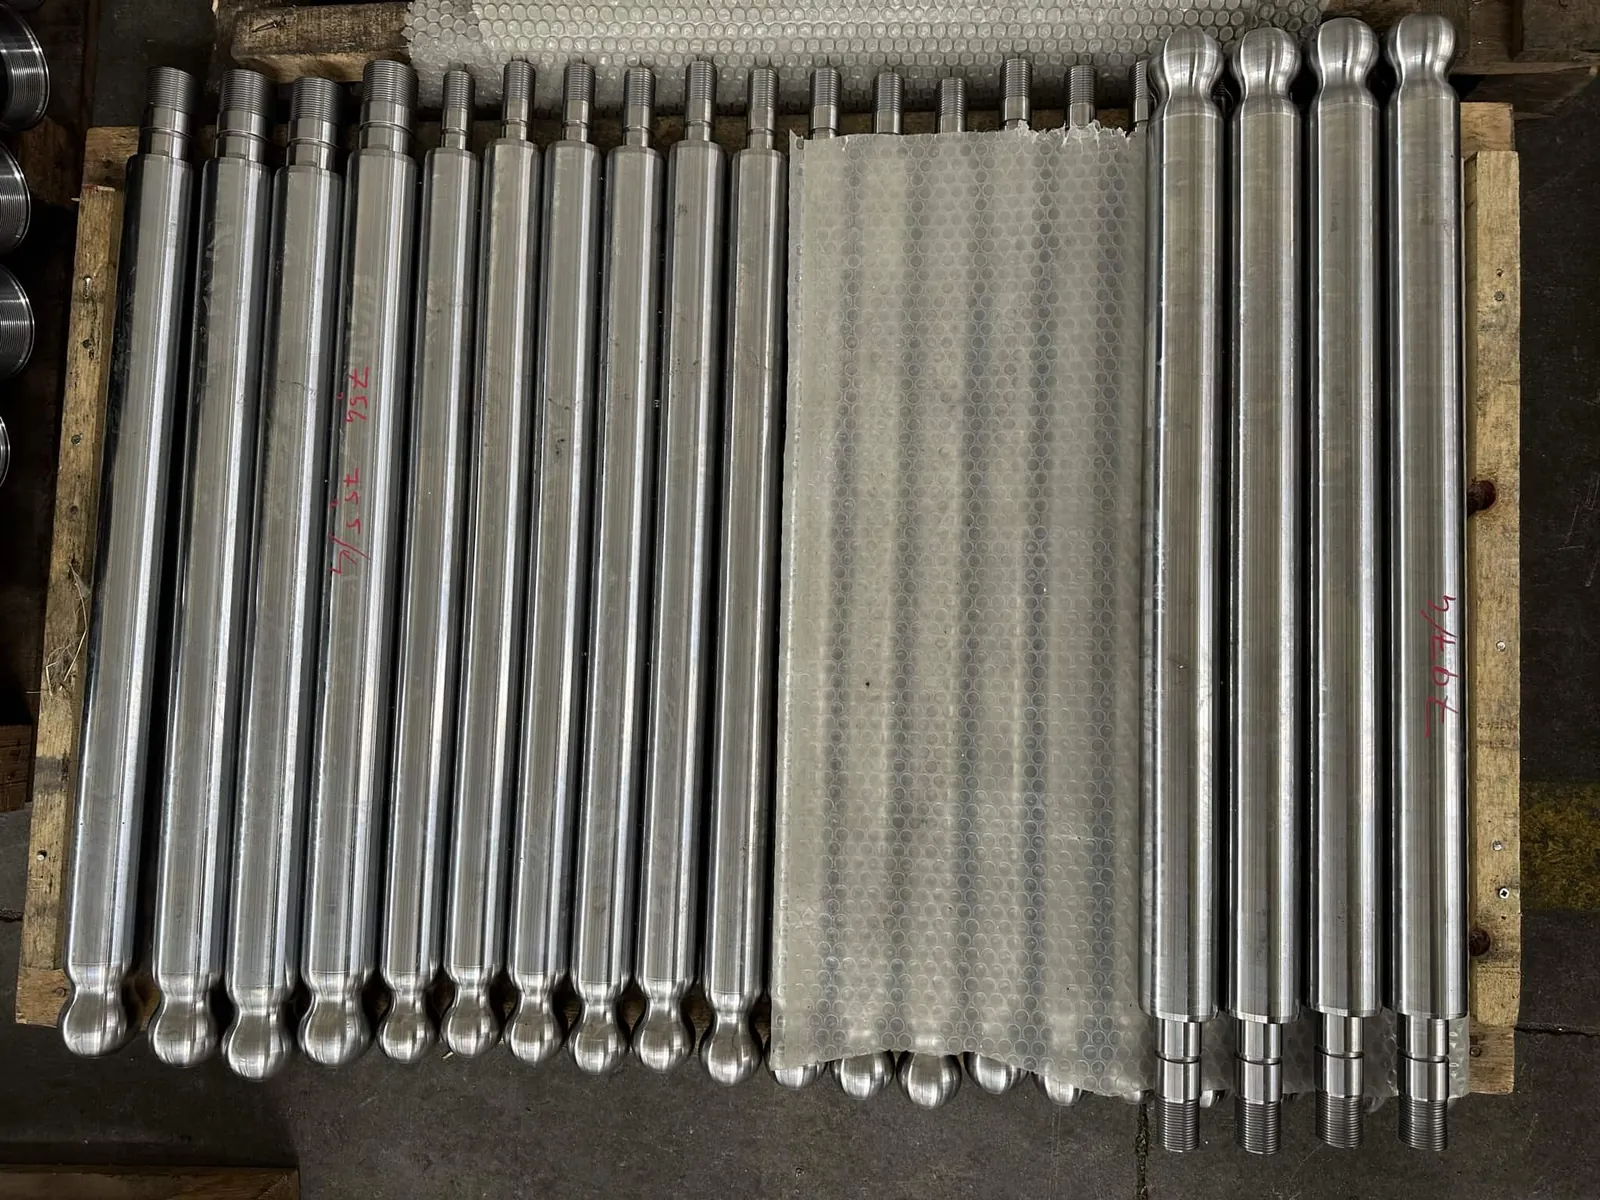
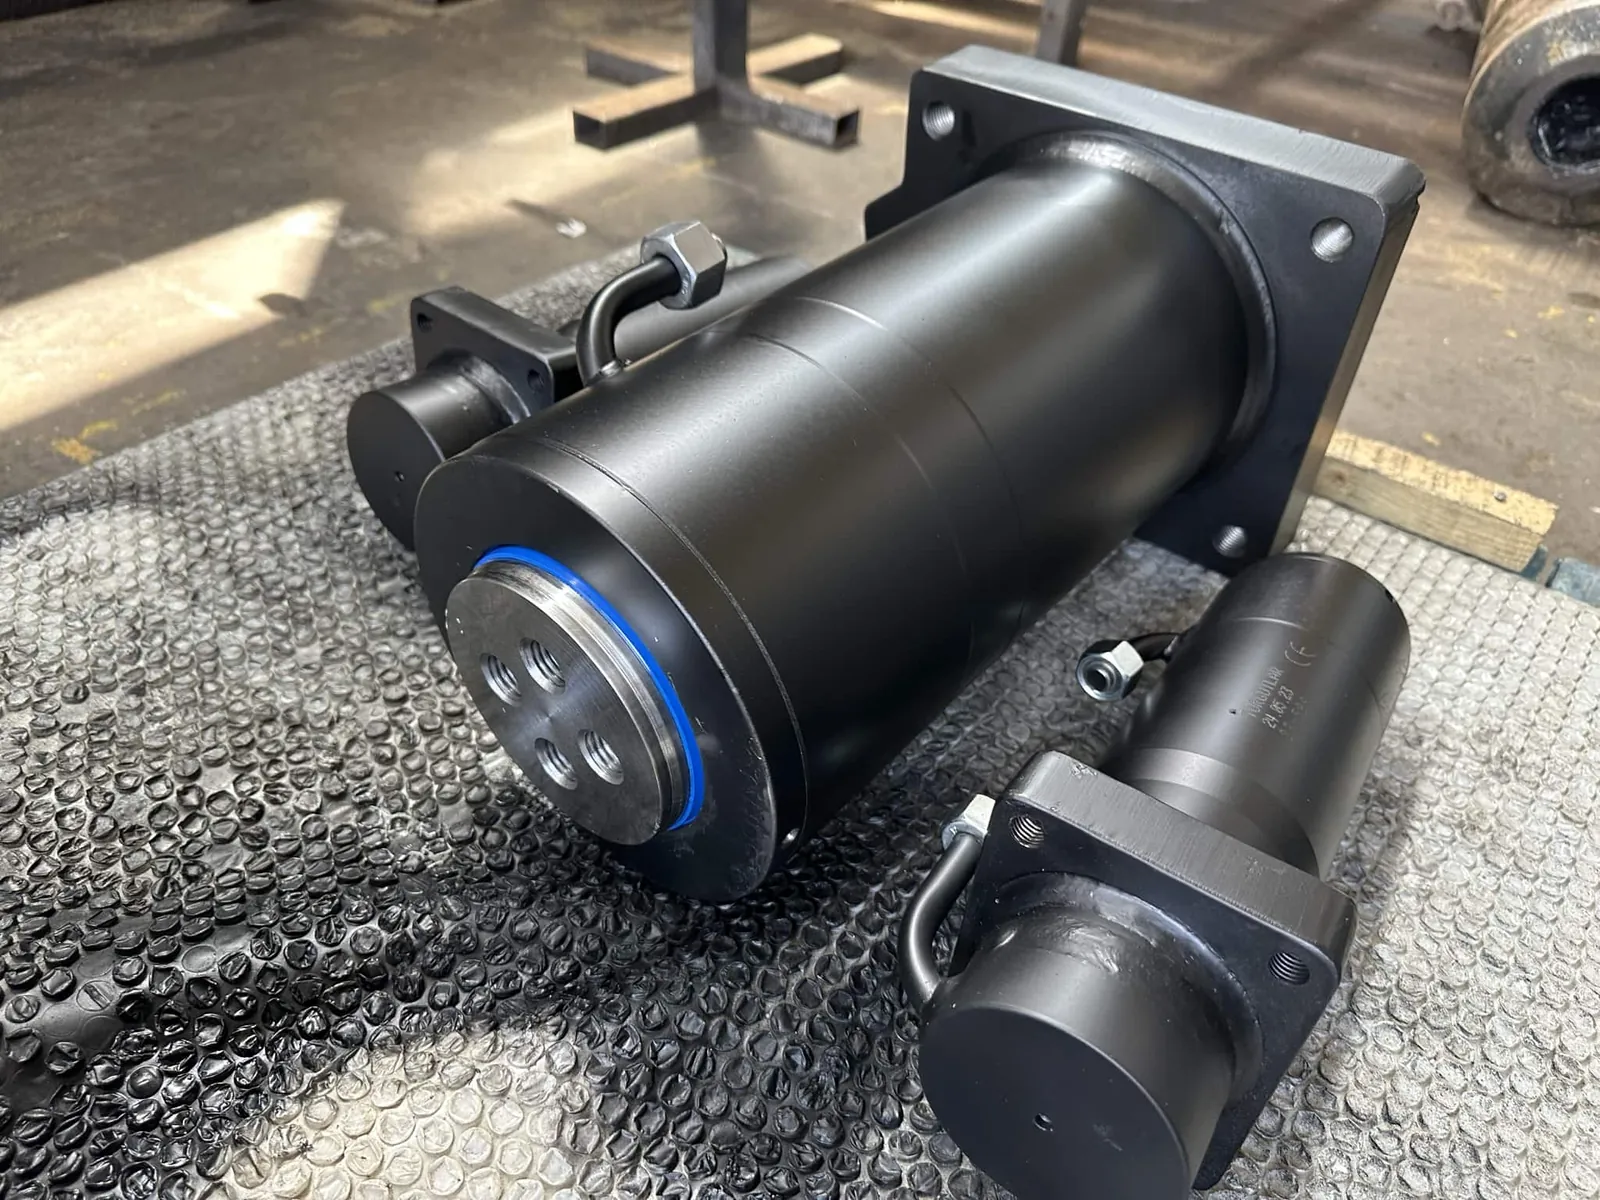
Piston Rods, Barrels and Cylinders in Series
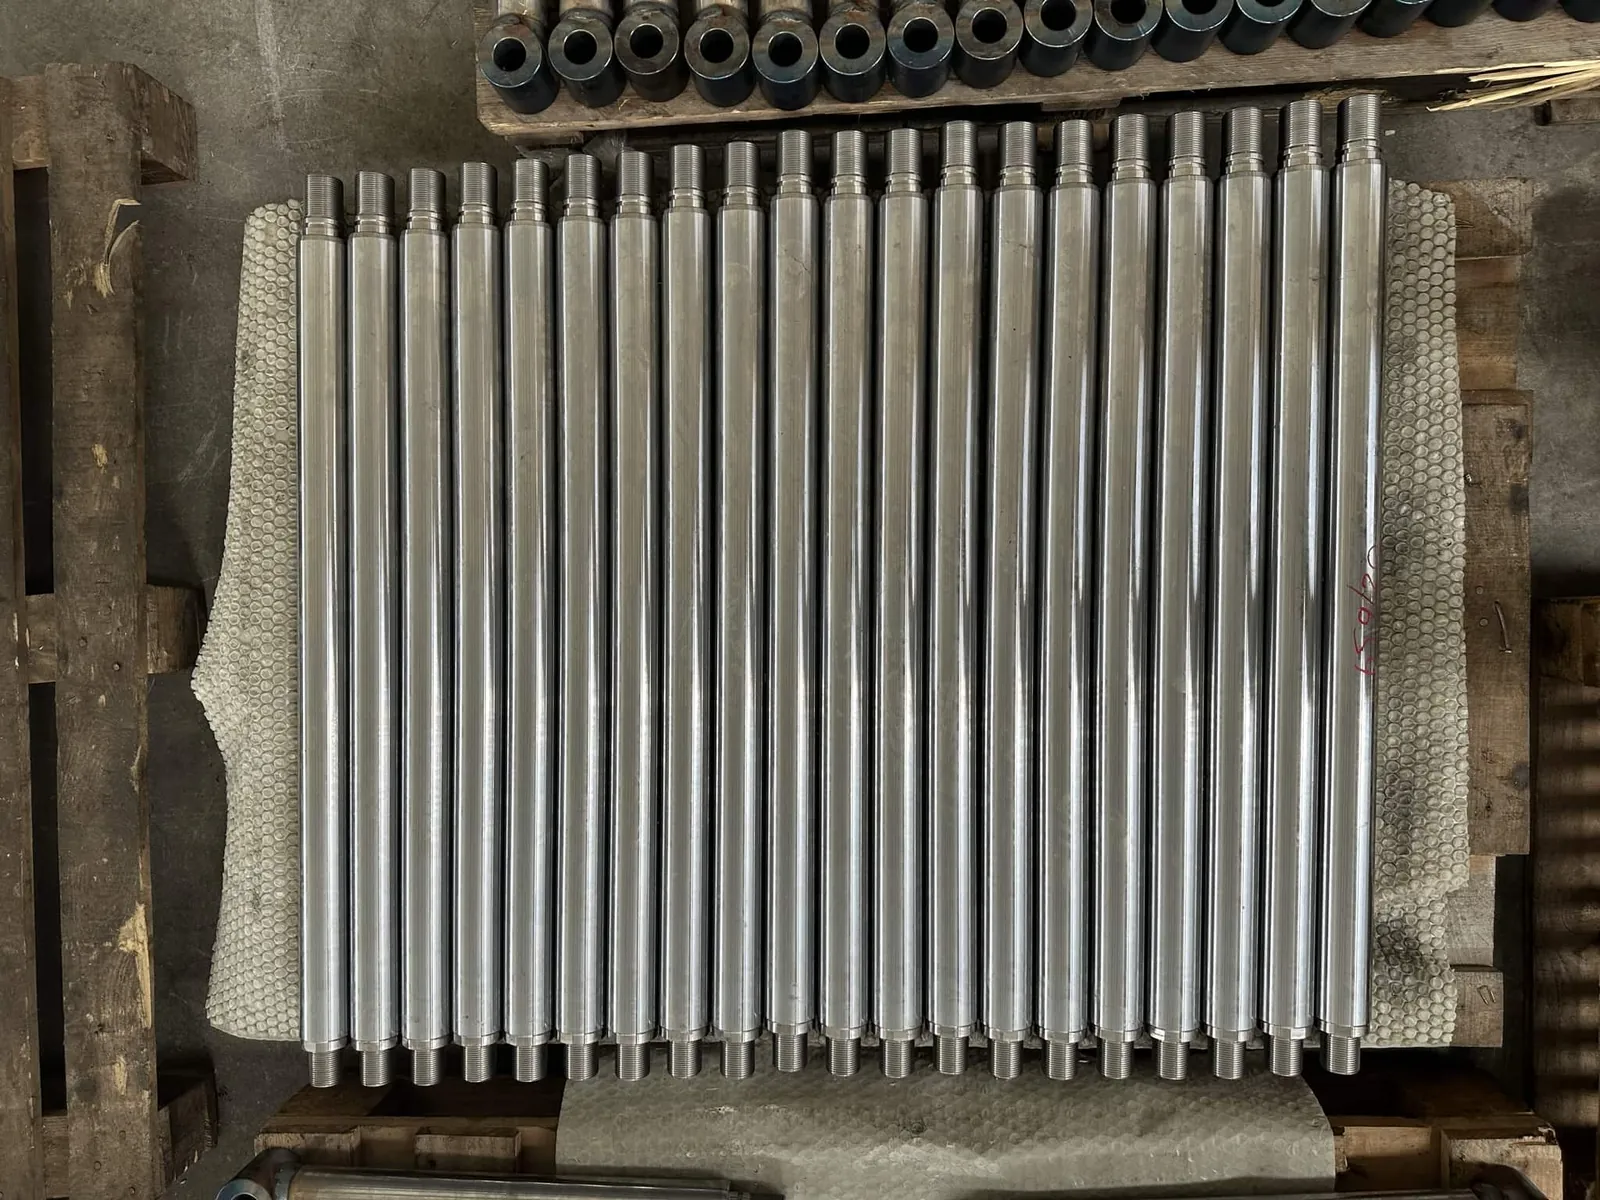
Hydraulic Cylinder Parts We Make
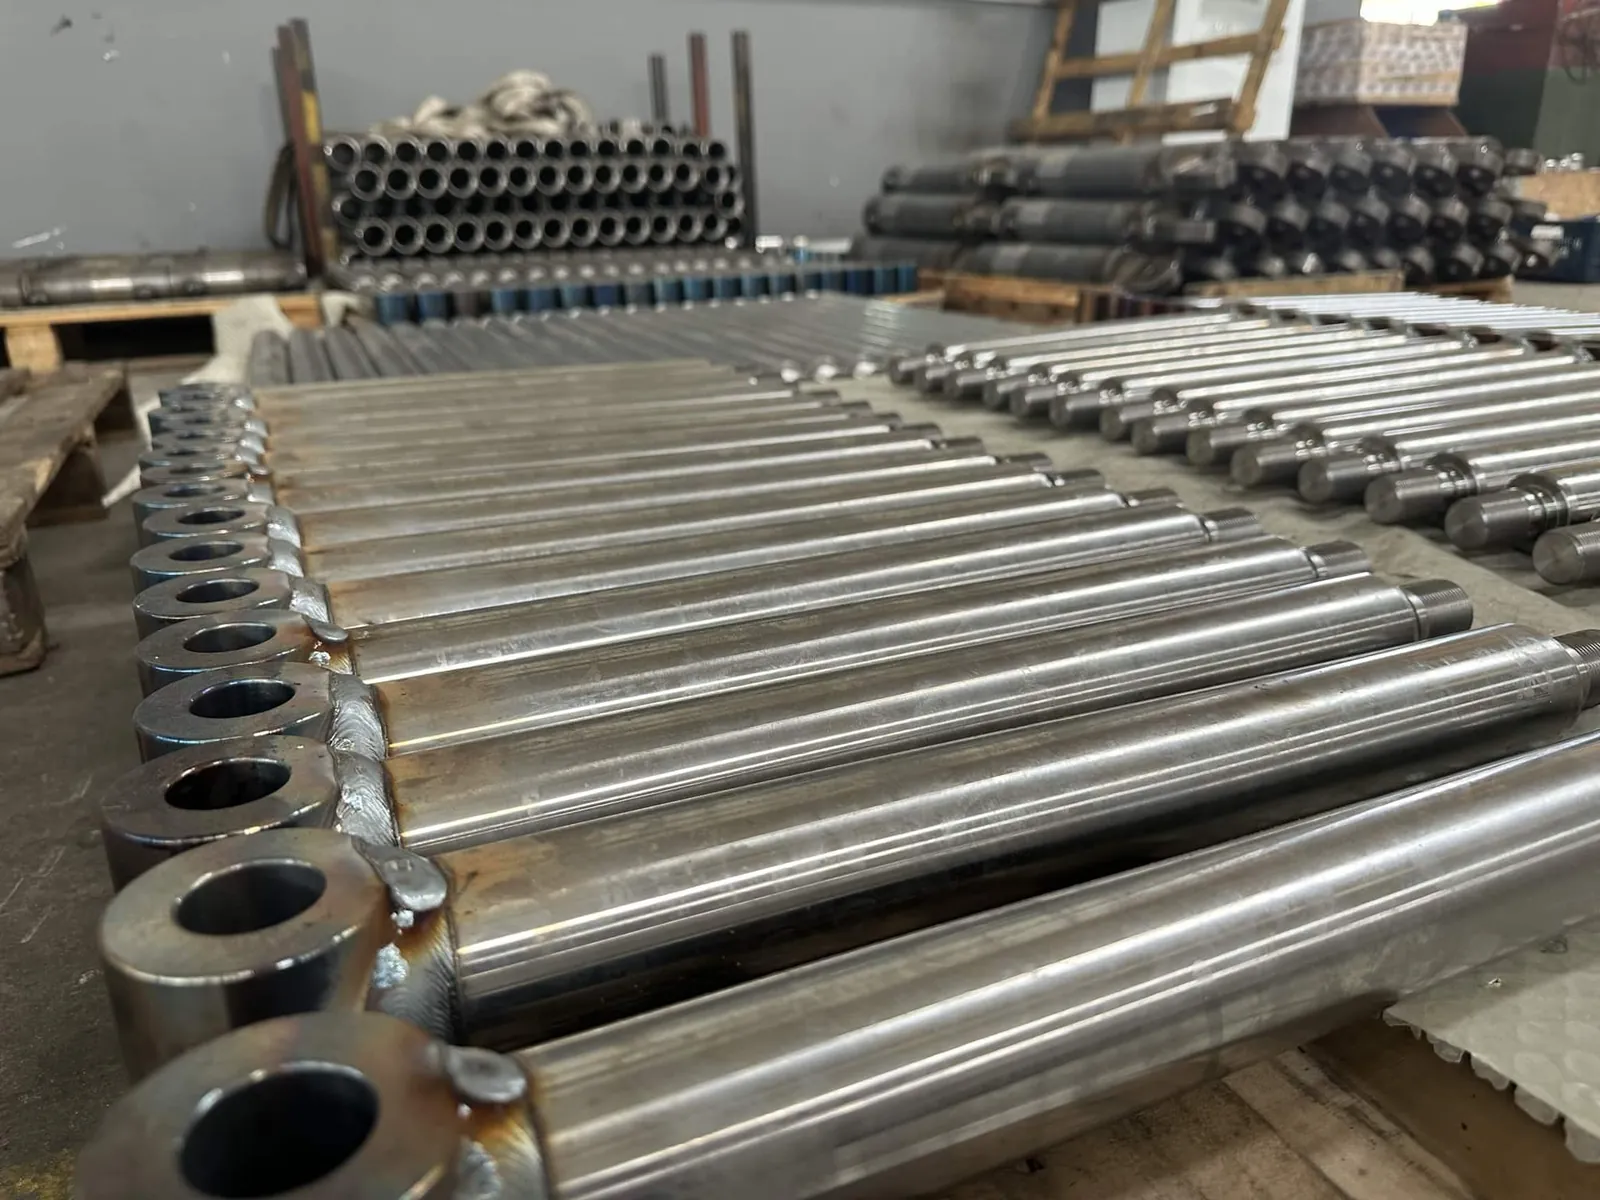
Piston rods
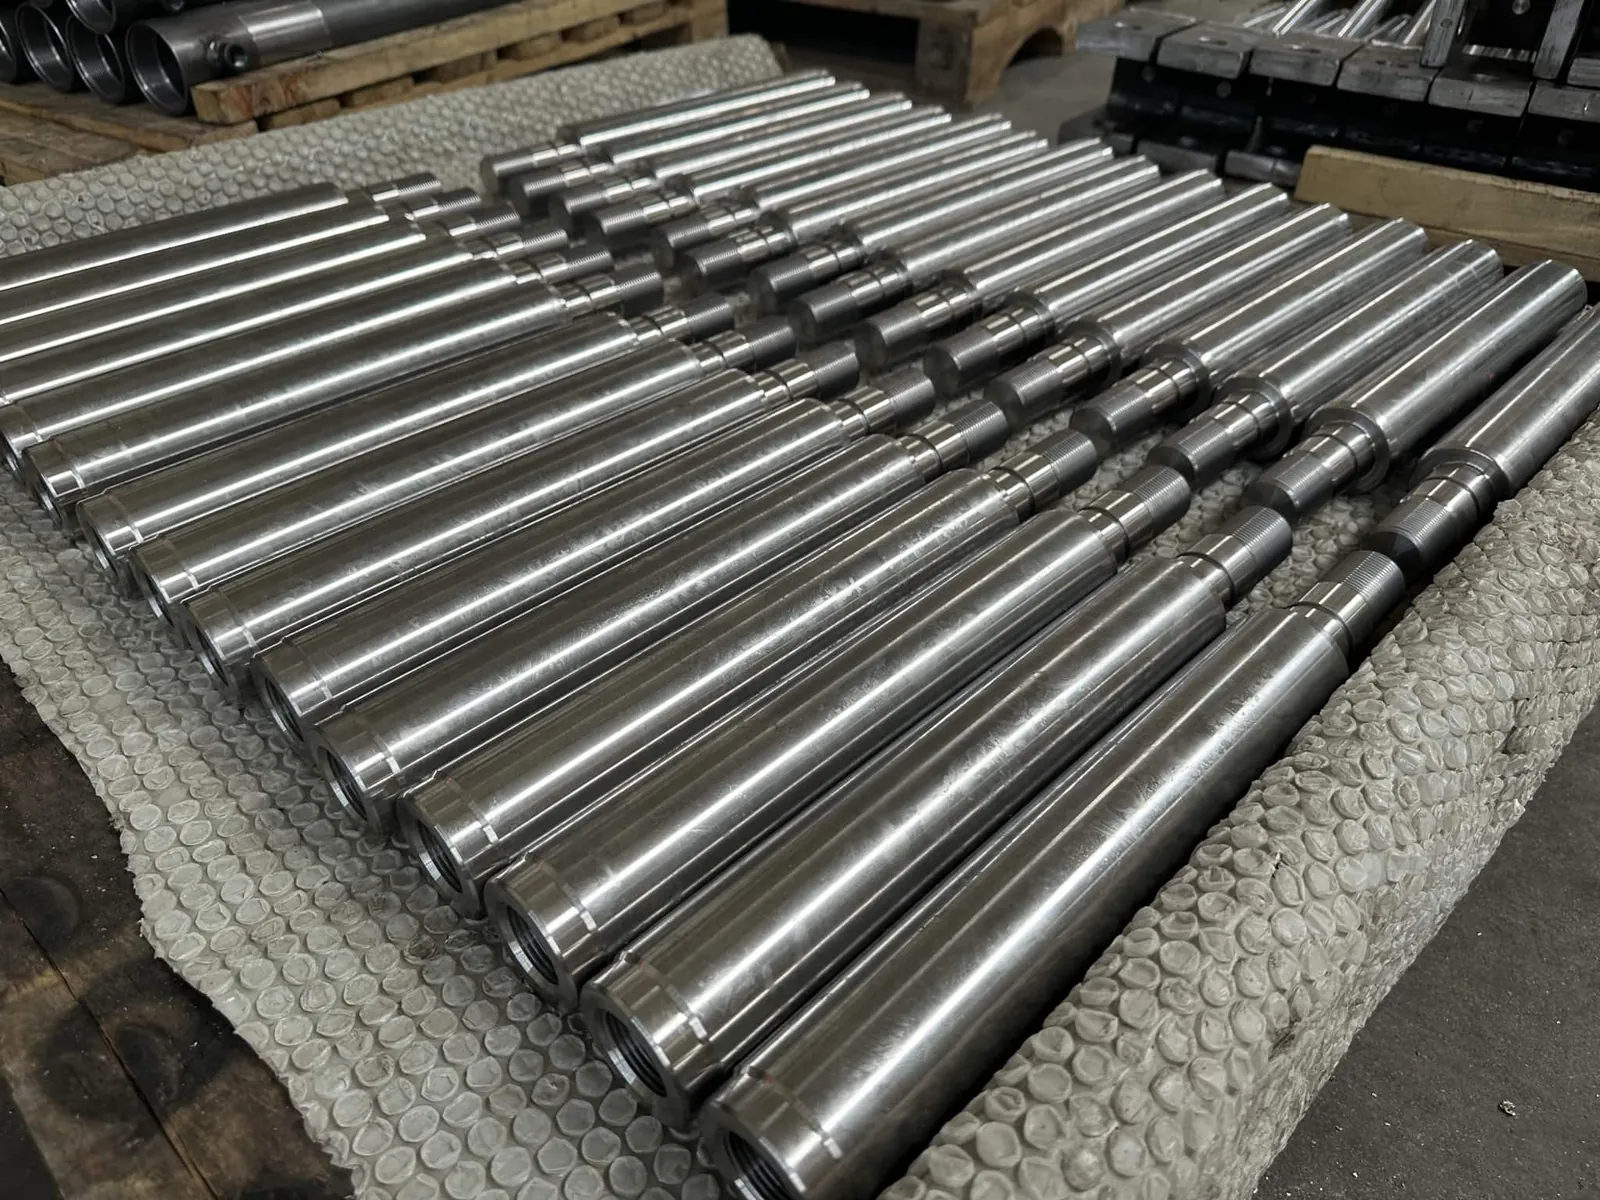
Turned, ground and hard-chrome plated rods, with rod eyes or threads.
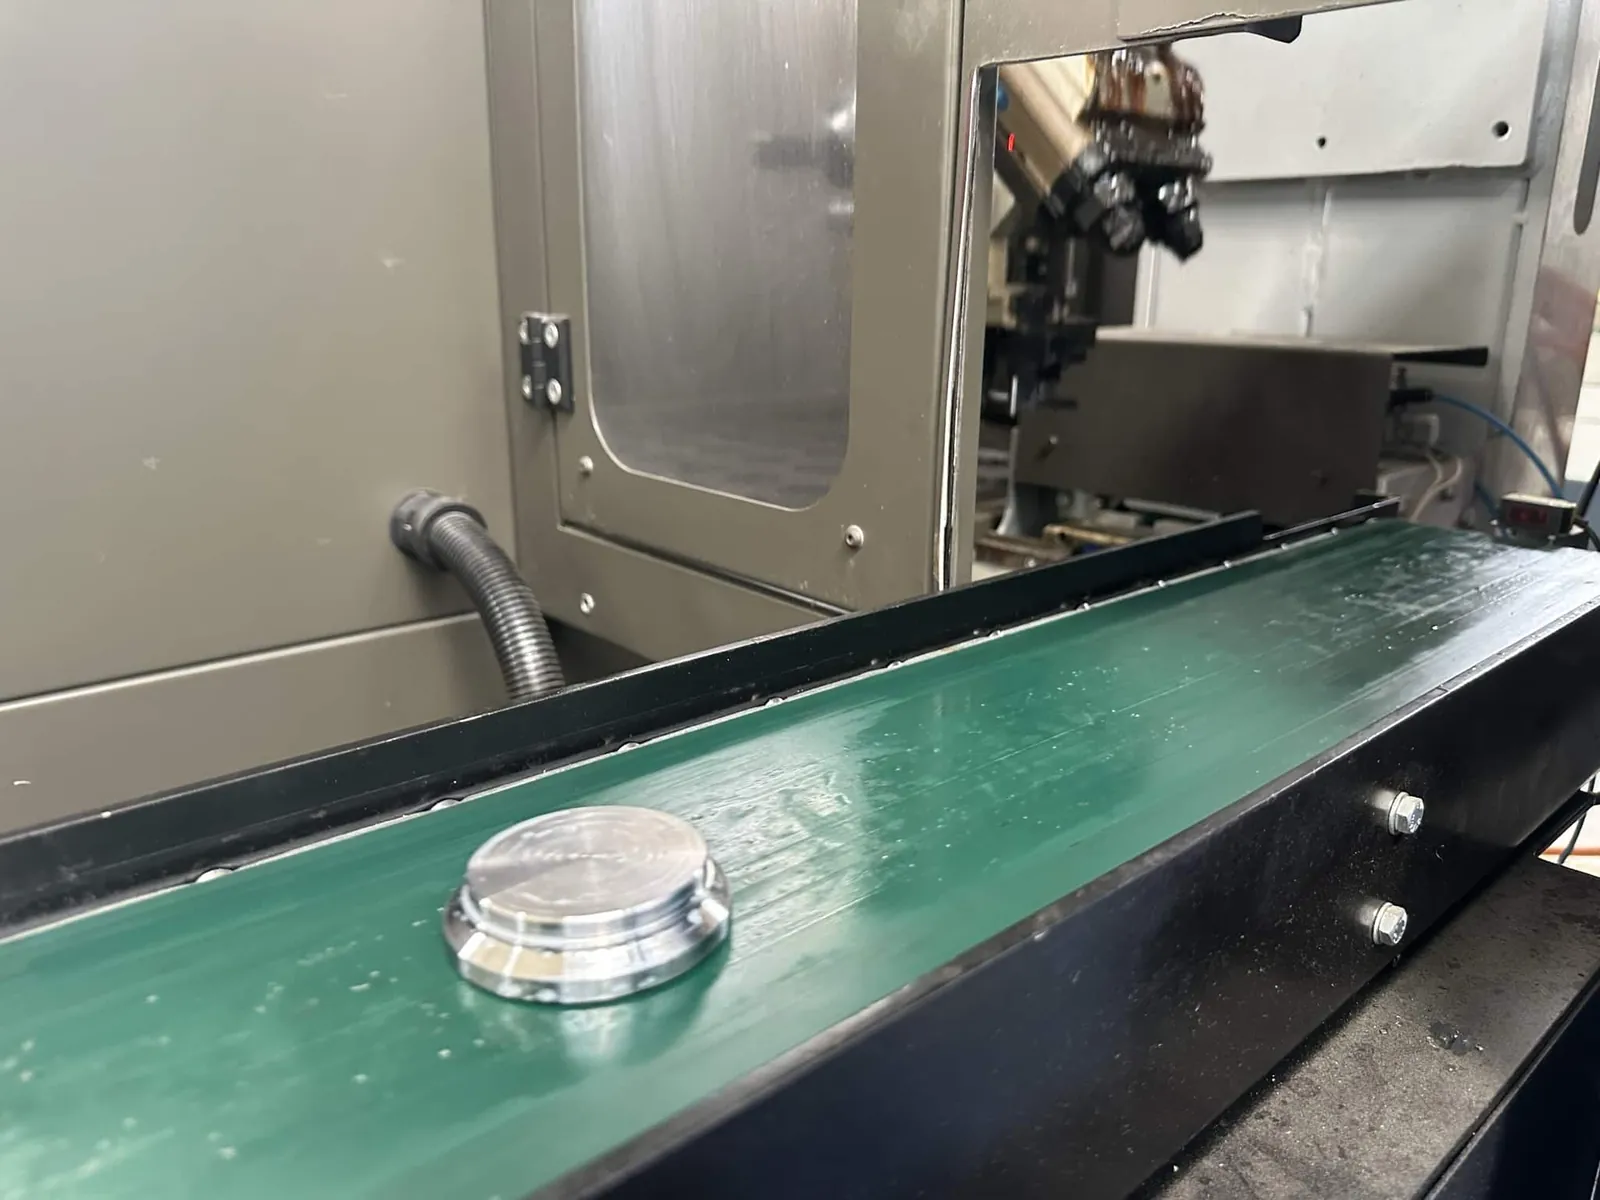
Pistons
Machined pistons with seal grooves to your drawing.
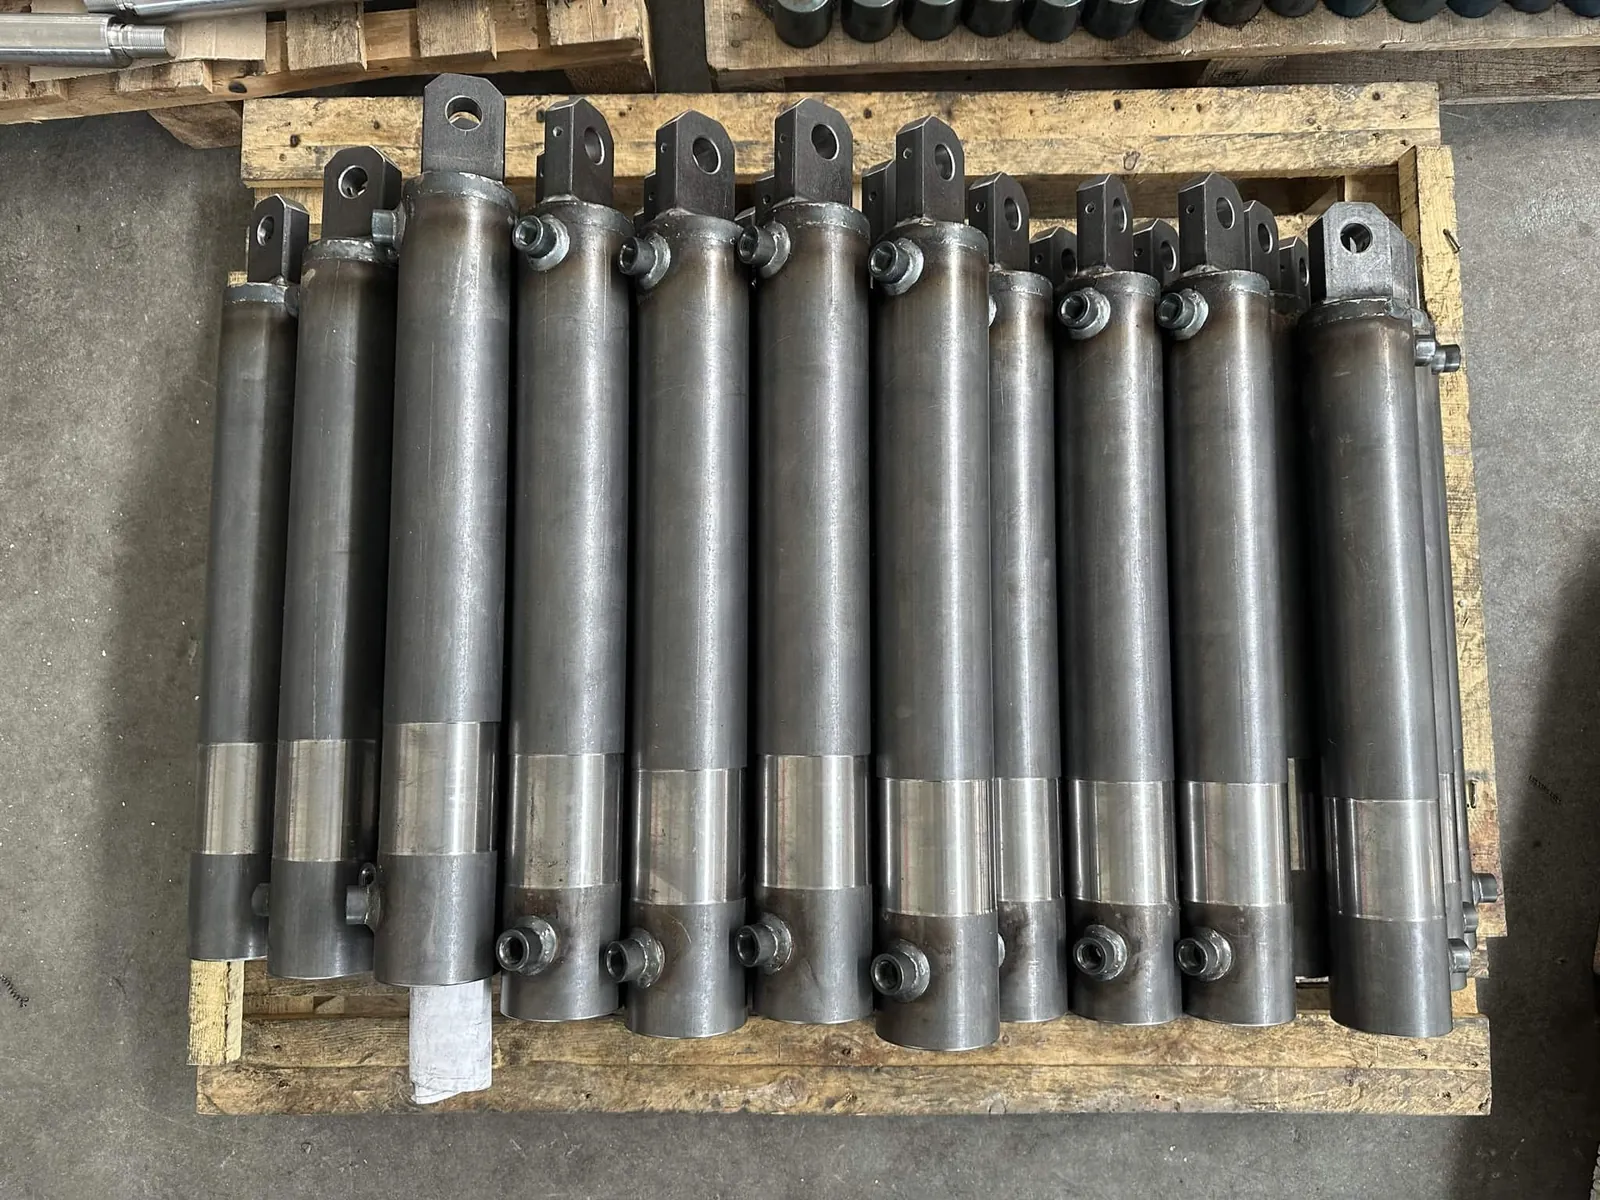
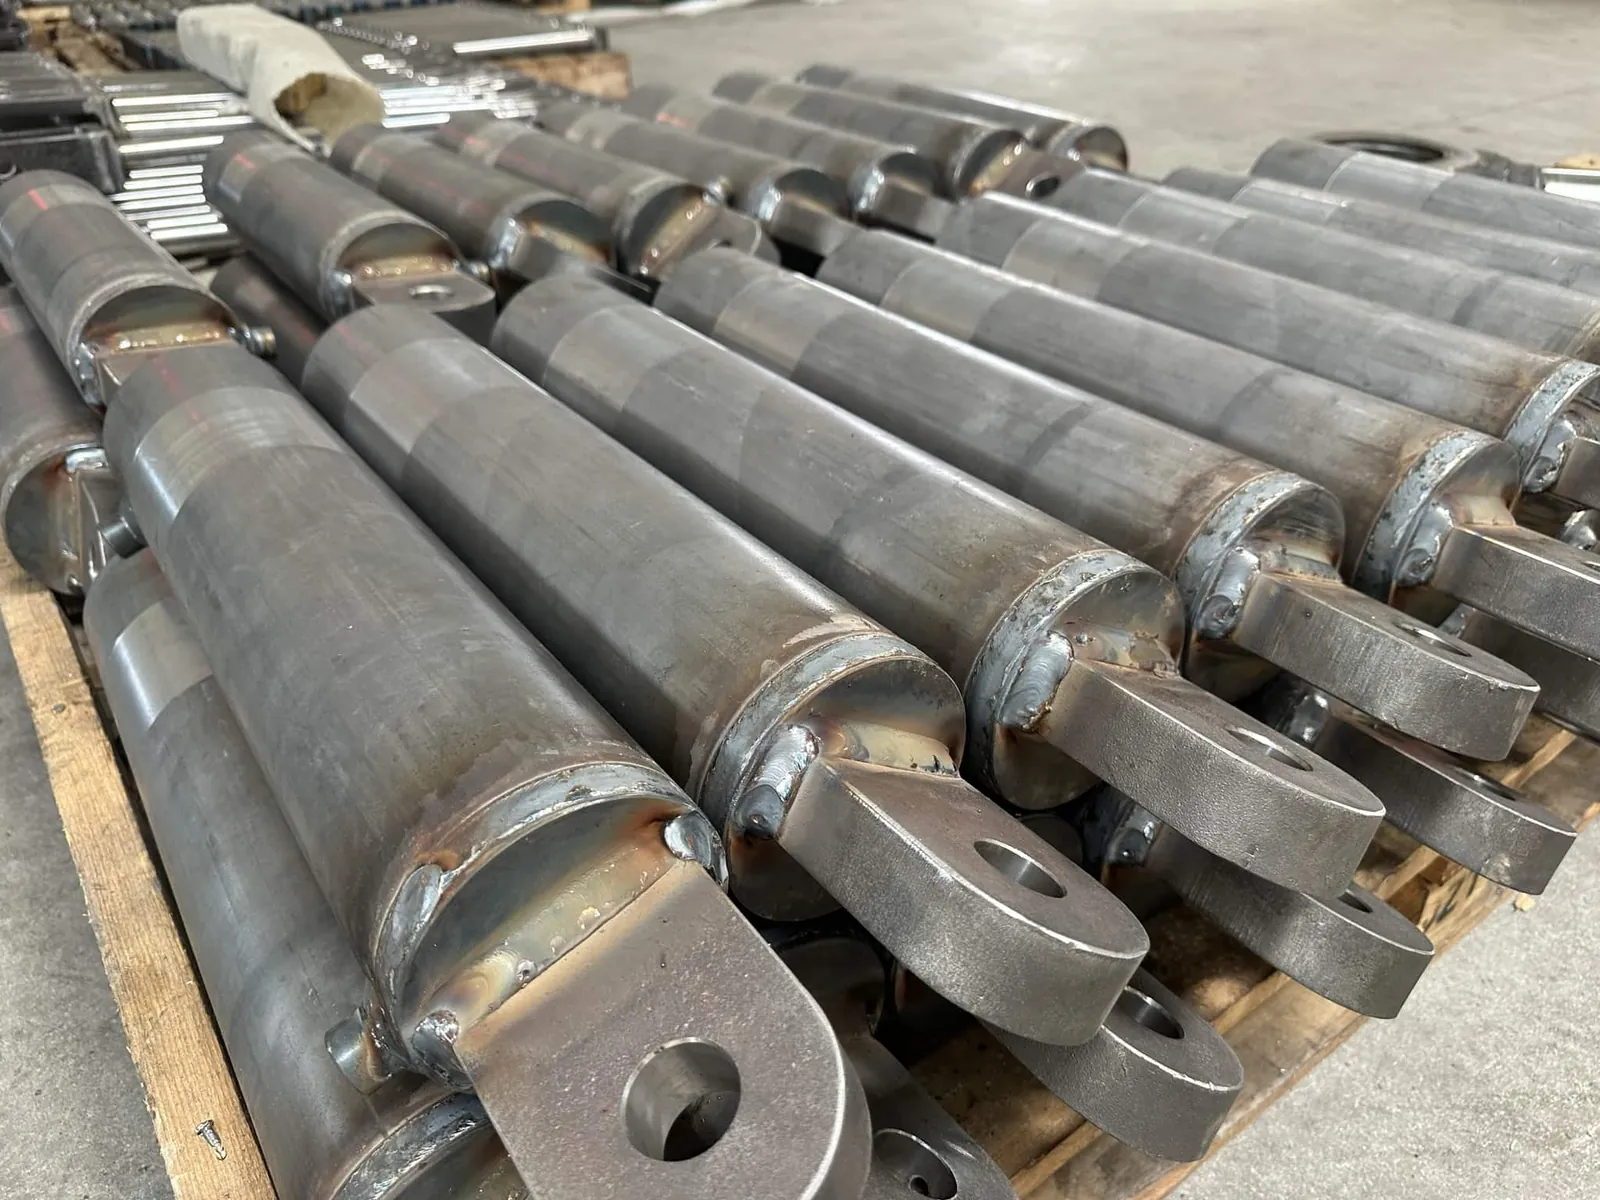
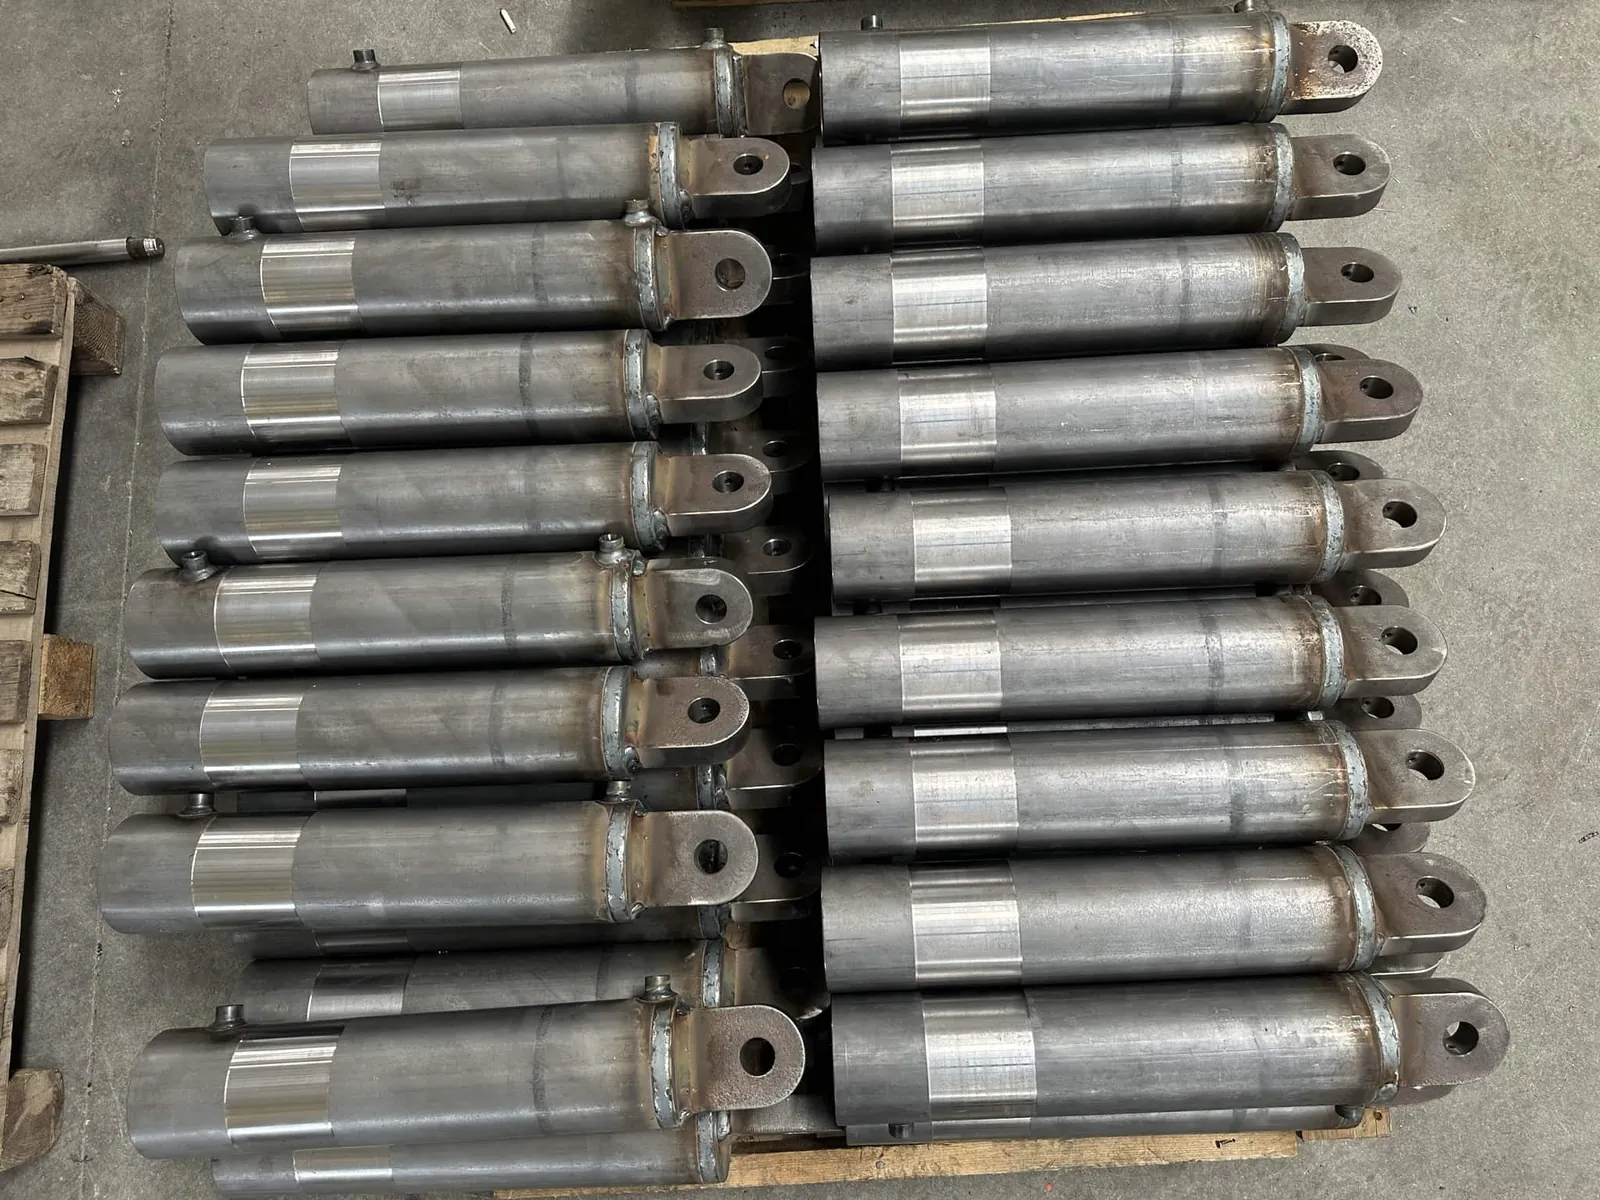
Cylinder barrels
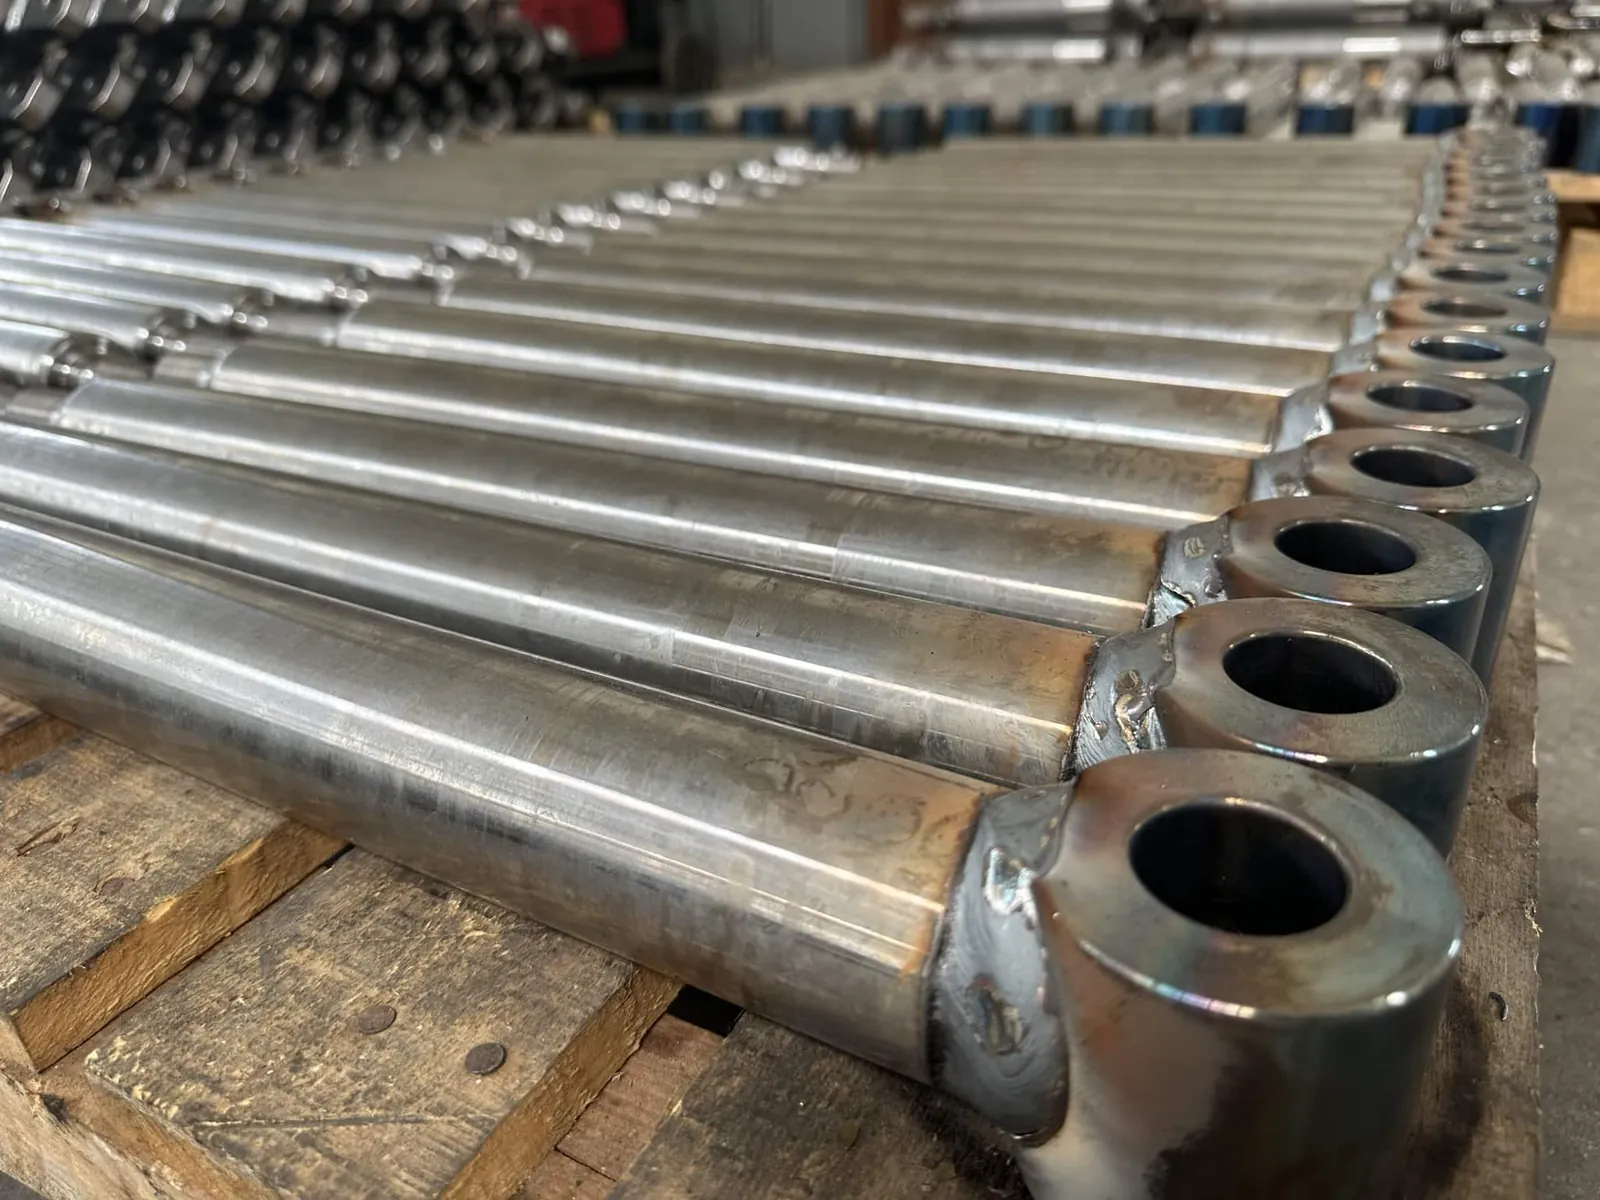
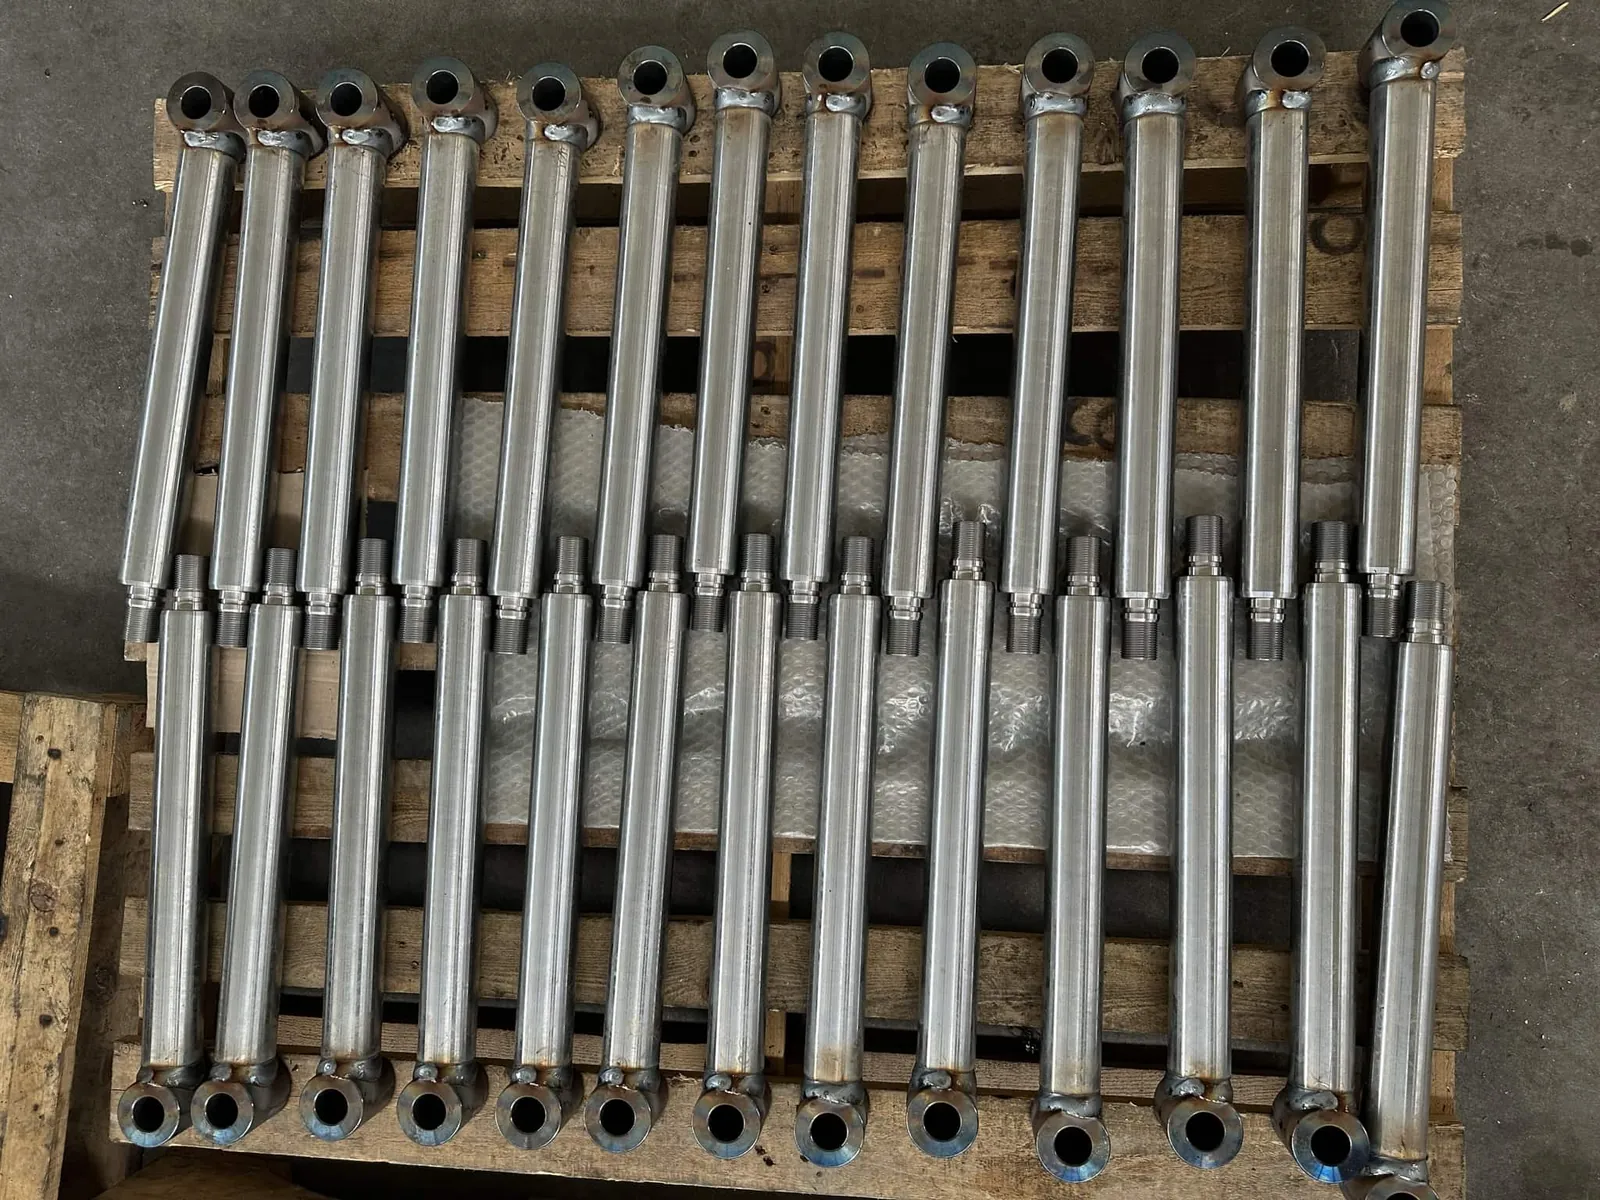
Honed barrels and tubes, with welded clevis eyes, ports and flanges.
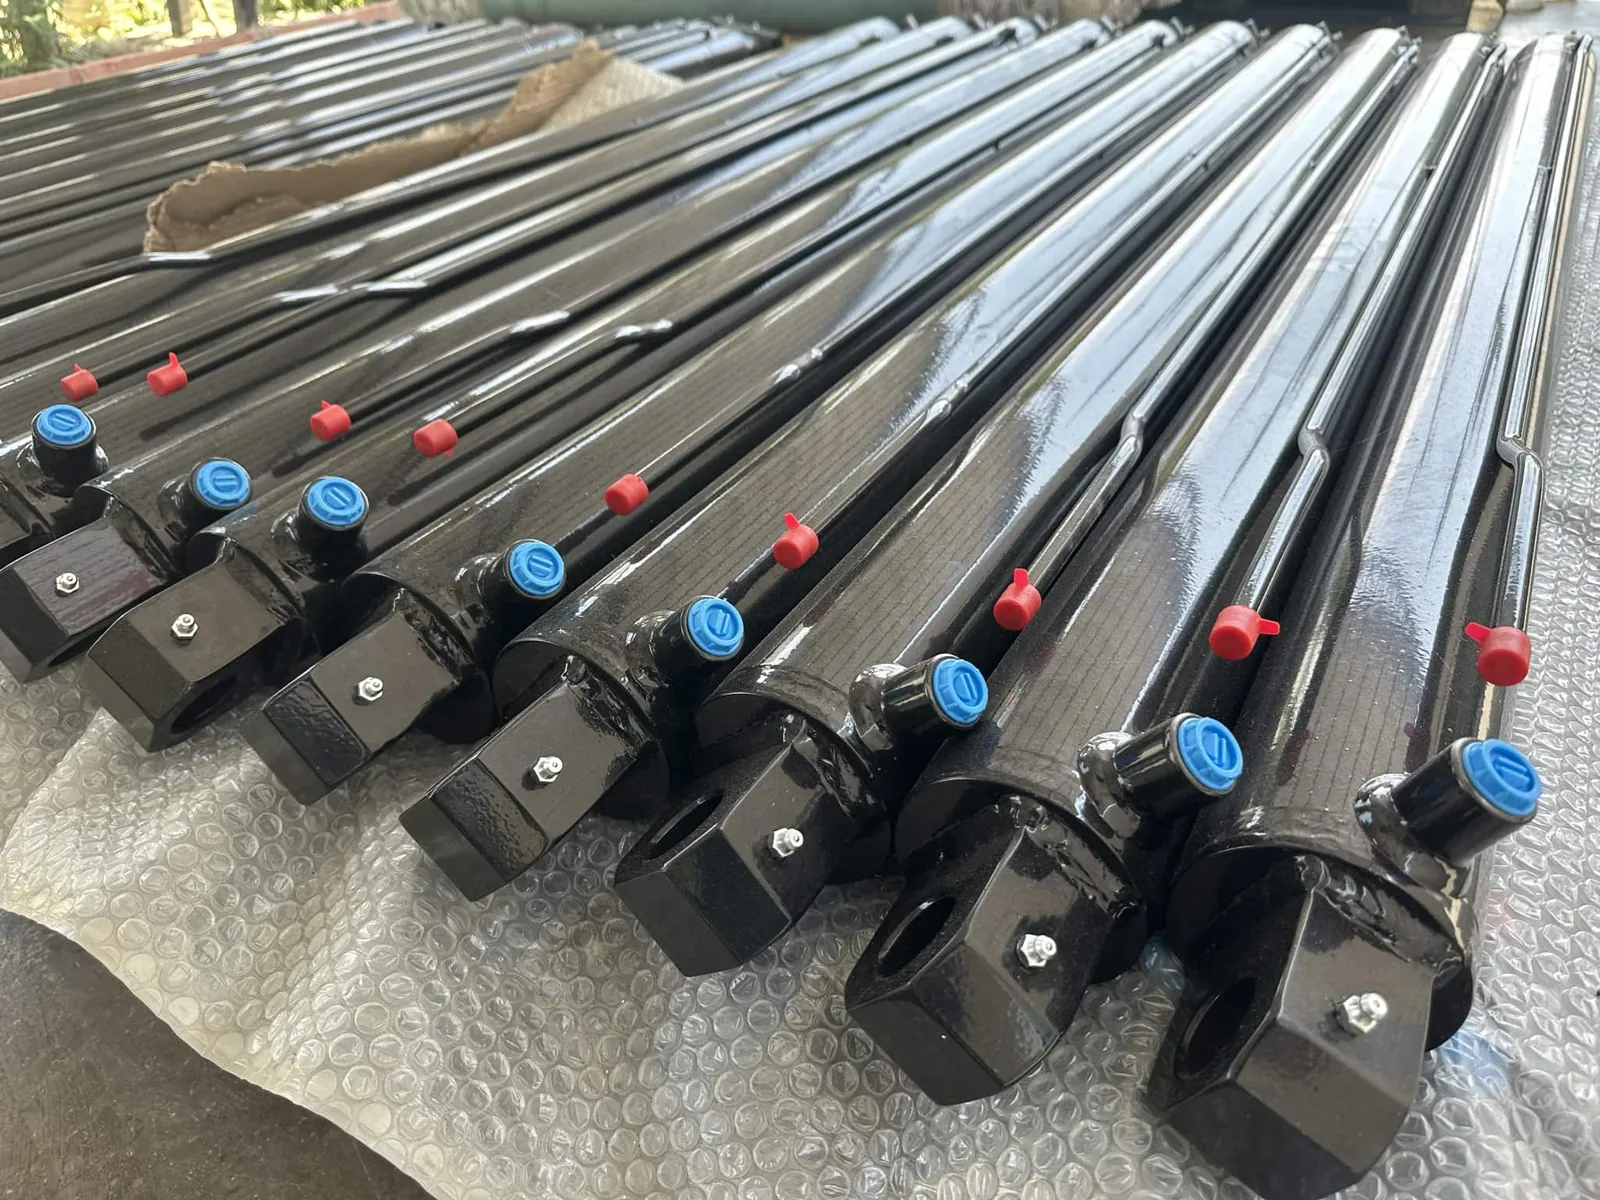
Complete cylinders
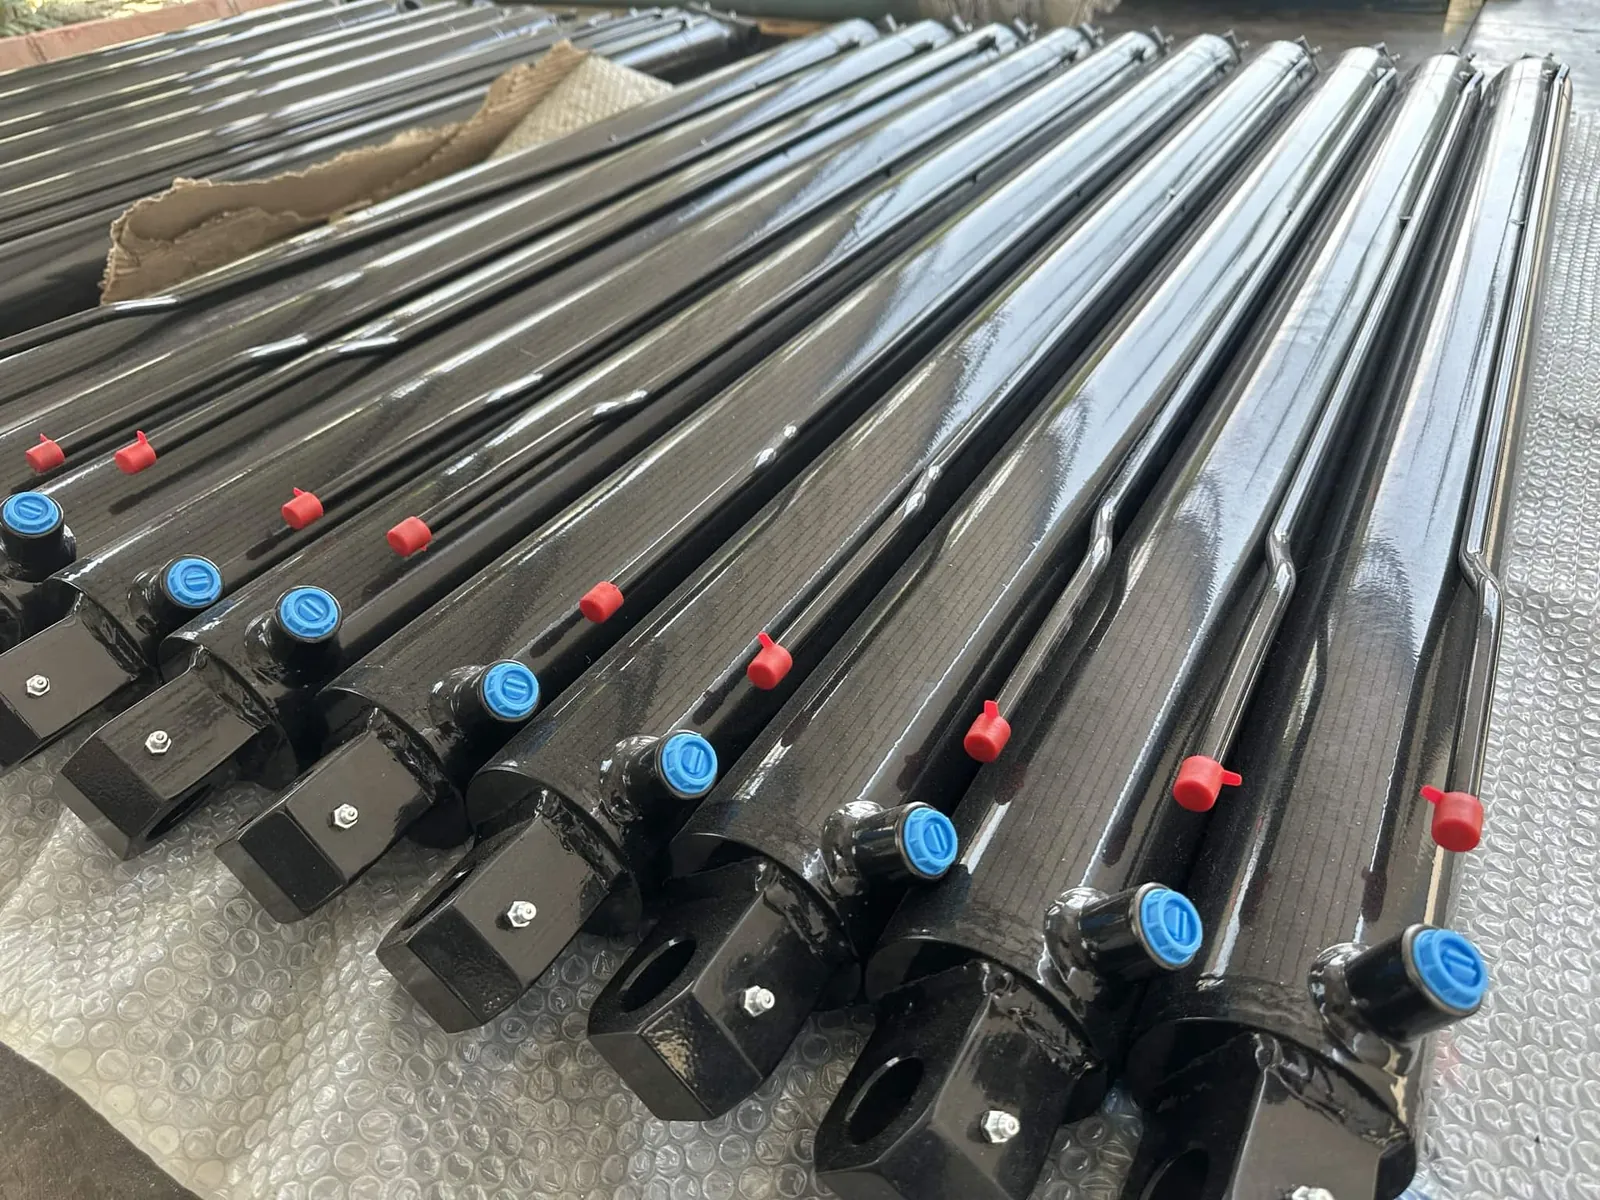
Assembled, painted cylinders with port caps, ready for shipping.
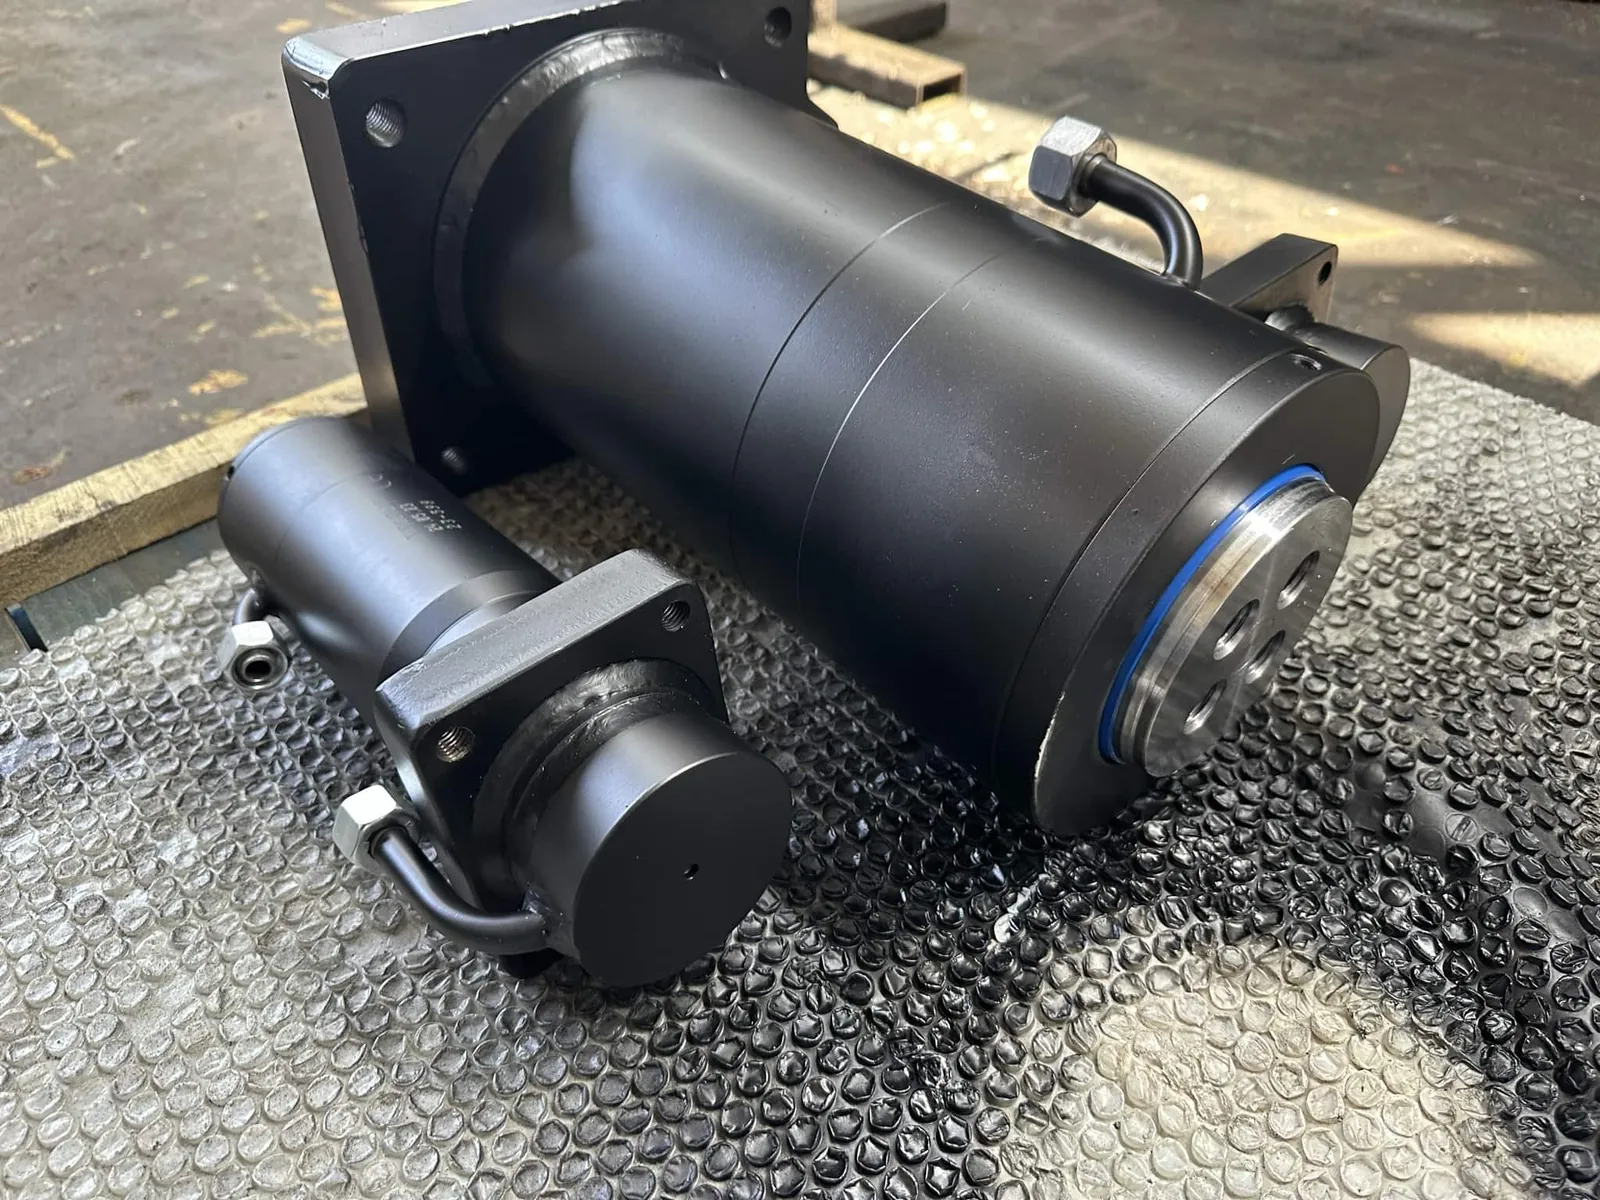
Flange-mounted cylinders
Heavy cylinders with square or round mounting flanges.
Plungers
Large chrome-plated plungers for presses and lifting equipment.
Honed Barrels up to Ø550 mm and 6,000 mm Deep
The seal of a hydraulic cylinder runs on the bore, so bore quality decides how long the cylinder stays tight. Our honing machines finish bores from Ø200 mm up to Ø550 mm and depths up to 6,000 mm, with the cross-hatch surface seals need.
- Six honing machines, up to Ø550 × 6,000 mm
- Welded clevis eyes, ports and flanges under certified procedures
- Piston rods hard-chrome plated and ground in-house
- Assembly and painting to your specification
Hydraulic Component Capacity
We work to frozen drawings for repeat call-off orders. Send the drawing, material, quantity per batch and annual volume.
| Bore honing | Ø200 to Ø550 mm, up to 6,000 mm deep |
|---|---|
| Piston rods | Turned, ground, hard-chrome plated |
| Hard chrome | Rods and plungers, ground after plating |
| Welding | Clevis eyes, ports, flanges; EN 1090 EXC3, ISO 3834-2 |
| CNC turning | Series parts on CNC lathes incl. robot-loaded cell |
| Supply | Components or complete painted cylinders |
| Quantities | Repeat batches and call-off orders |
Questions About Hydraulic Cylinder Parts
Do you make complete hydraulic cylinders?
Yes. We make piston rods, pistons and barrels, and supply them as components or as complete, painted cylinders to your drawing.
What bore sizes can you hone?
From Ø200 mm up to Ø550 mm, and up to 6,000 mm deep.
Do you hard chrome plate piston rods?
Yes. Piston rods are turned, ground, hard-chrome plated and finish-ground in-house.
Can you supply repeat batches?
Yes. We produce to frozen drawings for repeat and call-off orders.
Hydraulic Cylinder Components With Honing and Chrome In-House
A hydraulic cylinder is a set of precision surfaces: a honed bore, a ground and chromed rod, and a piston that seals between them. Many suppliers buy in honed tube and chrome bar and only assemble. We hone barrels, plate and grind rods and machine pistons ourselves, which gives control over the surfaces that decide the cylinder's life.
Batches for machine builders
Hydraulic components are typically ordered by builders of agricultural, construction, lifting and industrial machinery, as repeat batches on frozen drawings. CNC turning centres, including a robot-loaded cell, keep series parts consistent; see the machine park.
Related capability
The same hard chrome and grinding lines serve our roller business, and welded parts are produced under the certified procedures of Nika Steelworks. Send your cylinder drawing via the contact page.
Piston rods: the critical surface
A piston rod moves in and out of the cylinder thousands of times, through a seal that must stay tight. Any scratch, pit or corrosion on the rod damages the seal and causes leaks. Rods are therefore turned, ground, hard-chrome plated and ground again to a fine finish. For outdoor and marine machines, a thicker chrome layer improves corrosion resistance.
Barrels and honing
The barrel bore is the second sealing surface. Honing produces the precise diameter, roundness and cross-hatch pattern the piston seals need to run and hold oil. Our six honing machines cover bores from Ø200 mm to Ø550 mm and up to 6,000 mm deep, which includes long-stroke cylinders for cranes, presses and heavy machinery.
Welded mounting parts
Clevis eyes, trunnions, ports and flanges are welded to barrels and rods under certified procedures, then machined where the drawing requires it, so mounting bores line up with the cylinder axis. Finished cylinders are painted and fitted with port caps for transport.
Call-off orders for machine builders
Machine builders often order hydraulic components on annual frameworks with monthly or quarterly call-offs. We hold the approved drawing and process, so every call-off matches the previous one, and plan production around your schedule.