Quality and Testing for Every Roller
Certified welding, dimensional and runout inspection, CMM measurement and EN 10204 3.1 material certificates. Every roller leaves with the documents that prove it matches your drawing.
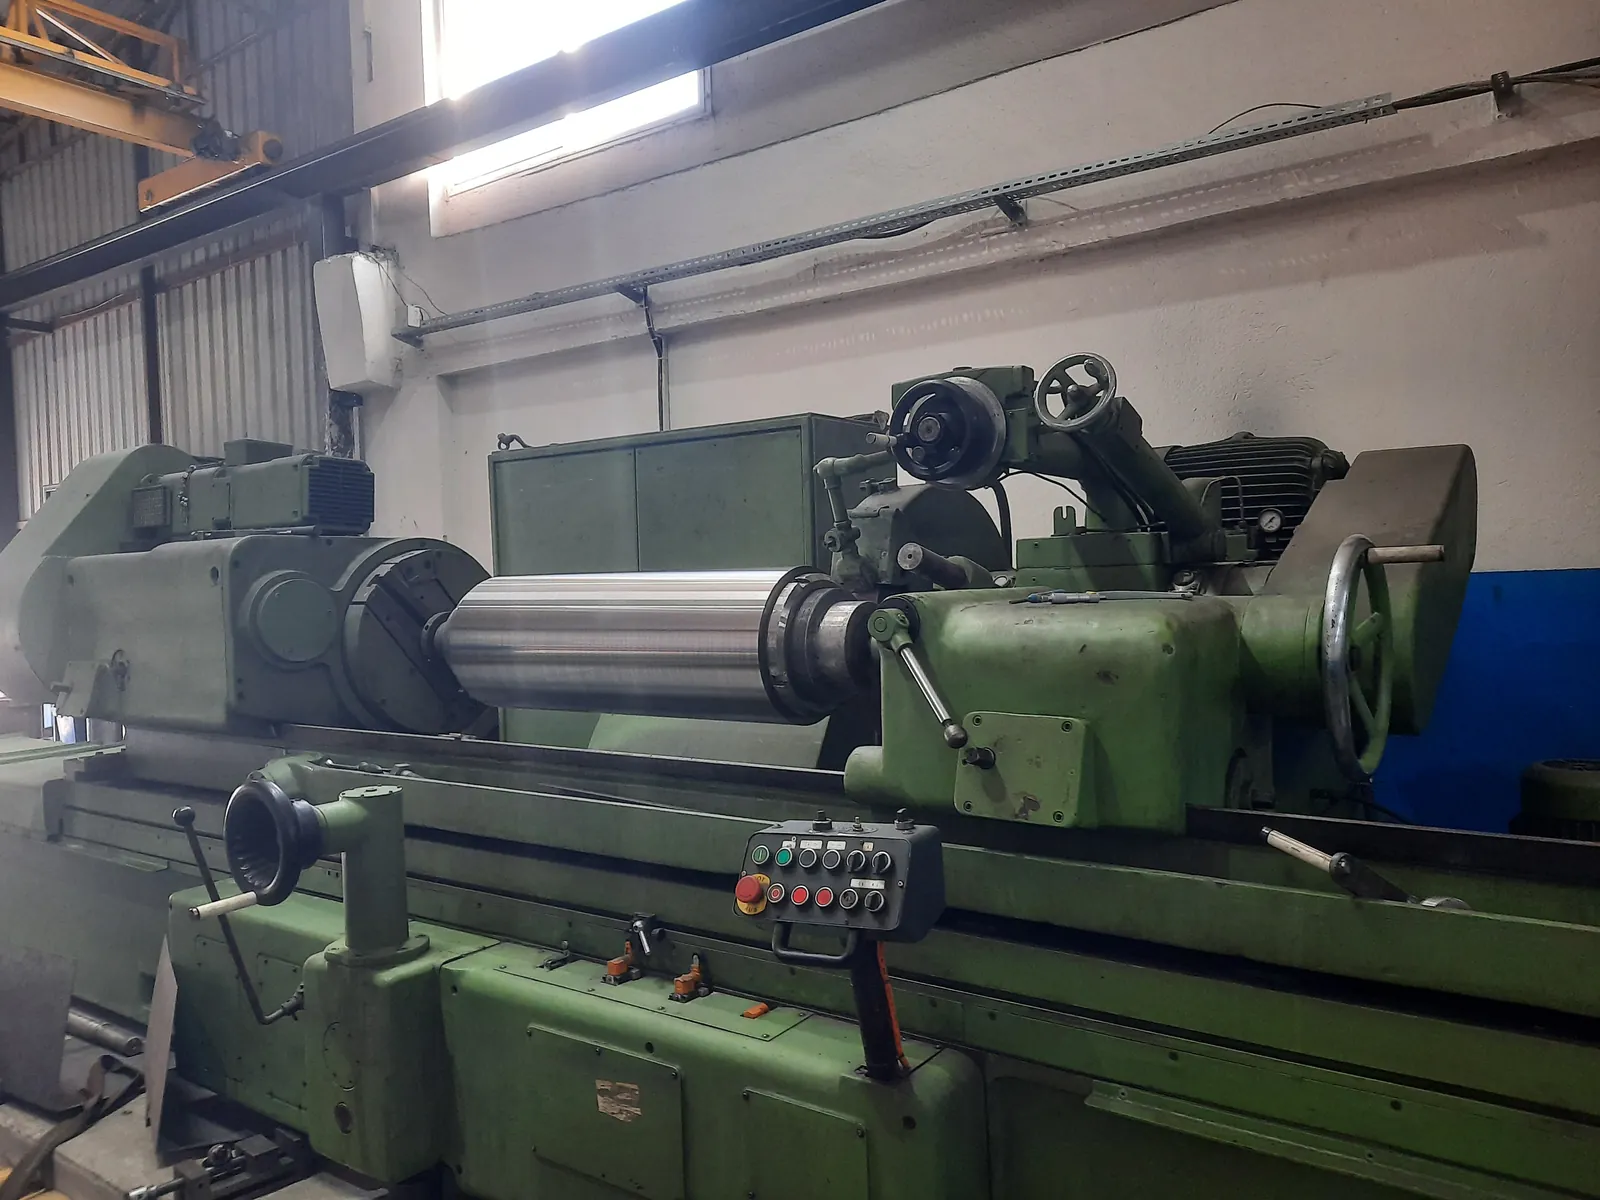
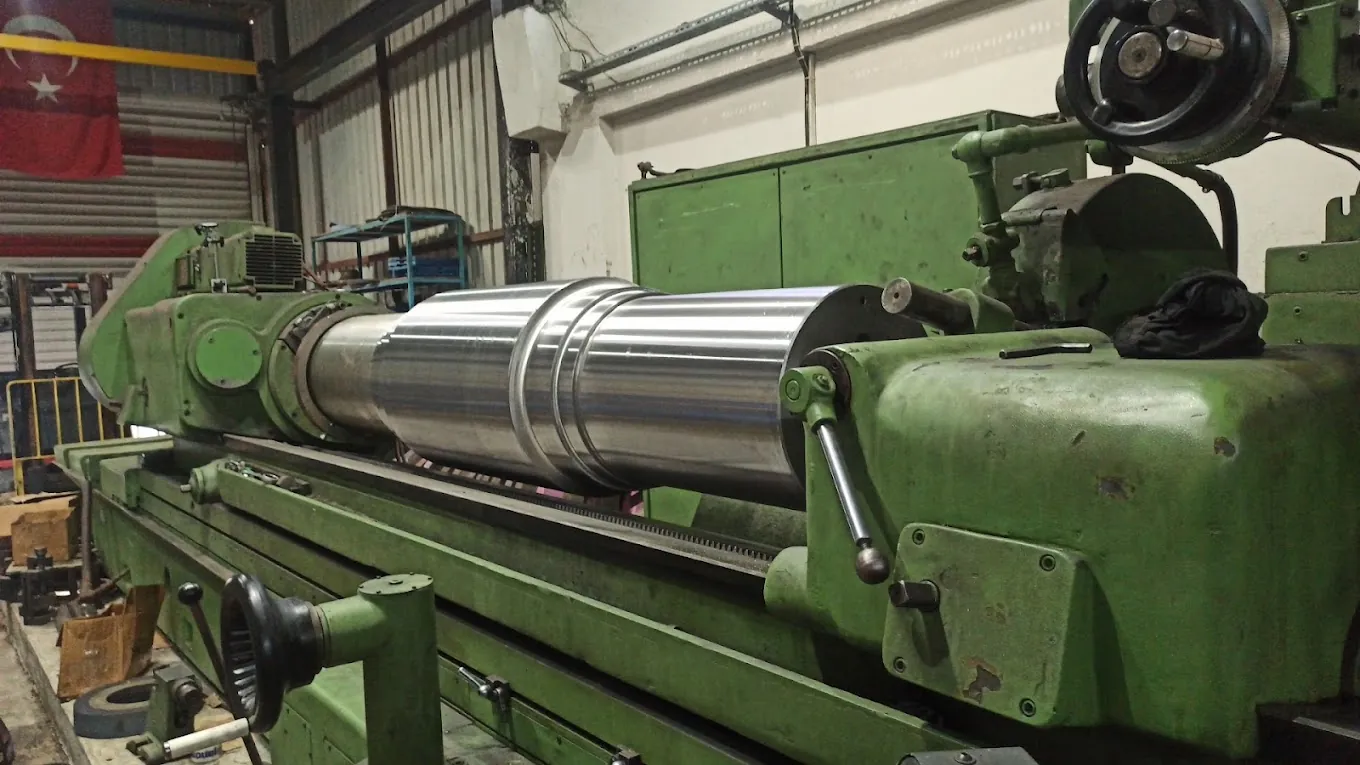
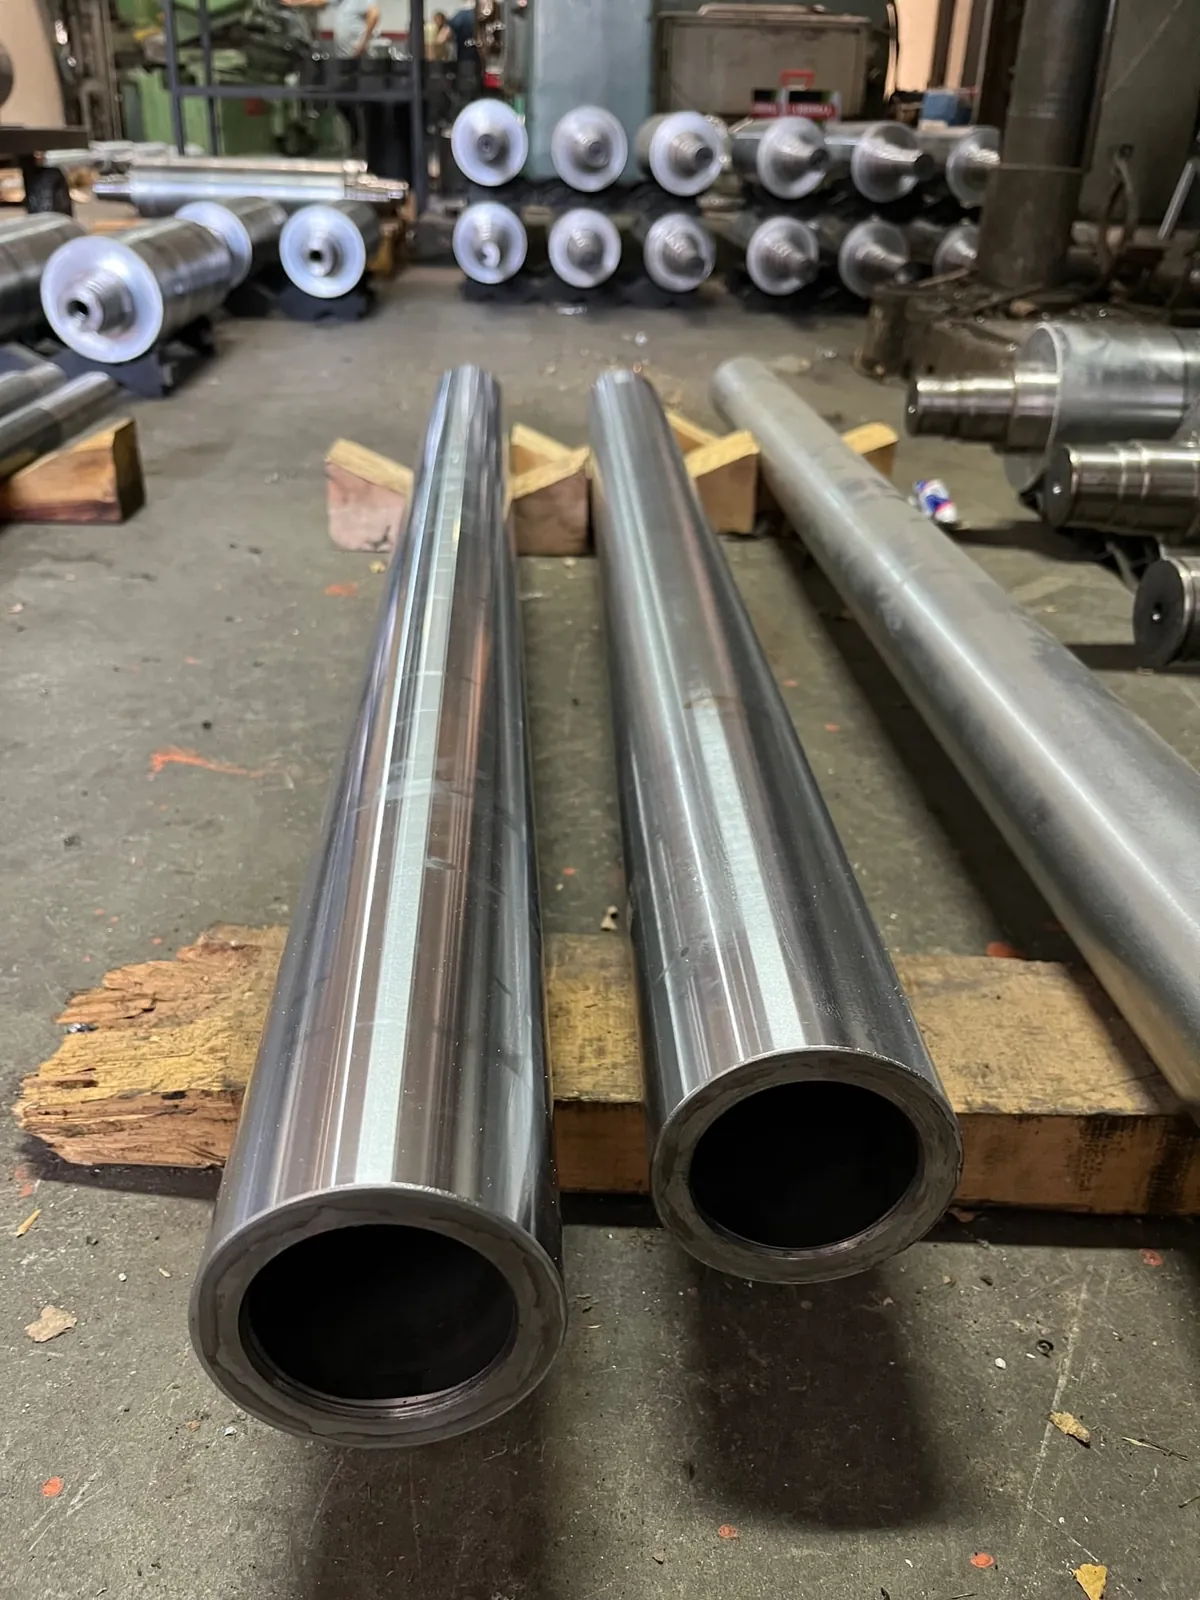
Quality Starts at the Machine
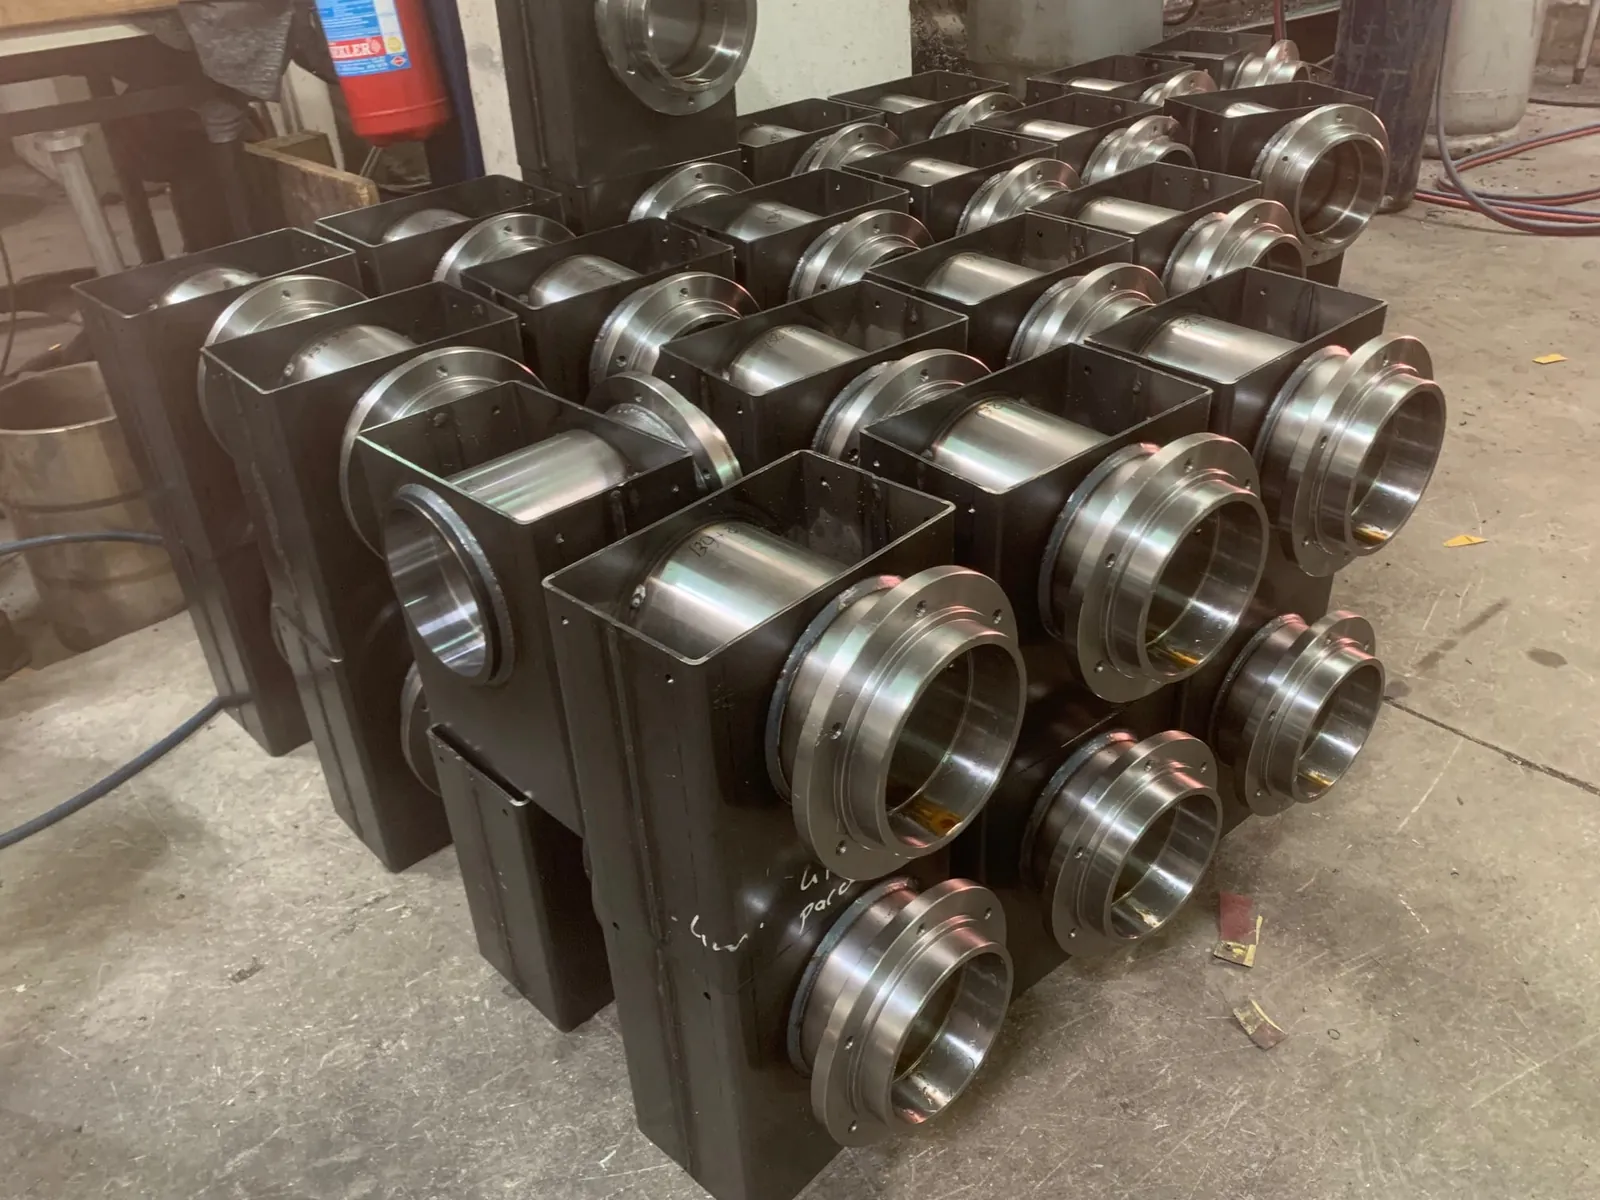
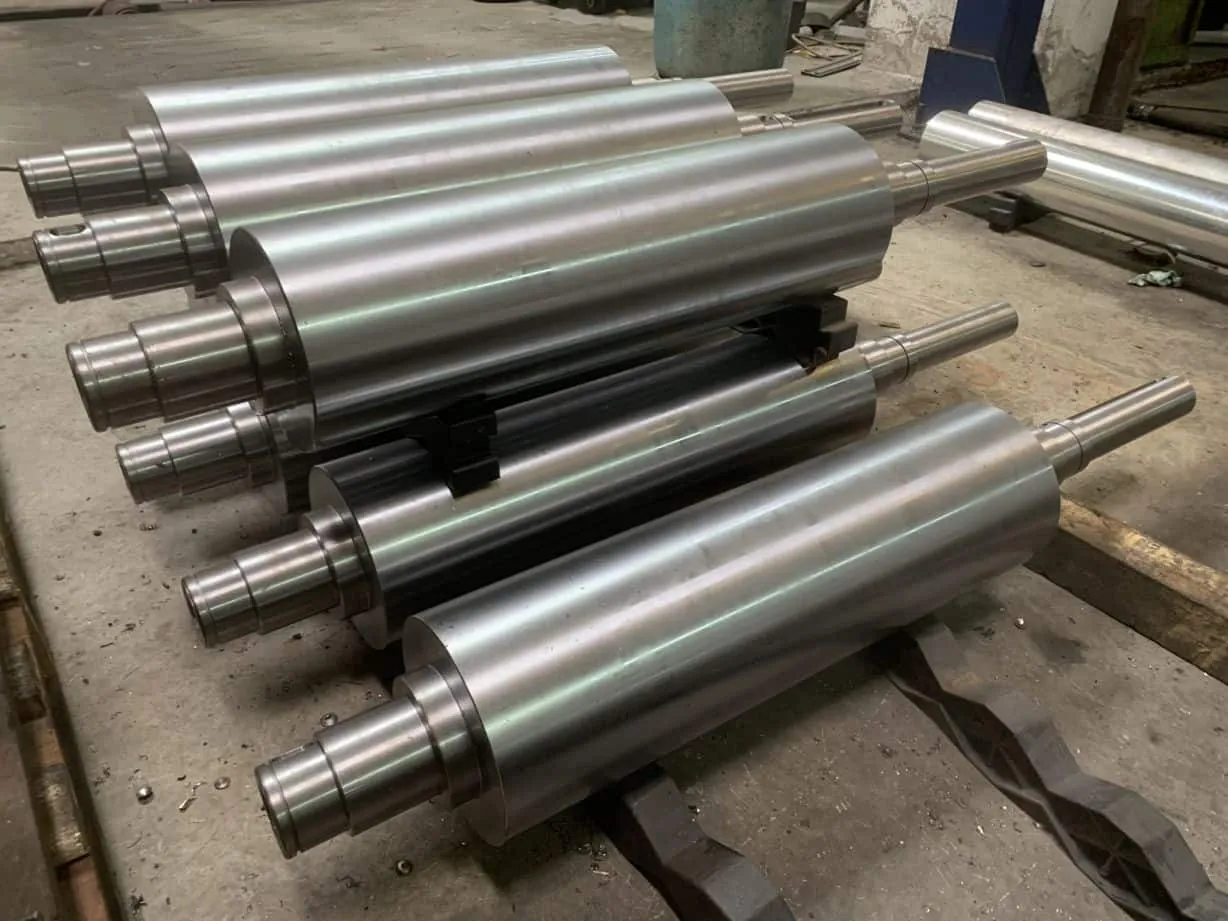
Our Certificates
ISO 9001:2015
Quality management system covering quoting, production, inspection and delivery.
EN 1090-1 FPC
Factory production control for welded steel components.
EN 1090-2 EXC3
Execution class 3 for welded steel, the class used for demanding structural work.
ISO 3834-2
Comprehensive quality requirements for fusion welding, with EN ISO 9606-1 qualified welders.
What We Check Before a Roller Ships
Every roller is inspected against its drawing before it is packed. The checks depend on the roller type and your specification, and typically include:
- Diameters, lengths and journal dimensions
- Runout of body and journals, to 0.01 mm on ground rolls
- Surface finish (Ra) on ground and chromed surfaces
- Coating thickness and hardness where specified
- CMM measurement for tight-tolerance features
- Balance after balancing
- Visual and NDT inspection of welds when specified
Documents Supplied With Your Roller
Tell us which documents your quality department needs. Standard documents come with every order; others are supplied on request.
| Material certificates | EN 10204 3.1 with every order; 3.2 on request |
|---|---|
| Dimensional report | Key dimensions against drawing |
| Runout report | Body and journal runout |
| Surface report | Roughness and coating data where specified |
| Welding documents | WPS, welder qualifications on request |
| NDT reports | When specified (e.g. UT, MT, PT) |
| Balancing report | On request |
Quality at Every Step
Drawing review
Requirements, tolerances and documents are confirmed before production.
Material check
Material grades checked against EN 10204 certificates, with heat-number traceability.
Welding control
Certified procedures and qualified welders under EN 1090 and ISO 3834-2.
In-process checks
Dimensions and runout checked between turning, grinding and coating.
Final inspection
Full inspection against the drawing, with CMM and NDT where specified.
Documentation
Reports and certificates packed with the roller and sent digitally.
Questions About Quality
Which certificates do you hold?
ISO 9001:2015, EN 1090-1 factory production control, EN 1090-2 EXC3 and ISO 3834-2, with welders qualified to EN ISO 9606-1.
Do you supply material certificates?
Yes. EN 10204 3.1 certificates with every order, and 3.2 certificates on request.
Do you measure runout?
Yes. Body and journal runout is measured and reported, to 0.01 mm on ground rolls.
Can you provide NDT reports?
Yes. NDT such as ultrasonic, magnetic particle or dye penetrant testing is carried out and reported when specified.
Documented Quality for European Buyers
For European buyers sourcing rollers from Türkiye, documented quality is as important as price. Our quality system is shared with Nika Steelworks and certified to ISO 9001:2015, with welding certified to EN 1090-2 EXC3 and ISO 3834-2.
Precision starts in production: rolls are ground to 0.01 mm runout and Ra 0.2 µm, and dynamically balanced. Inspection confirms it, and the documents prove it. See the machine park for our equipment, or tell us what documentation you need.
Traceability
Every steel grade used in a roller is checked against its material certificate on arrival, and heat numbers are tracked through production on request. For welded rollers, welding procedure specifications and welder qualifications are available for your quality documentation.
Inspection between steps
On rollers that go through several processes, such as welding, turning, grinding, plating and balancing, checks happen between steps, not only at the end. That catches a problem while it can still be corrected, instead of after the roller has been plated or lagged.
Third-party inspection
If your project requires third-party inspection or witness tests, tell us at the quoting stage. We plan hold points in production and coordinate with your inspector so inspections do not delay delivery.
Questions we ask before production
Before production starts, we confirm the inspection and documentation requirements with you: which dimensions are critical, which runout and surface values apply, which NDT methods are required and which certificates must accompany the delivery. Agreeing this at the start avoids surprises at delivery.