Machine Park for Large Rollers and Precision Rolls
Turning, grinding, hard chrome plating and balancing up to Ø3,200 mm × 6,000 mm, plus bore honing up to Ø550 × 6,000 mm. Everything a roll needs between the steel blank and the finished, ready-to-install part.
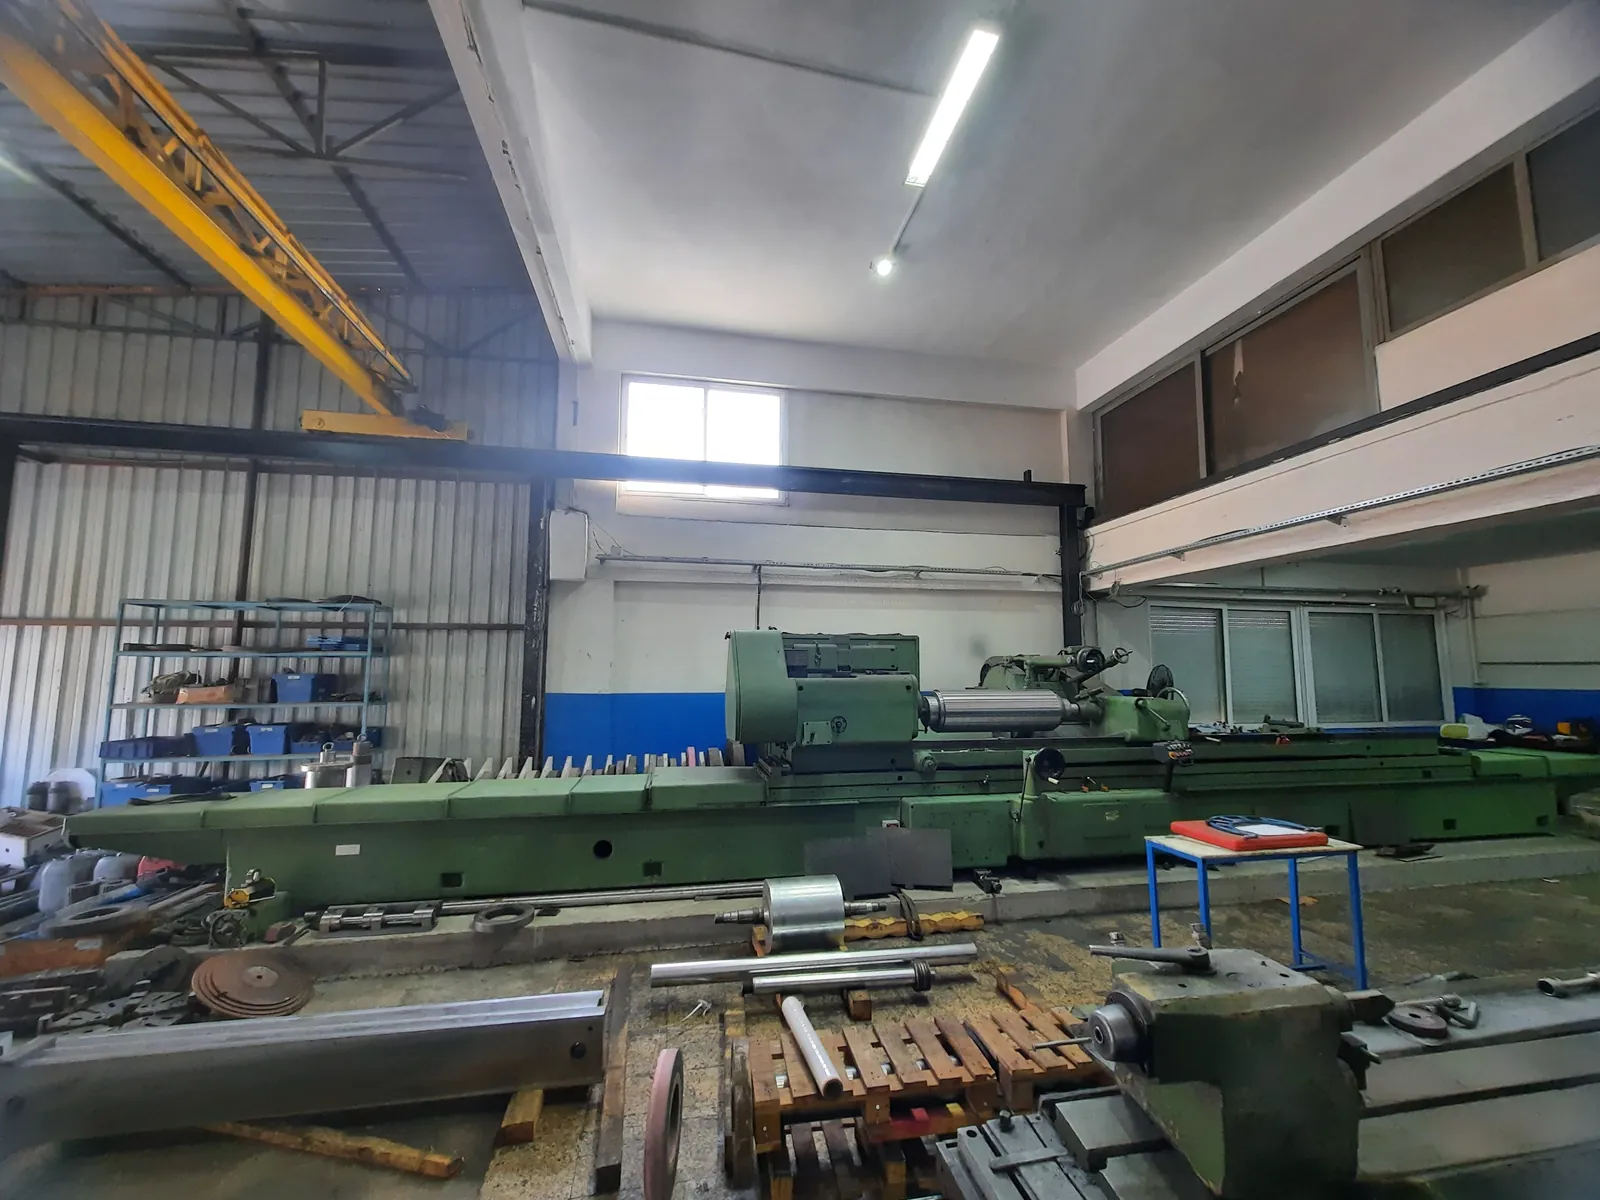
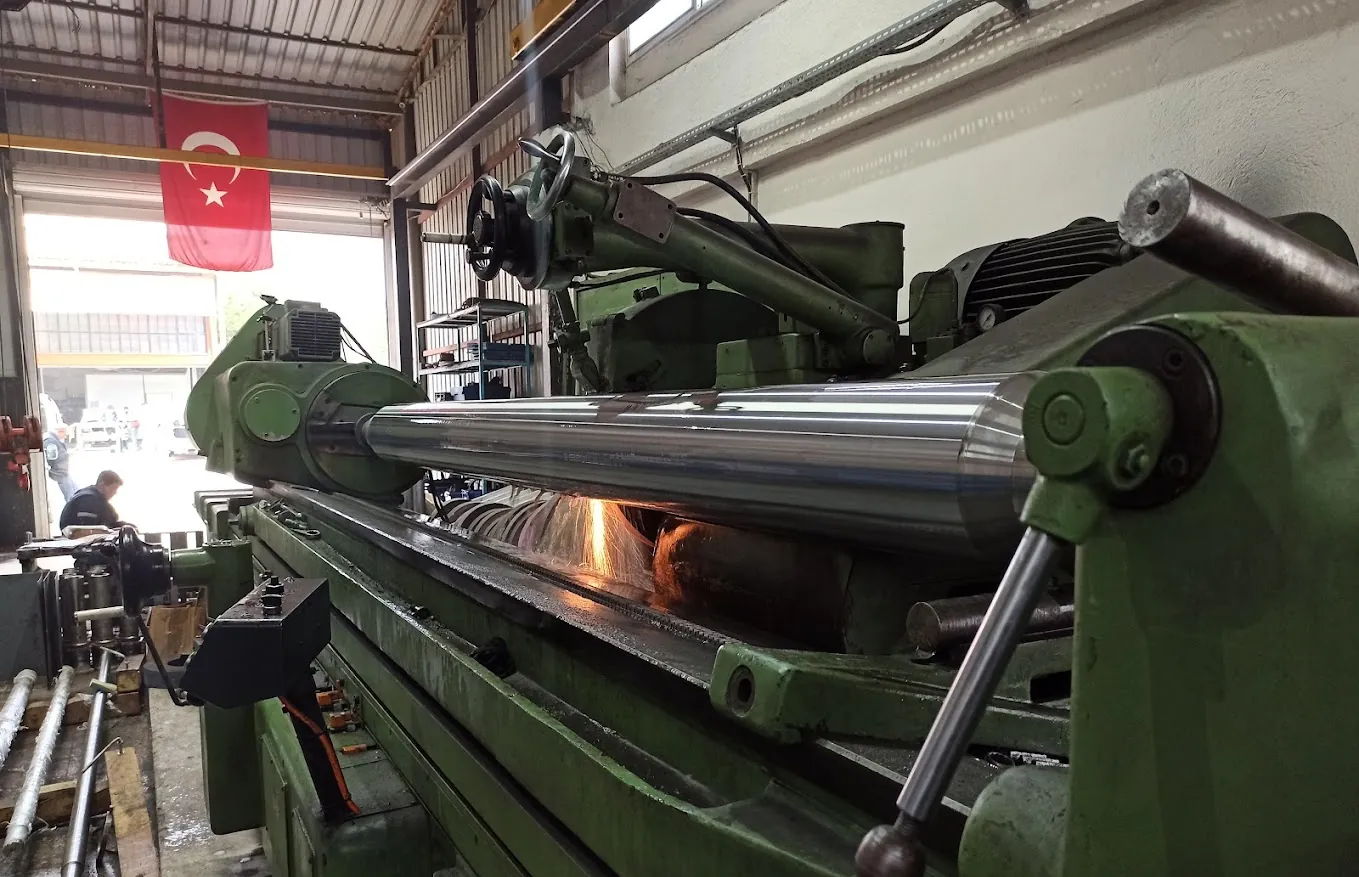
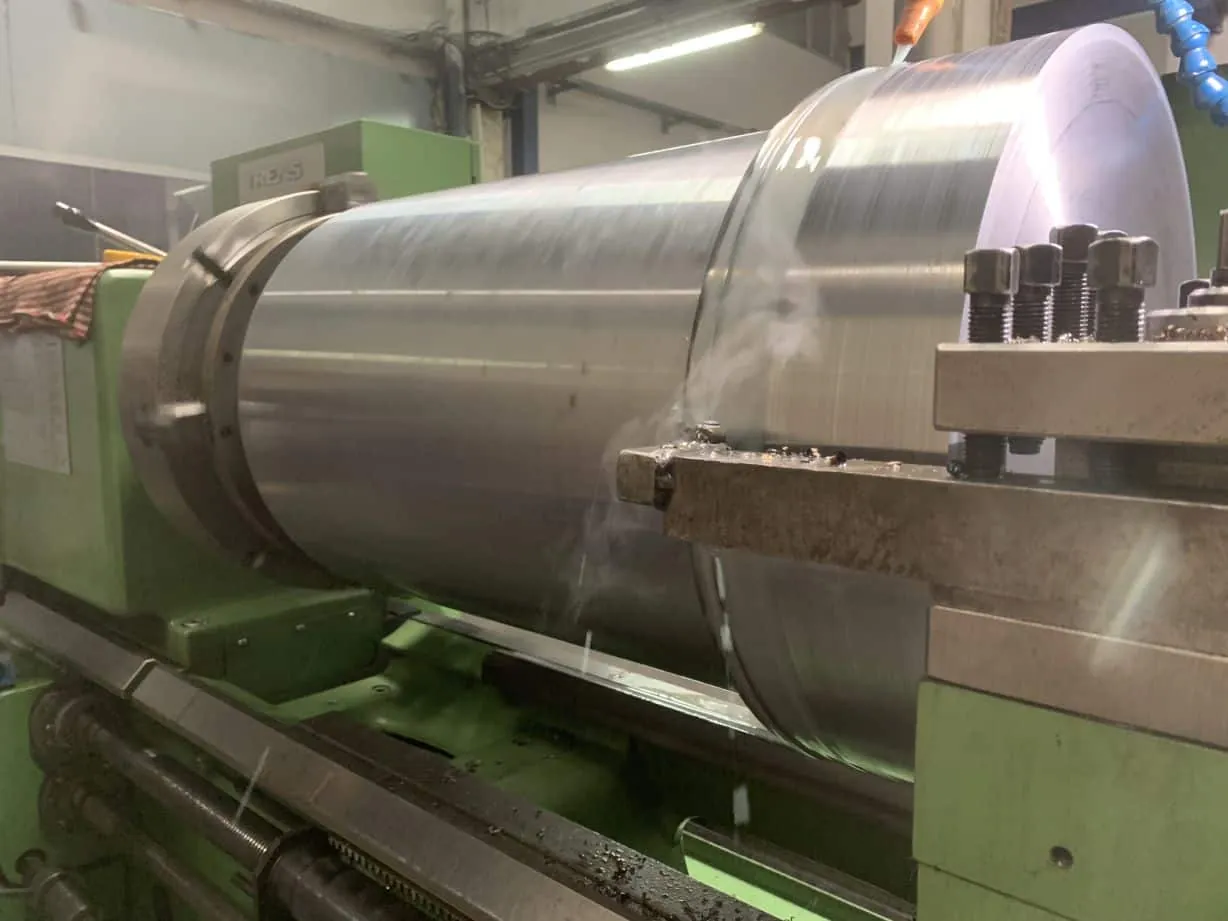
Heavy Lathes, Roll Grinders and CNC Turning Cells
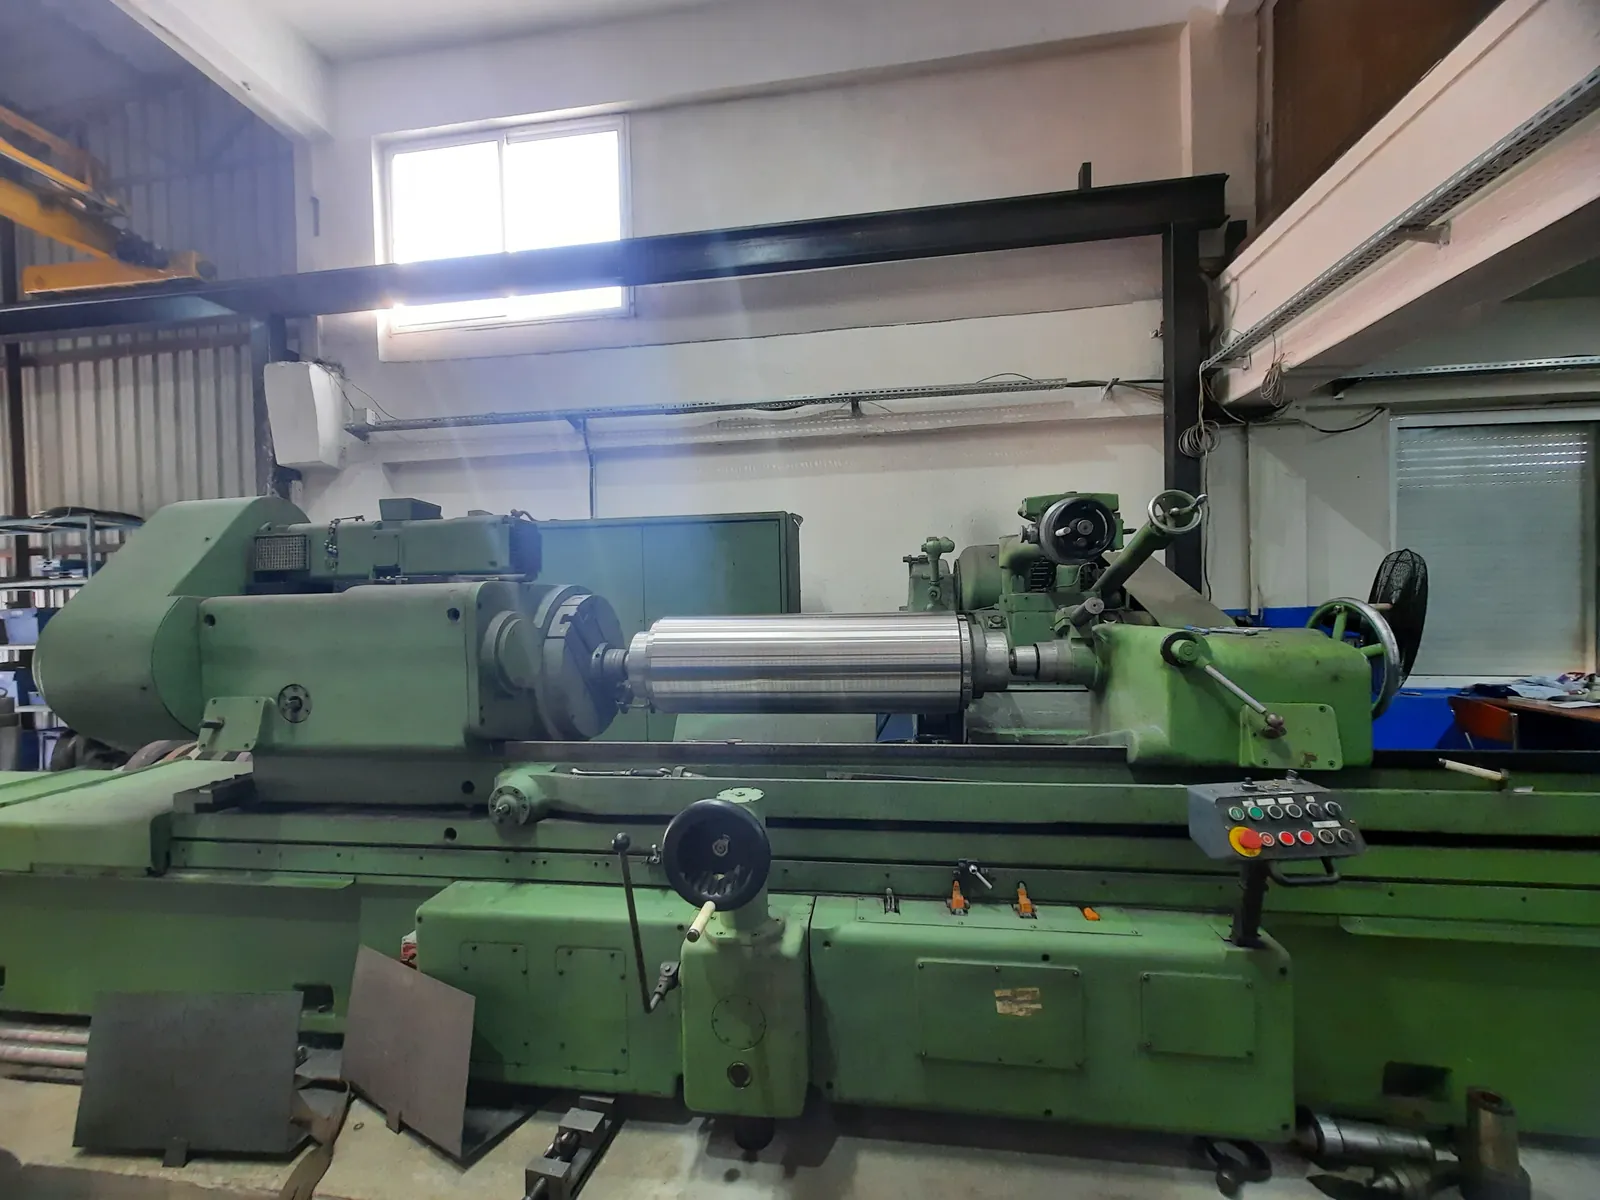
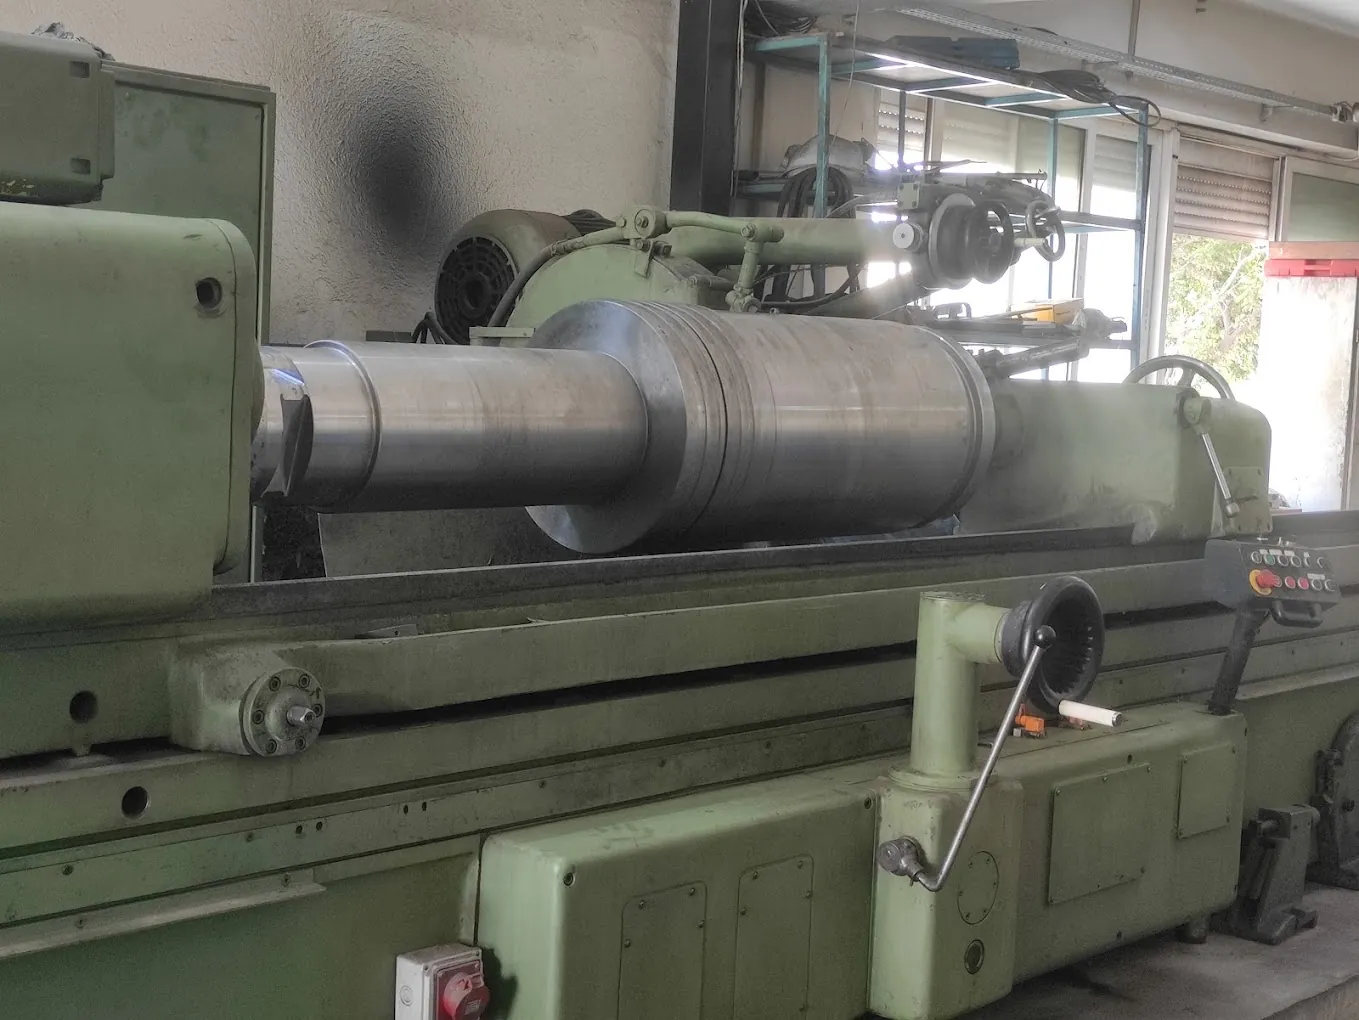
Large rolls are turned on our heavy lathe, ground between centres on long-bed cylindrical grinders and finished in the chrome and honing lines. Series parts run on CNC turning centres, including a robot-loaded cell.
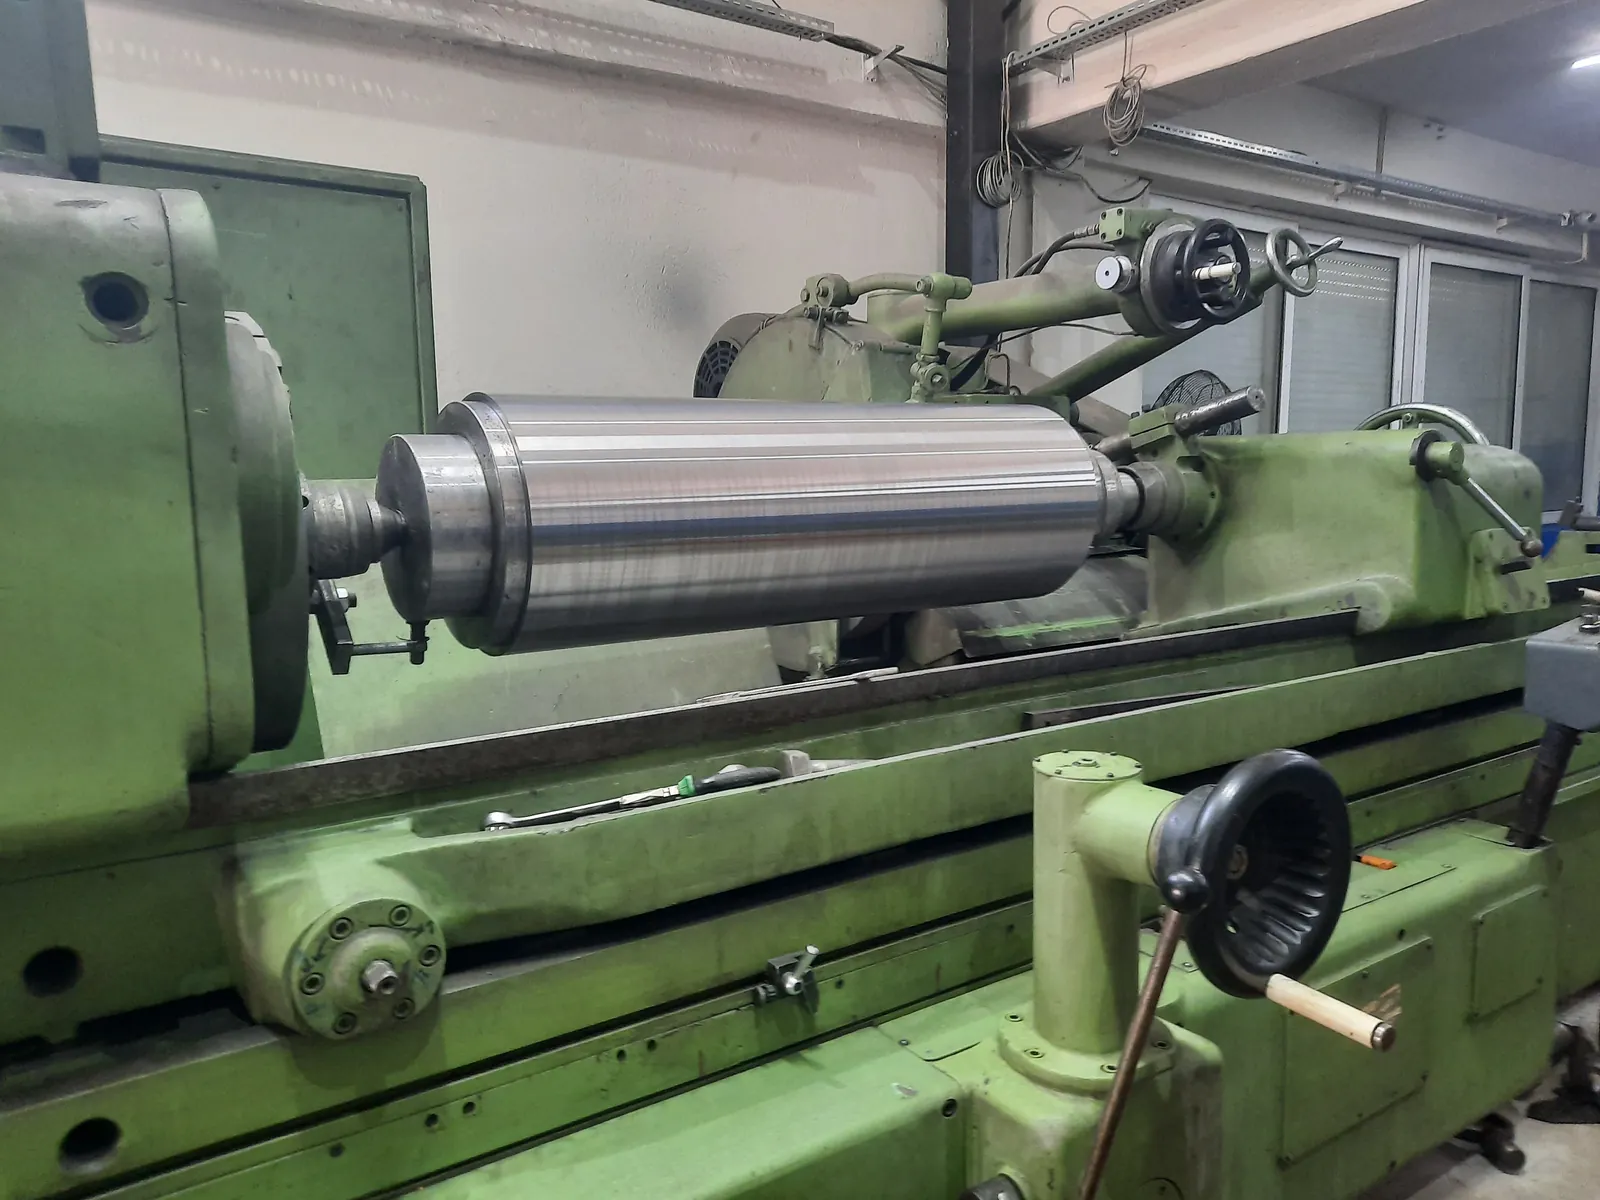
Heavy Turning up to Ø3,200 mm and 12 Tonnes
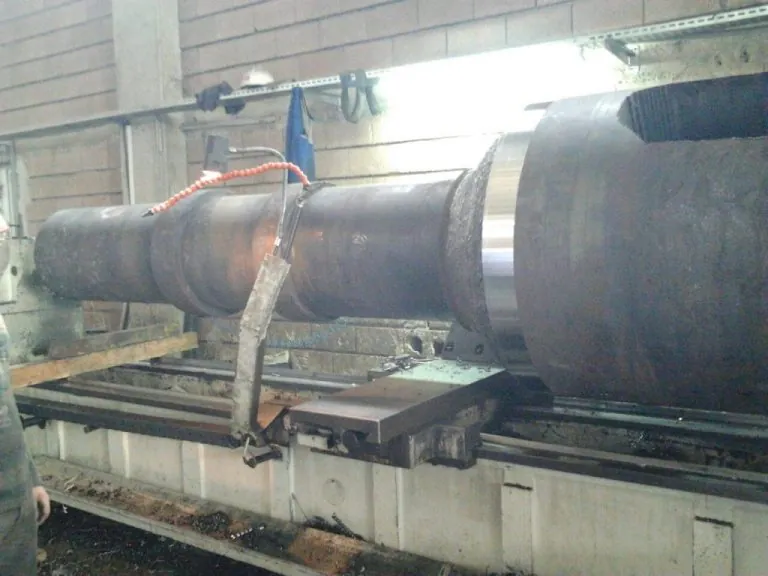
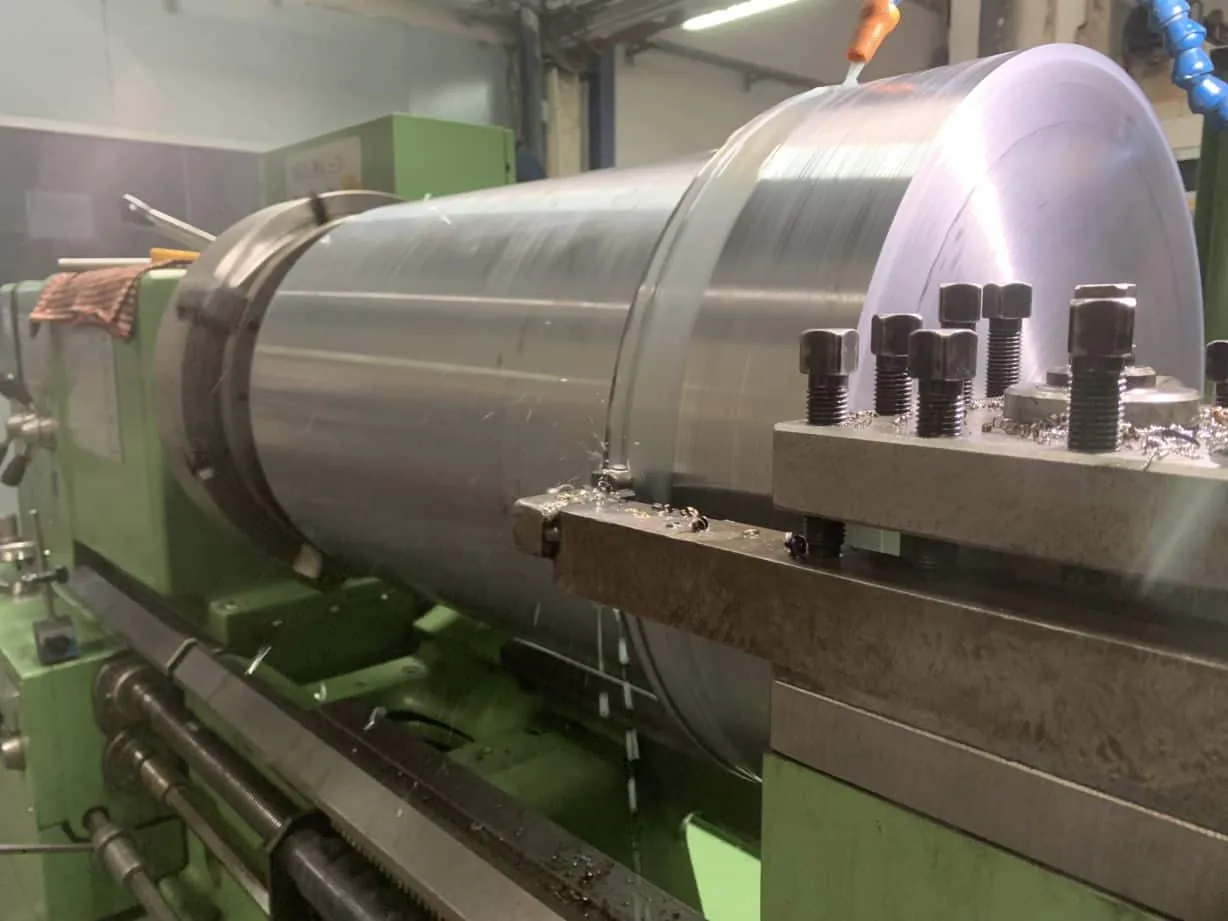
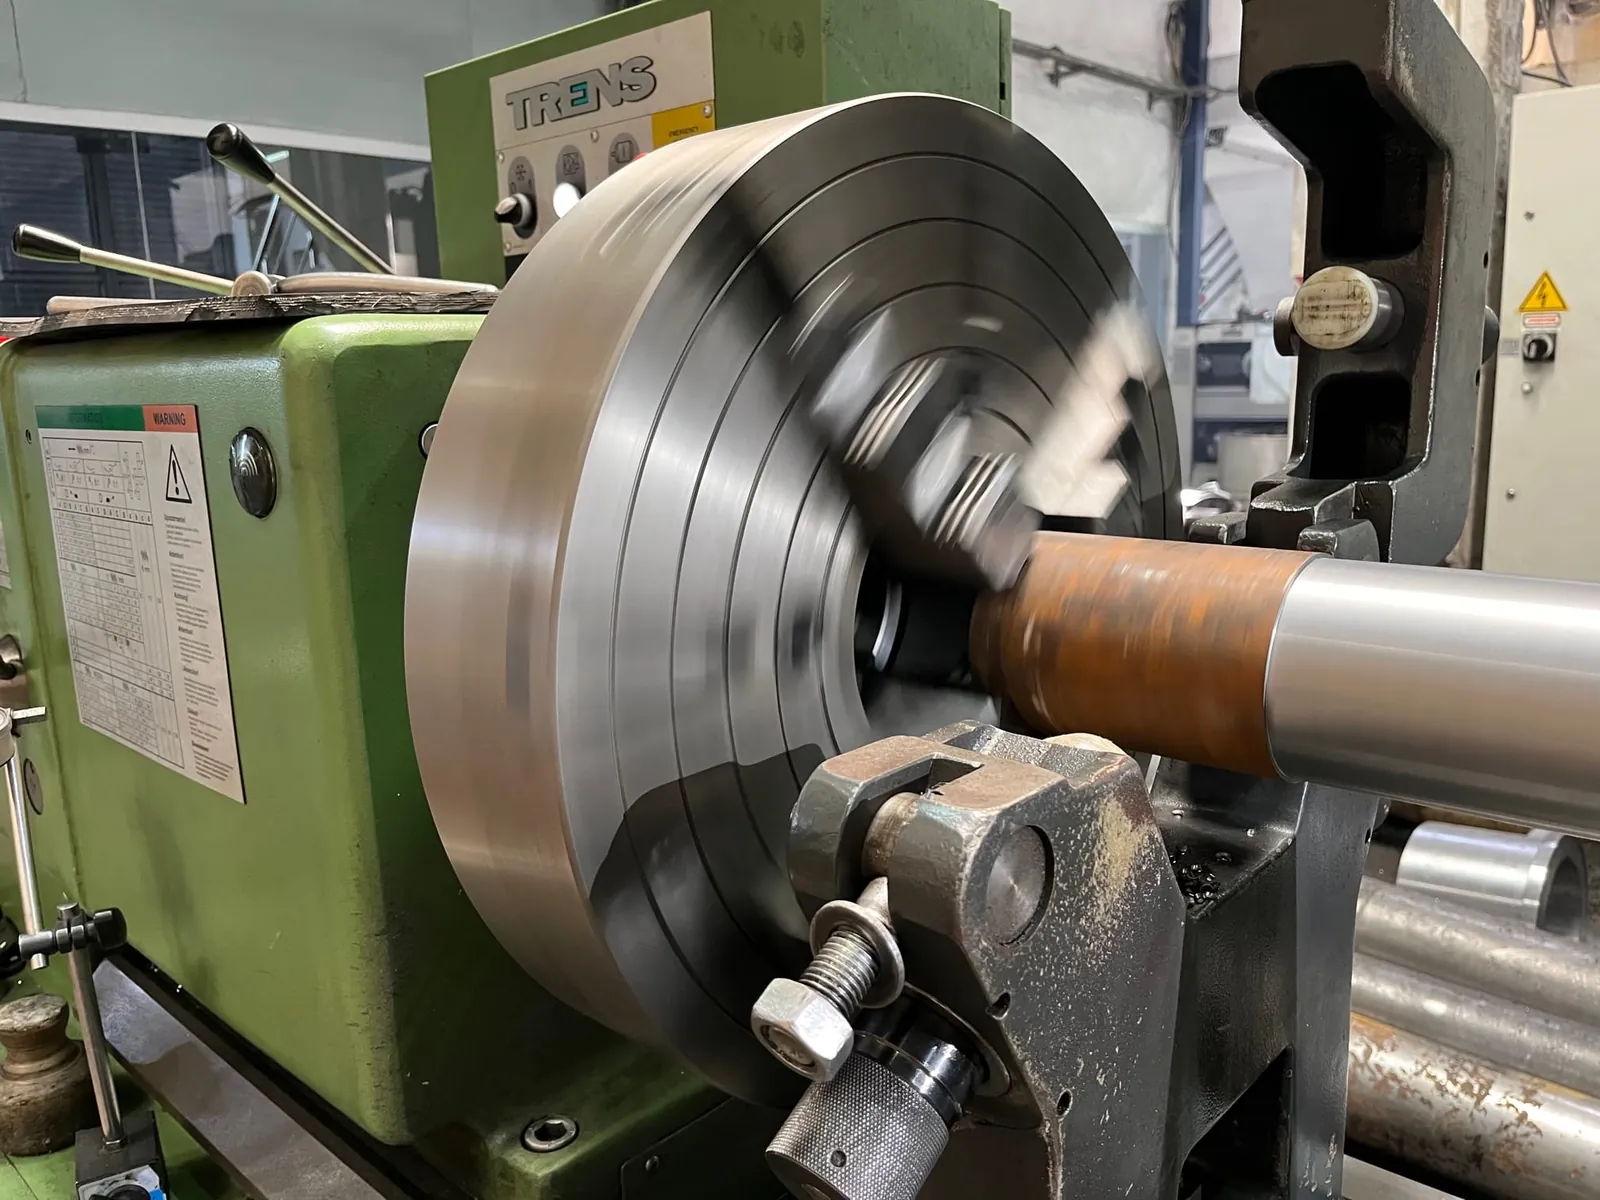
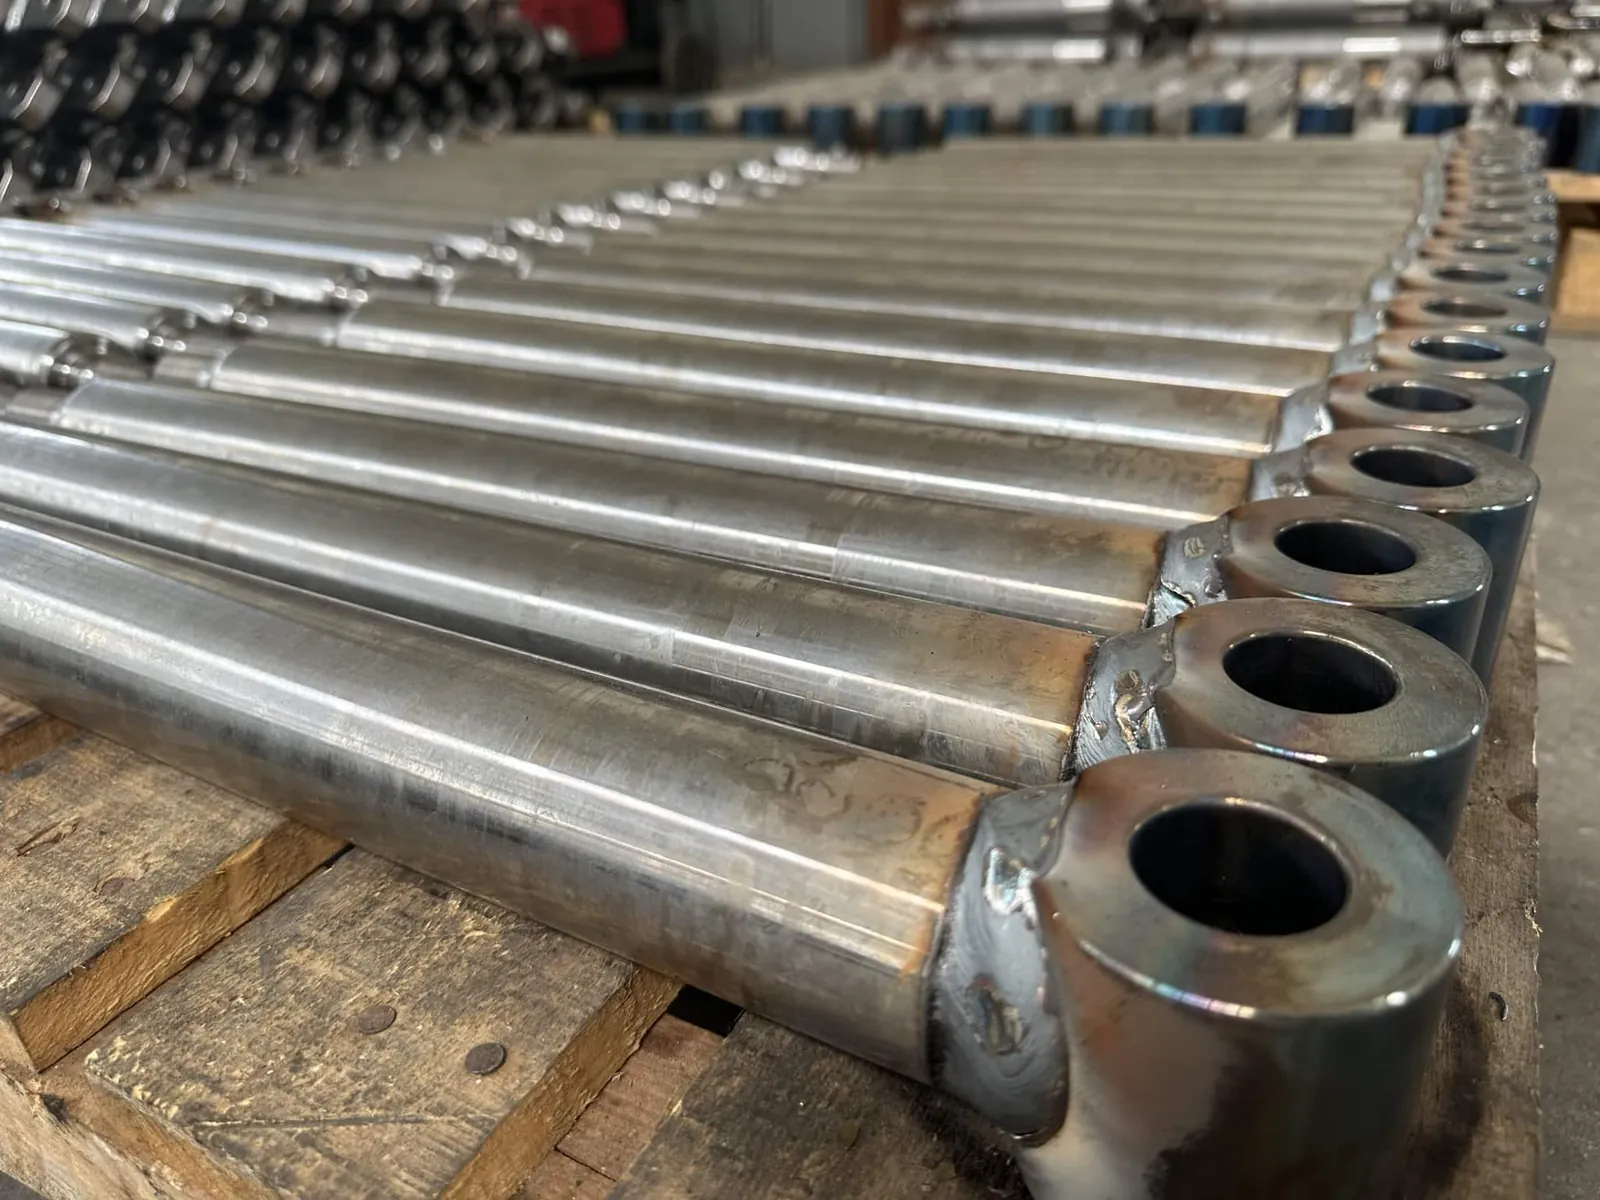
Every roller starts on a lathe. Our heavy lathe in Pınarbaşı, İzmir swings roller bodies and drum shells up to 3,200 mm in diameter and 6,000 mm long, weighing up to 12 tonnes. Large drums are clamped on the faceplate or in the chuck and turned in stages, with stock planned for grinding when the drawing calls for it.
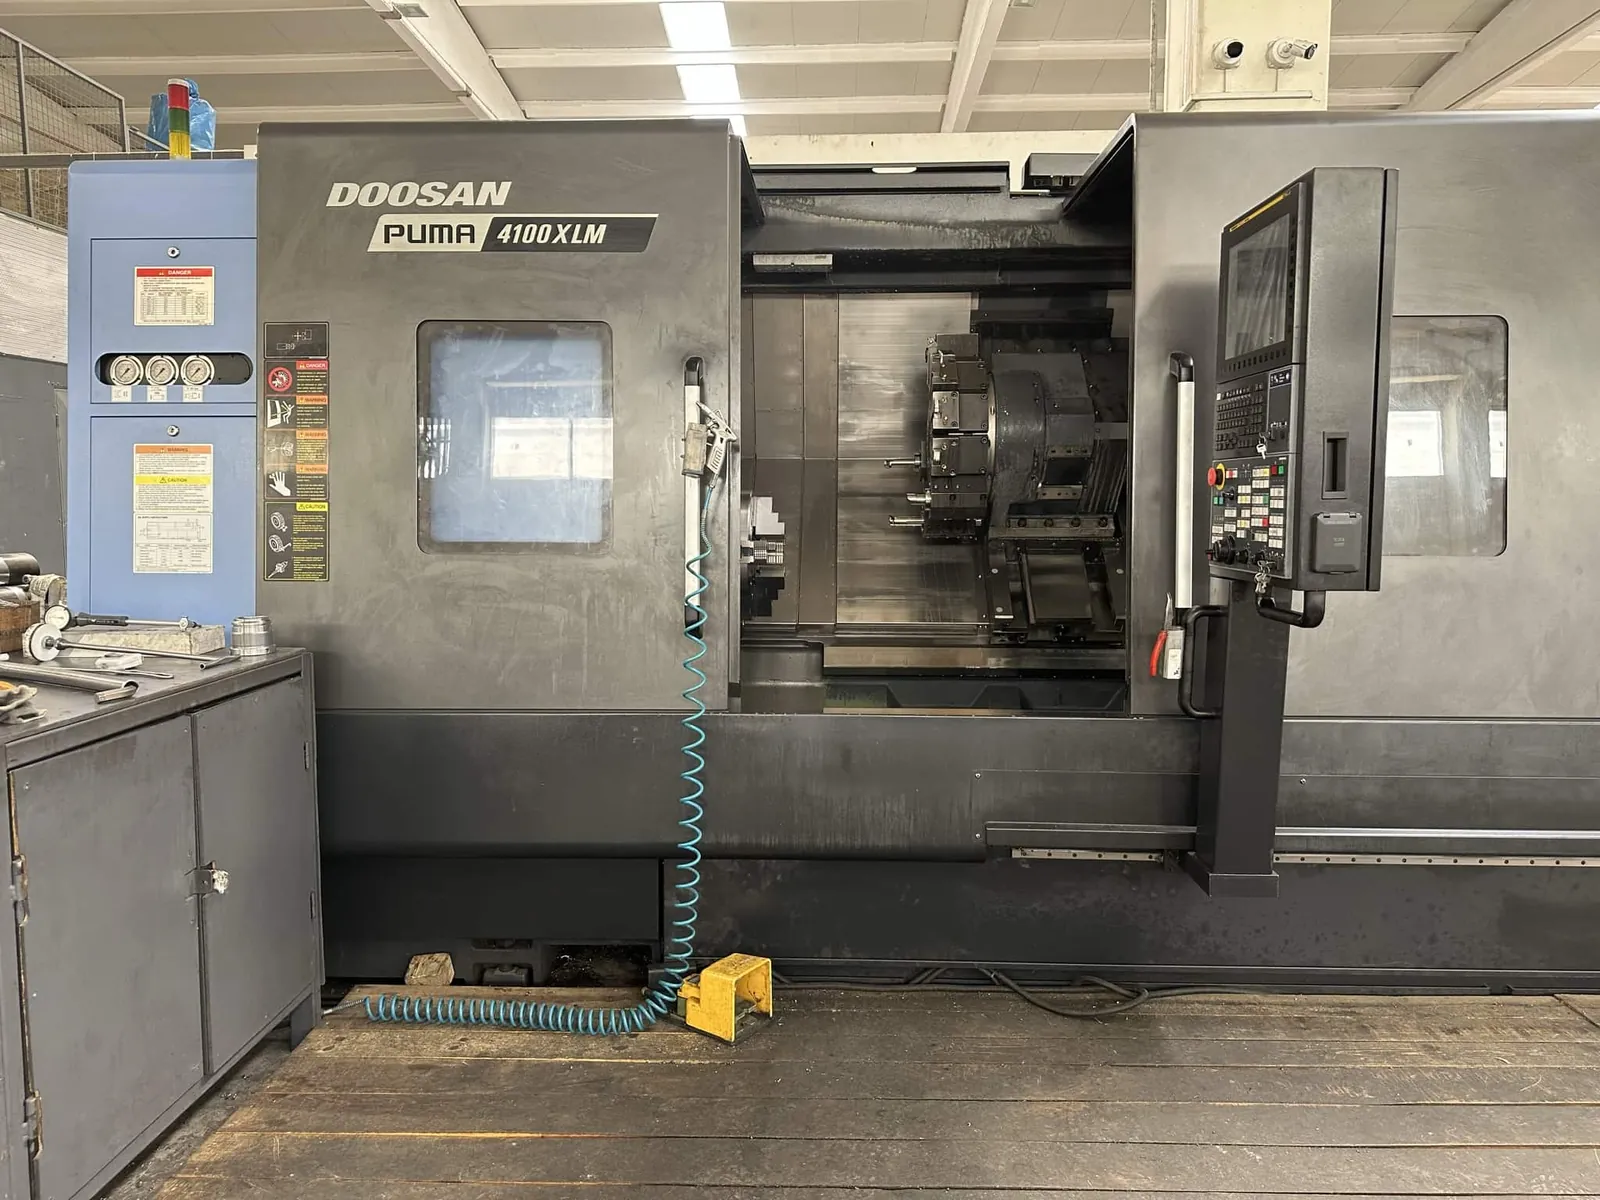
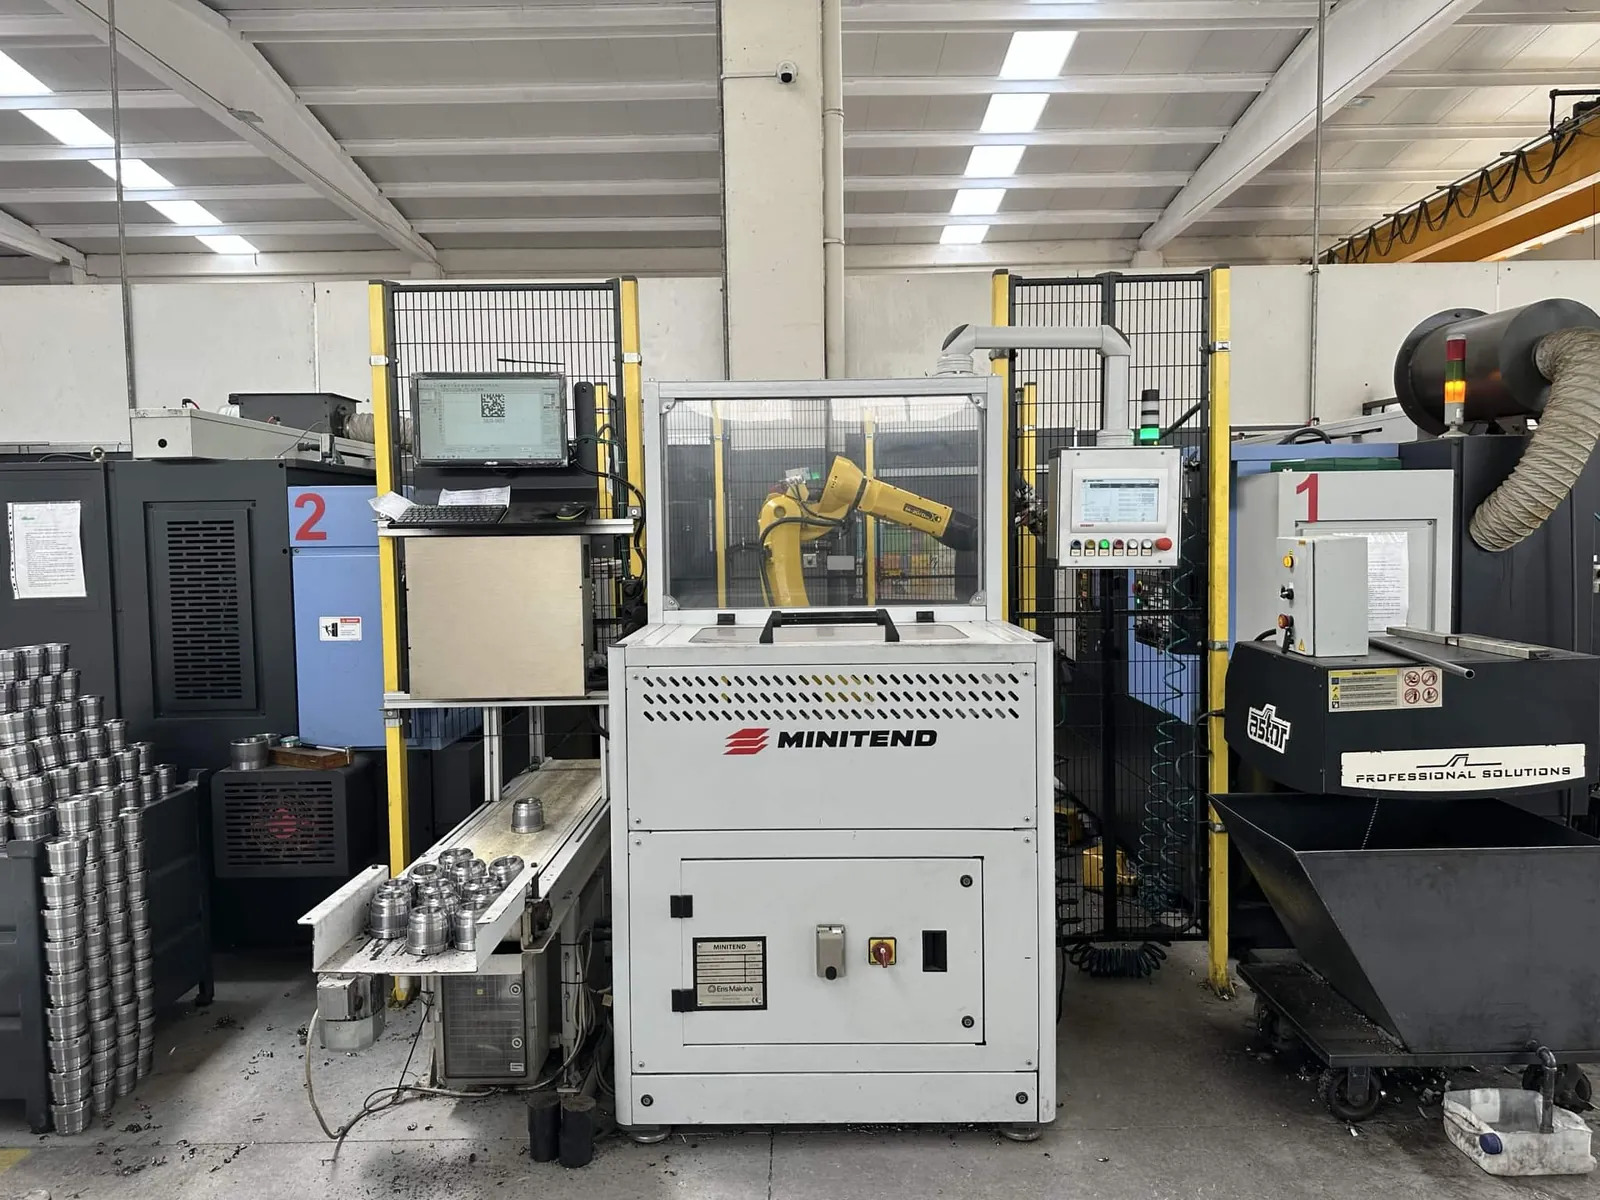
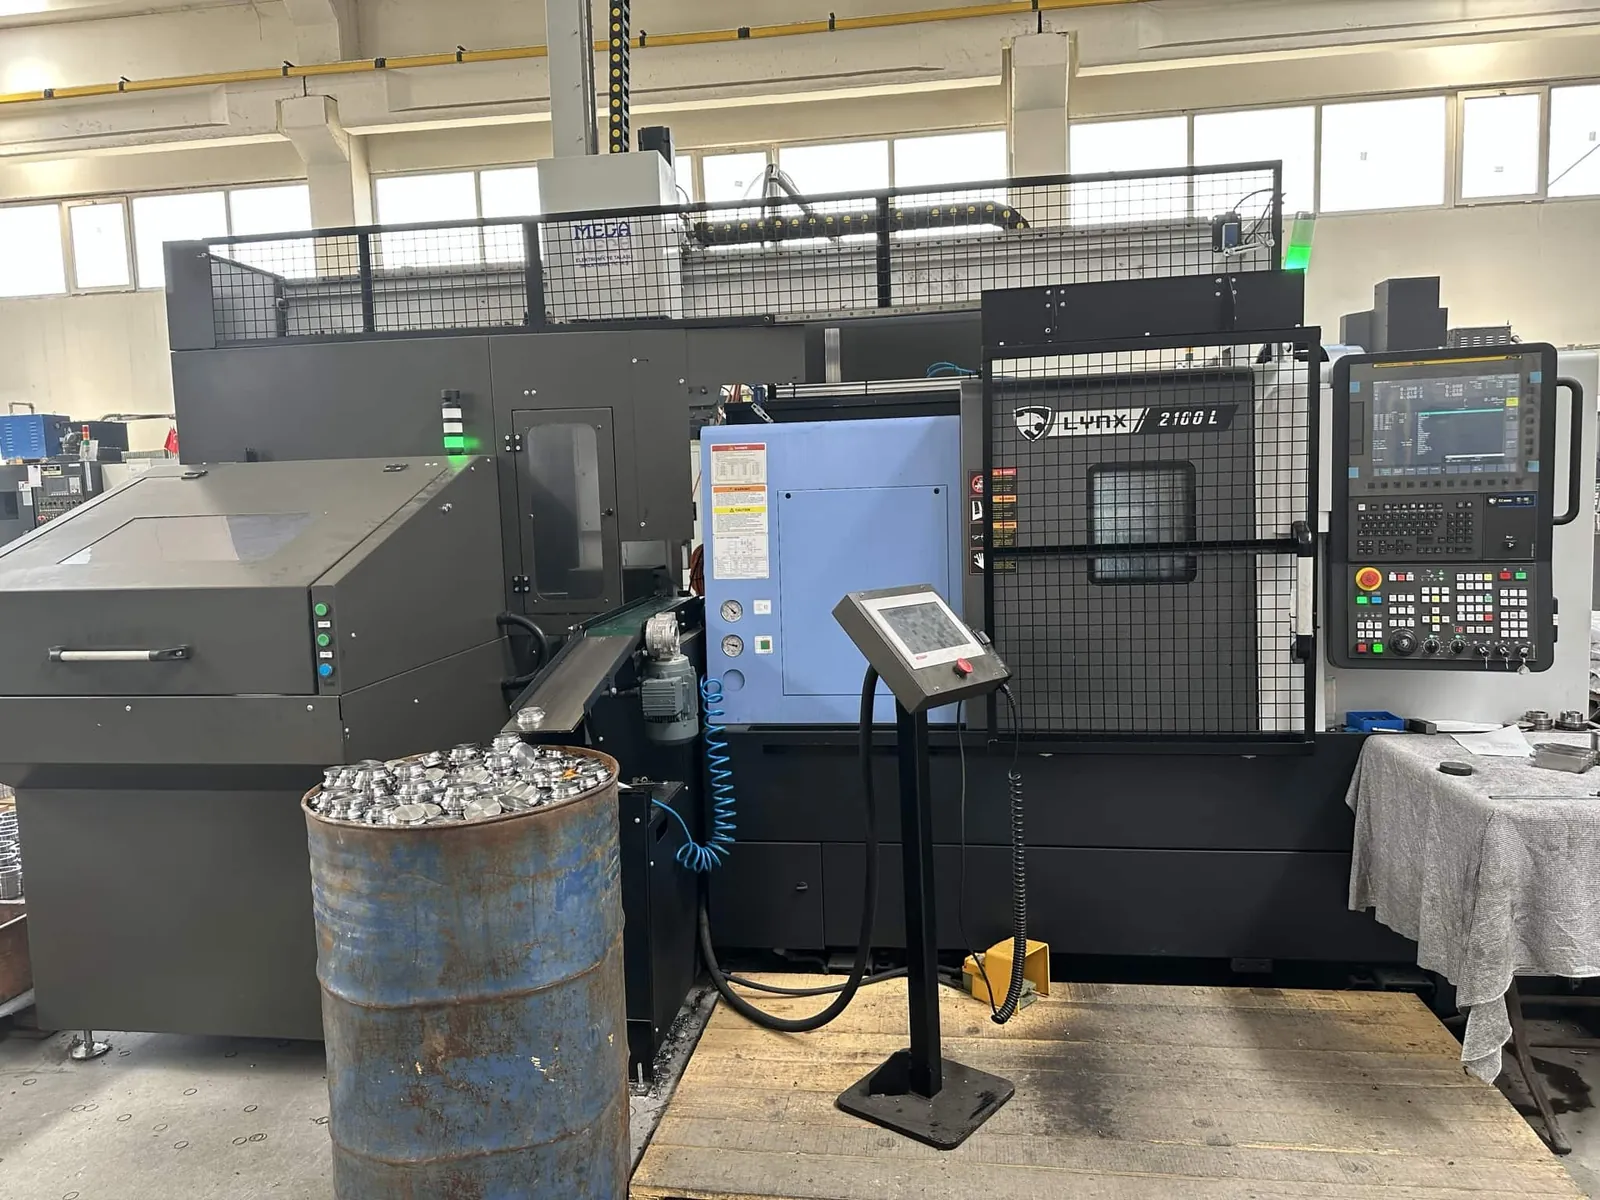
For shafts, journals, hubs and series rollers we run CNC turning centres, including a Doosan Puma 4100XLM and a robot-loaded turning cell for repeat batches without operator loading.
- Roller shells, drum bodies, end discs and hubs
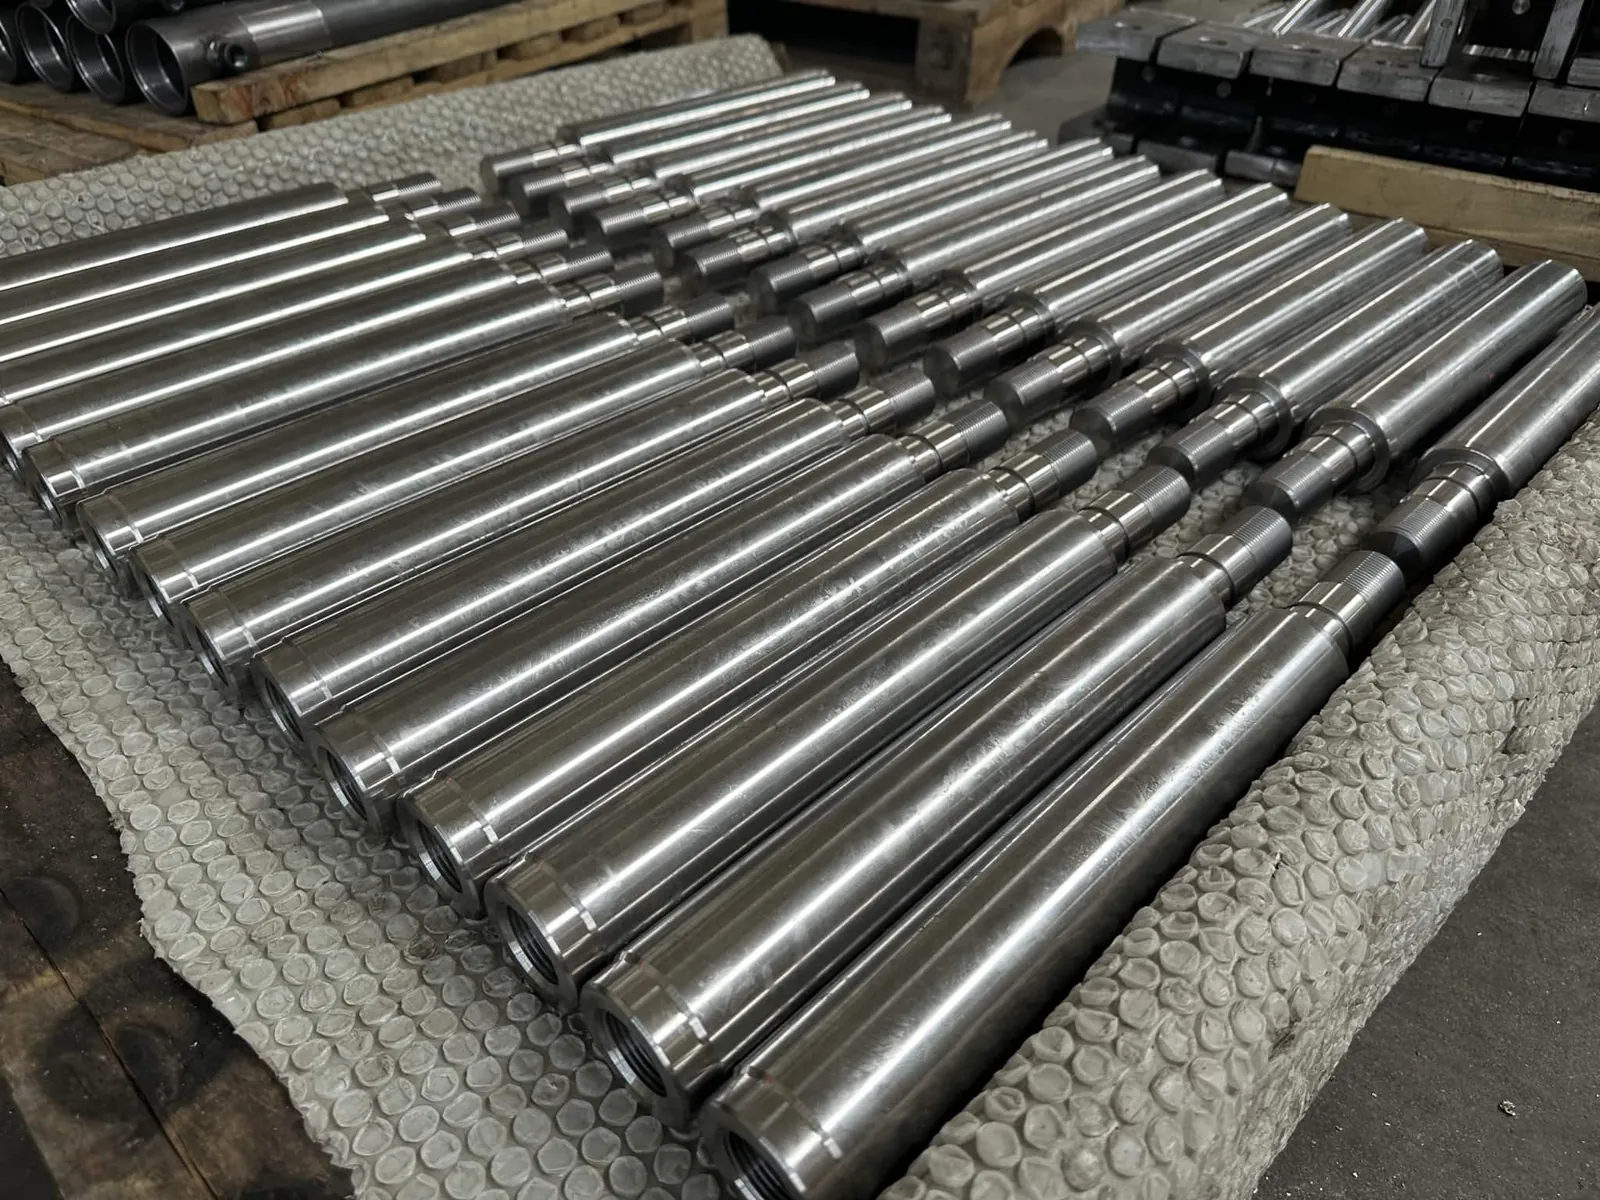
- Long roll shafts with stepped journals and bearing seats
- Series turning of idler rollers, sleeves and housings
Roll Grinding up to Ø3,200 mm, to 0.01 mm and Ra 0.2 µm
Grinding is how a turned roll becomes a precision roll. After turning, the roll is mounted between centres and rotated while a fine-grain grinding wheel removes material from its surface. This corrects size, roundness and runout, and leaves a surface finish no lathe can reach.
On rolls we hold 0.01 mm size and runout with surface roughness down to Ra 0.2 µm. On smaller cylindrical and flat precision parts we hold ±0.005 mm. Grinding is also the step before and after hard chrome plating, so plated rolls come out true and smooth.
Roll grinding service →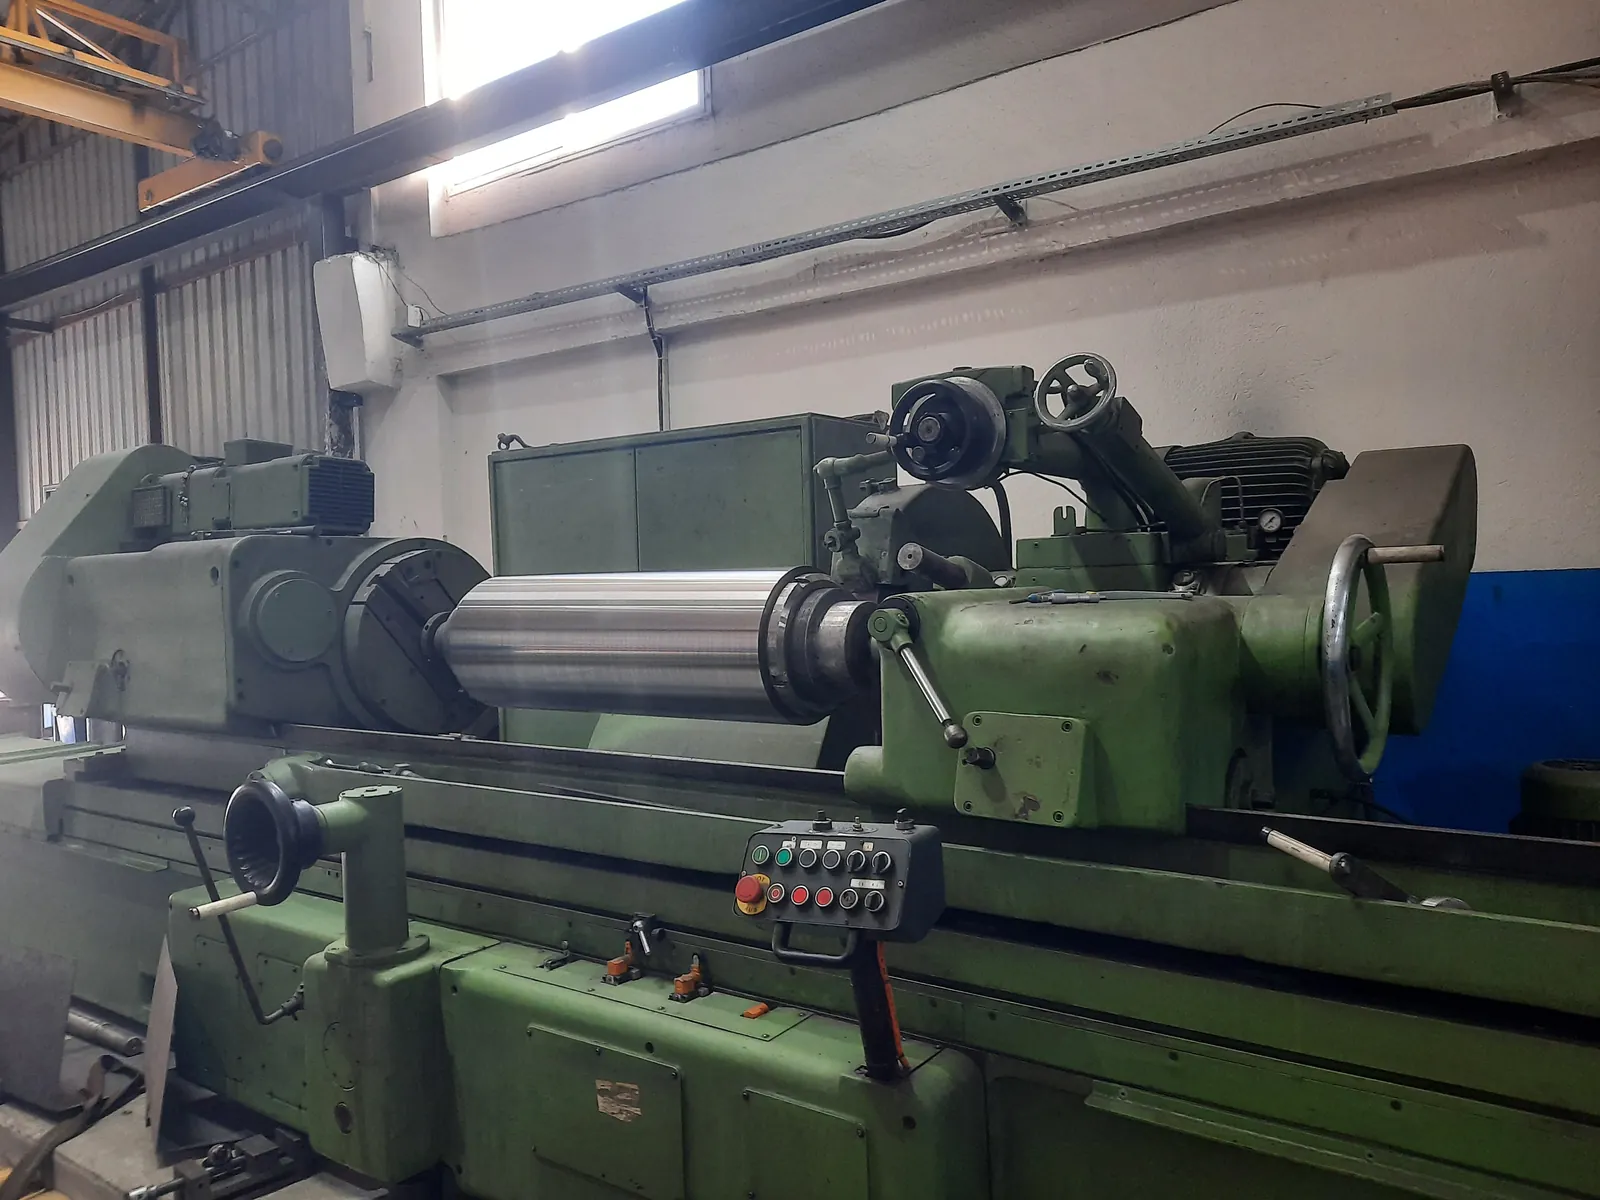
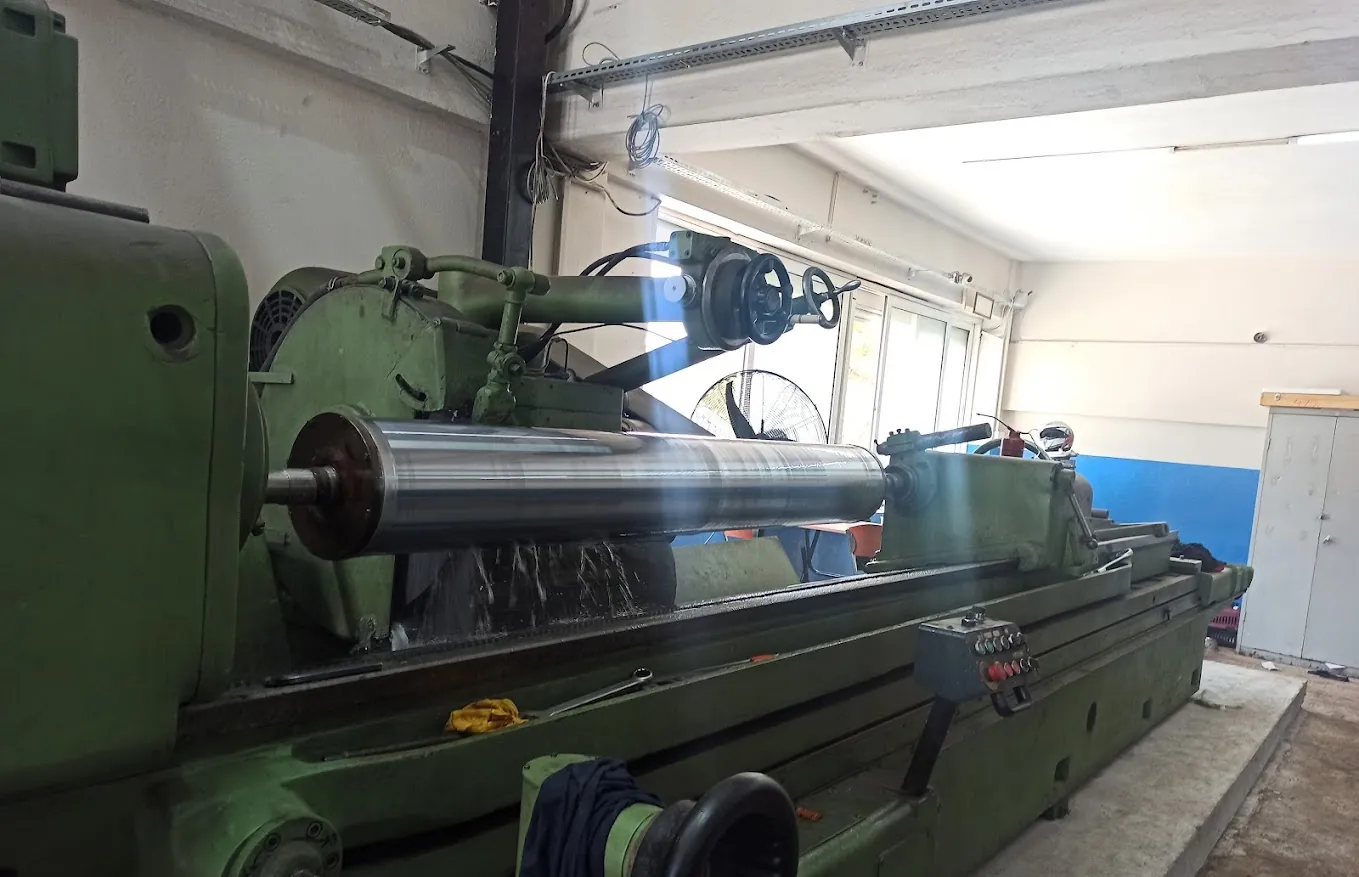
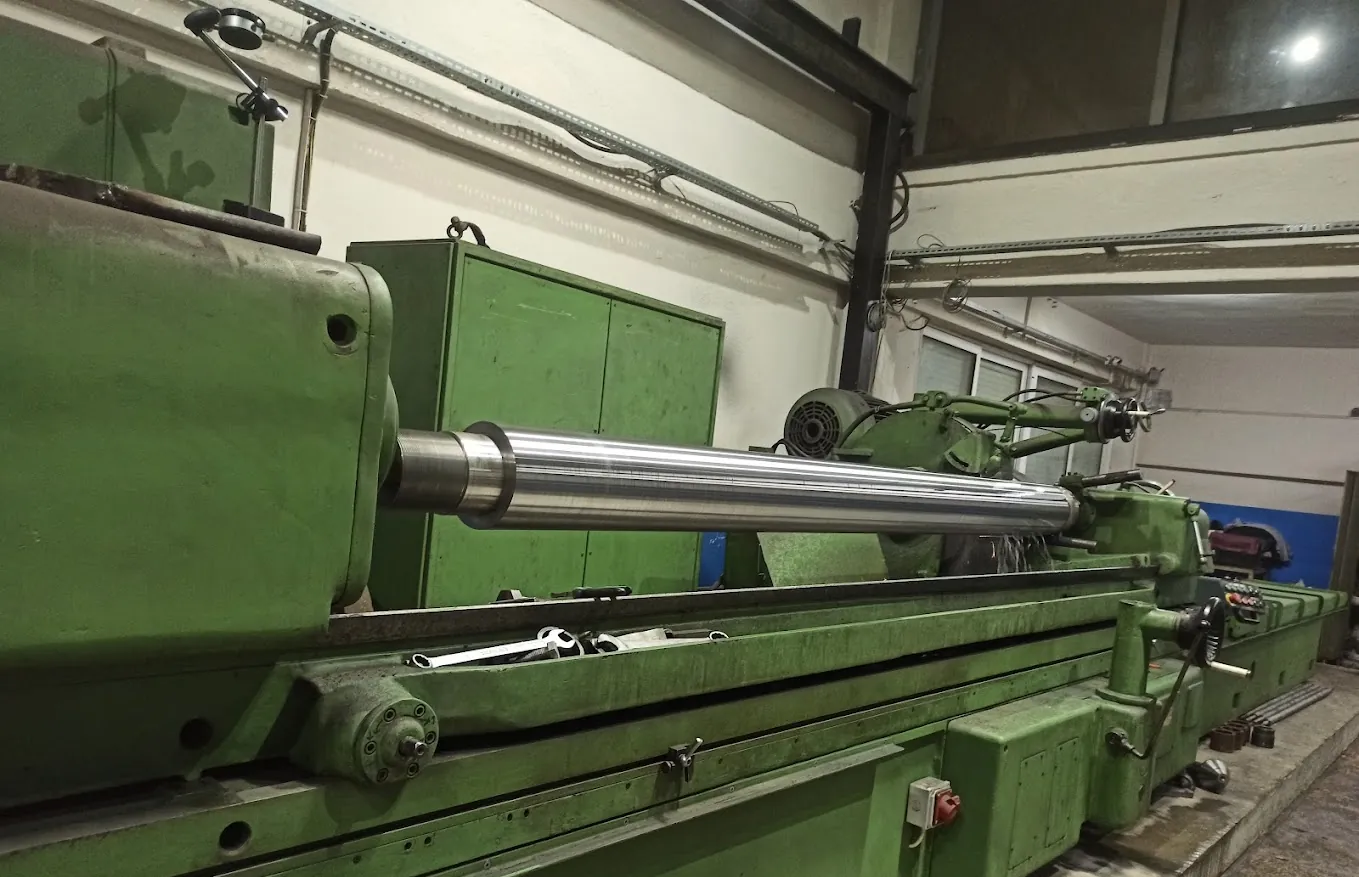
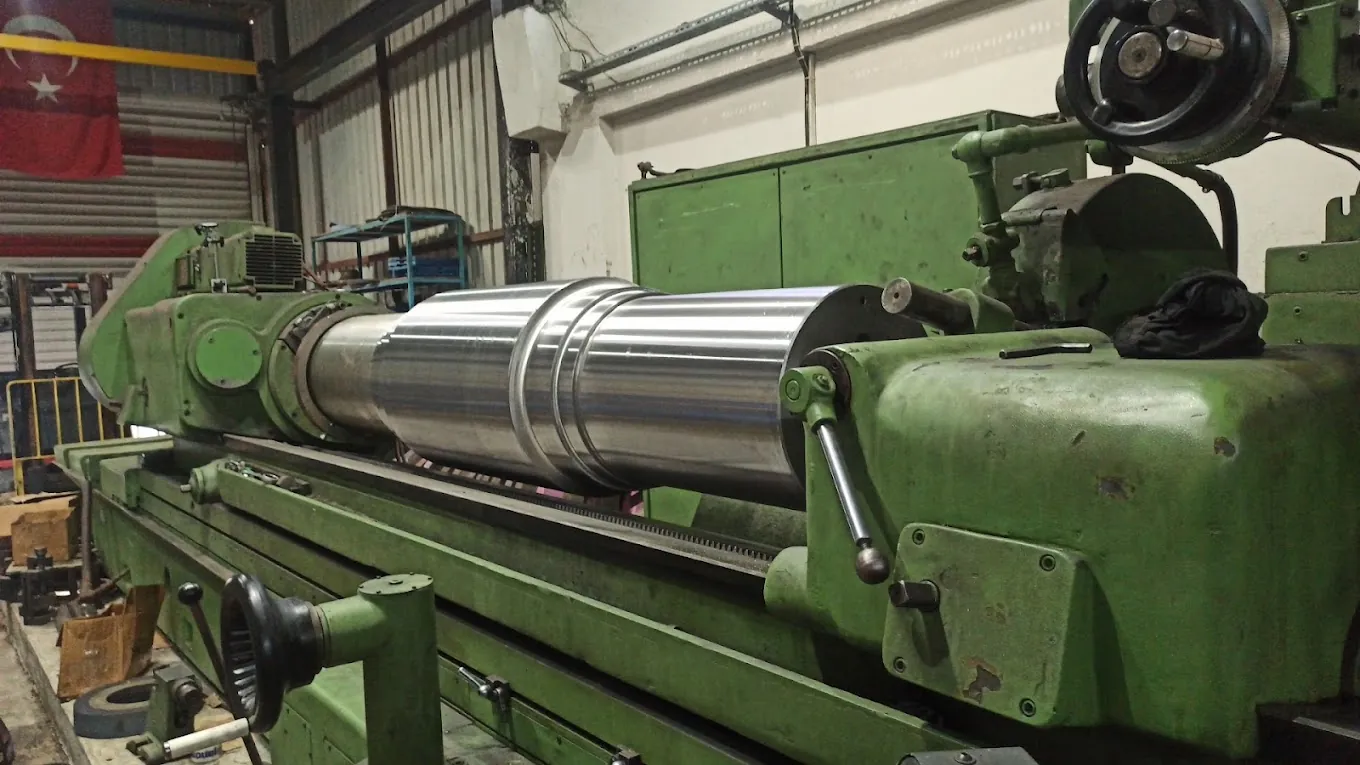
Standard cylindrical grinding machines
| Machine | Origin | Max. diameter | Max. length | Qty |
|---|---|---|---|---|
| Naxos-Union | Germany | Ø1,000 mm | 2,500 mm | 1 |
| C.C. | France | Ø800 mm | 3,000 mm | 1 |
| Friedrich Schmaltz | Germany | Ø600 mm | 4,000 mm | 1 |
| Stanko | Russia | Ø600 mm | 4,000 mm | 1 |
| Naxos-Union | Germany | Ø600 mm | 3,500 mm | 1 |
| Titan (cylindrical, internal & surface) | – | Ø470 mm | 3,000 mm | 1 |
| Johnsson (cylindrical, internal & surface) | – | Ø470 mm | 1,800 mm | 1 |
| Cincinnati | USA | Ø350 mm | 2,000 mm | 2 |
| Fortuna | Germany | Ø350 mm | 1,000 mm | 1 |
| Taksan (cylindrical, internal & surface) | Türkiye | Ø320 mm | 1,000 mm | 1 |
Internal and surface grinding
| Process | Capacity |
|---|---|
| Internal (bore) grinding, small bores | Bores down to Ø3 mm (Taksan) |
| Internal (bore) grinding, deep bores | Bores from Ø90 mm, up to 1,000 mm deep (Titan) |
| Internal grinding, medium parts | Up to Ø470 mm parts (Johnsson) |
| Surface grinding | 1,700 × 600 mm table, 380 mm height, plates up to 700 kg |
Rolls larger than the machines listed, up to Ø3,200 mm, are ground on request. Surface grinding gives flat parts their parallelism and surface quality. Size accuracy on flat and cylindrical precision parts: ±0.005 mm.
Grinding of Slitting Knives, Shear Blades and Granulator Blades
The same precision grinders also resharpen and regrind industrial knives and blades, a regular service for metal service centres, sheet-metal shops and plastics recyclers.
Slitting knives
Circular knives for coil slitting lines, ground for clean, burr-free cuts.
Shear blades
Long blades for guillotine shears and plate cutting, ground straight along their full length.
Granulator blades
Blades for plastic crushers and granulators, restored to a sharp, even edge.
Cobalt HSS knives
Cobalt high-speed-steel knives ground to their original geometry.
Hard Chrome Plating up to Ø3,200 mm
Hard chrome gives rolls, piston rods and shafts a hard, wear- and corrosion-resistant surface. Rolls are ground before plating, plated in our tanks, then ground again to final size and finish. For rechroming, a separate stripping tank removes the old chrome layer first.
| Tank: max. diameter | Max. length | Rectifier | Qty |
|---|---|---|---|
| Ø1,300 mm | 1,500 mm | 380 V / 15 V, 25,000 A | 1 |
| Ø900 mm | 5,000 mm | 380 V / 15 V, 10,000 A | 1 |
| Ø900 mm | 3,600 mm | 380 V / 15 V, 4,000 A | 1 |
| Ø800 mm | 3,000 mm | 380 V / 15 V, 6,000 A | 1 |
| Ø750 mm | 1,500 mm | 380 V / 15 V, 3,000 A | 1 |
| Chrome stripping tank: 1,000 × 1,100 × 3,000 mm | 380 V / 15 V, 4,000 A | 1 | |
Standard tanks listed above; rolls up to Ø3,200 mm are plated on request.
Deep Bore Honing up to Ø550 mm and 6,000 mm
Honing finishes the inside of a bore to a precise size, roundness and cross-hatch surface. It is essential for hydraulic cylinder barrels, where the seal runs on the bore, and for hollow rolls that need a true internal diameter.
| Max. bore diameter | Max. depth | Qty |
|---|---|---|
| Ø550 mm | 6,000 mm | 1 |
| Ø550 mm | 3,500 mm | 1 |
| Ø350 mm | 2,000 mm | 1 |
| Ø300 mm | 2,000 mm | 1 |
| Ø300 mm | 1,200 mm | 1 |
| Ø200 mm | 400 mm | 1 |
Everything Else a Roll Needs
Dynamic balancing
Rollers and drums are dynamically balanced after machining, so they run smoothly at line speed and bearings last longer.
Balancing →Certified welding
Shells, end discs and shafts are welded under EN 1090 EXC3 and ISO 3834-2, including KUKA robot welding for series parts.
Welding at Nika Steelworks →Lagging & coatings
Rubber and ceramic lagging, rubber and polyurethane covers, painting and galvanizing to your specification.
Lagged drums →Questions About Our Machine Capacity
What is your maximum cylindrical grinding size?
We grind rolls up to Ø3,200 mm. Our standard cylindrical grinders cover Ø320 mm to Ø1,000 mm and lengths up to 4,000 mm; larger rolls are ground up to Ø3,200 mm on request.
What tolerance and surface finish can you achieve by grinding?
Rolls are ground to 0.01 mm size and runout with surface roughness down to Ra 0.2 µm. On smaller precision cylindrical and flat parts we hold ±0.005 mm.
What size rolls can you hard chrome plate?
We hard chrome plate rolls up to Ø3,200 mm. Standard tanks take up to Ø1,300 mm × 1,500 mm, or Ø900 mm × 5,000 mm for long rolls; larger rolls are plated on request. A separate stripping tank removes old chrome before rechroming.
Can you hone hydraulic cylinder barrels?
Yes. We hone bores up to Ø550 mm and up to 6,000 mm deep, which covers most hydraulic cylinder barrels and tubes.
One Supplier for Turning, Grinding, Chroming and Honing Rolls
Buying a precision roll often means sending it to three or four shops: one to turn it, one to grind it, one to plate it and another to grind it again. Every transfer adds transport, lead time and the risk that nobody owns the final tolerance. At Nika Rollers, the whole route runs under one order, from the large roller shell on the heavy lathe to the ground, chromed and balanced roll in its crate.
Heavy turning for large rollers and drums
Our heavy lathe takes parts up to Ø3,200 mm, 6,000 mm long and 12 tonnes, which covers conveyor drive drums and pulleys, large process rolls and heavy shafts. Parts beyond a standard lathe's swing are exactly the work we are set up for. See our heavy lathe turning services for turned parts beyond rollers.
Cylindrical grinding in Türkiye up to Ø1,000 mm
Ten cylindrical grinders, from German Naxos-Union and Friedrich Schmaltz machines to American Cincinnati grinders, cover rolls from small shafts to Ø1,000 mm and lengths up to 4,000 mm, and larger rolls are ground up to Ø3,200 mm. Rolls are ground to 0.01 mm size and runout and down to Ra 0.2 µm, ready for paper, film, printing and metal-processing lines. Our roll grinding service takes new rolls and worn rolls sent in for regrinding.
Hard chrome plating and rechroming
Five hard chrome tanks with rectifiers up to 25,000 A plate rolls up to Ø1,300 mm, or up to 5,000 mm long at Ø900 mm, and larger rolls are plated up to Ø3,200 mm. Combined with the stripping tank and our grinders, this is a complete rechroming and roll refurbishment line: strip, regrind, plate, finish-grind. See hard chrome plated rolls.
Bore honing for hydraulic cylinders and hollow rolls
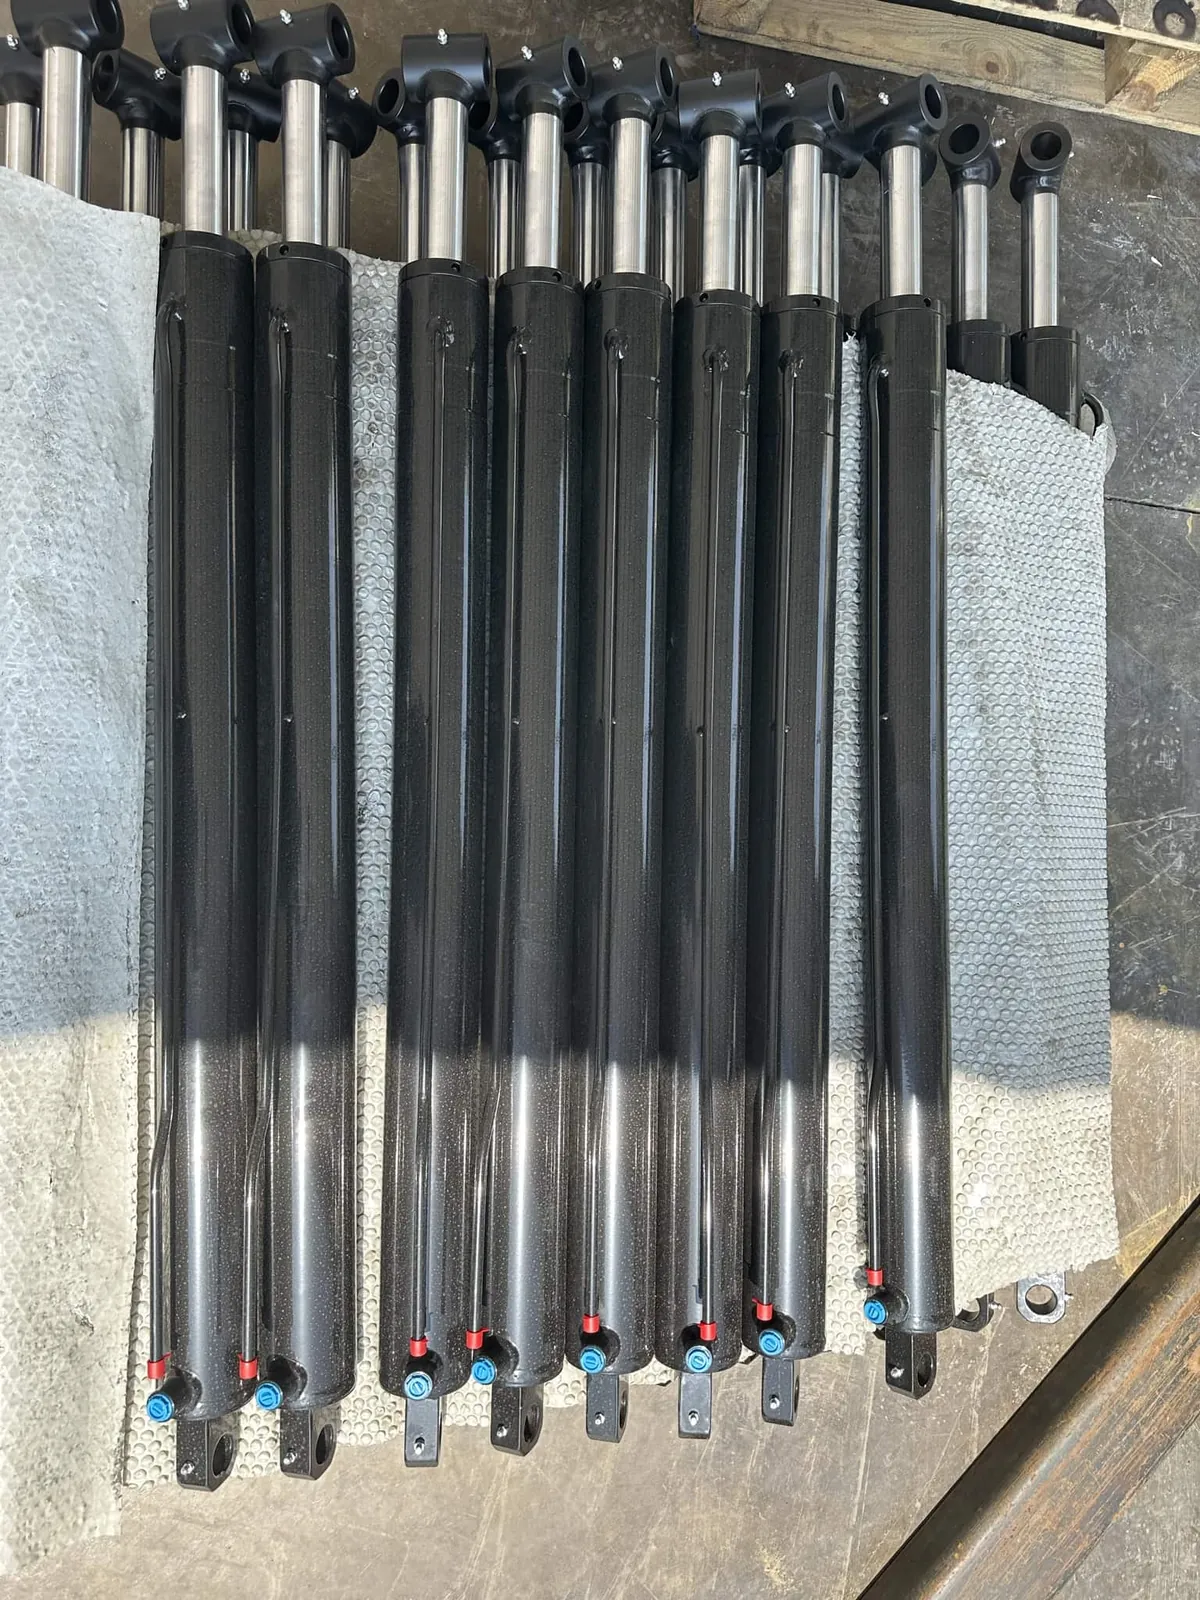
Six honing machines finish bores from Ø200 mm up to Ø550 mm and depths up to 6,000 mm. Together with chrome-plated piston rods, this makes us a full source for hydraulic cylinder pistons, rods and barrels.
To check whether your roll fits our machines, send the outside diameter, length, weight and surface requirement through the contact page. For welding and fabrication capacity, see the Nika Steelworks machine park.