Hard Chrome Plated Rolls and Rechroming
New hard chrome plated rolls and rechroming of worn ones, up to Ø3,200 mm. Each roll is ground before plating and finish-ground after, so it comes out hard, smooth and true.
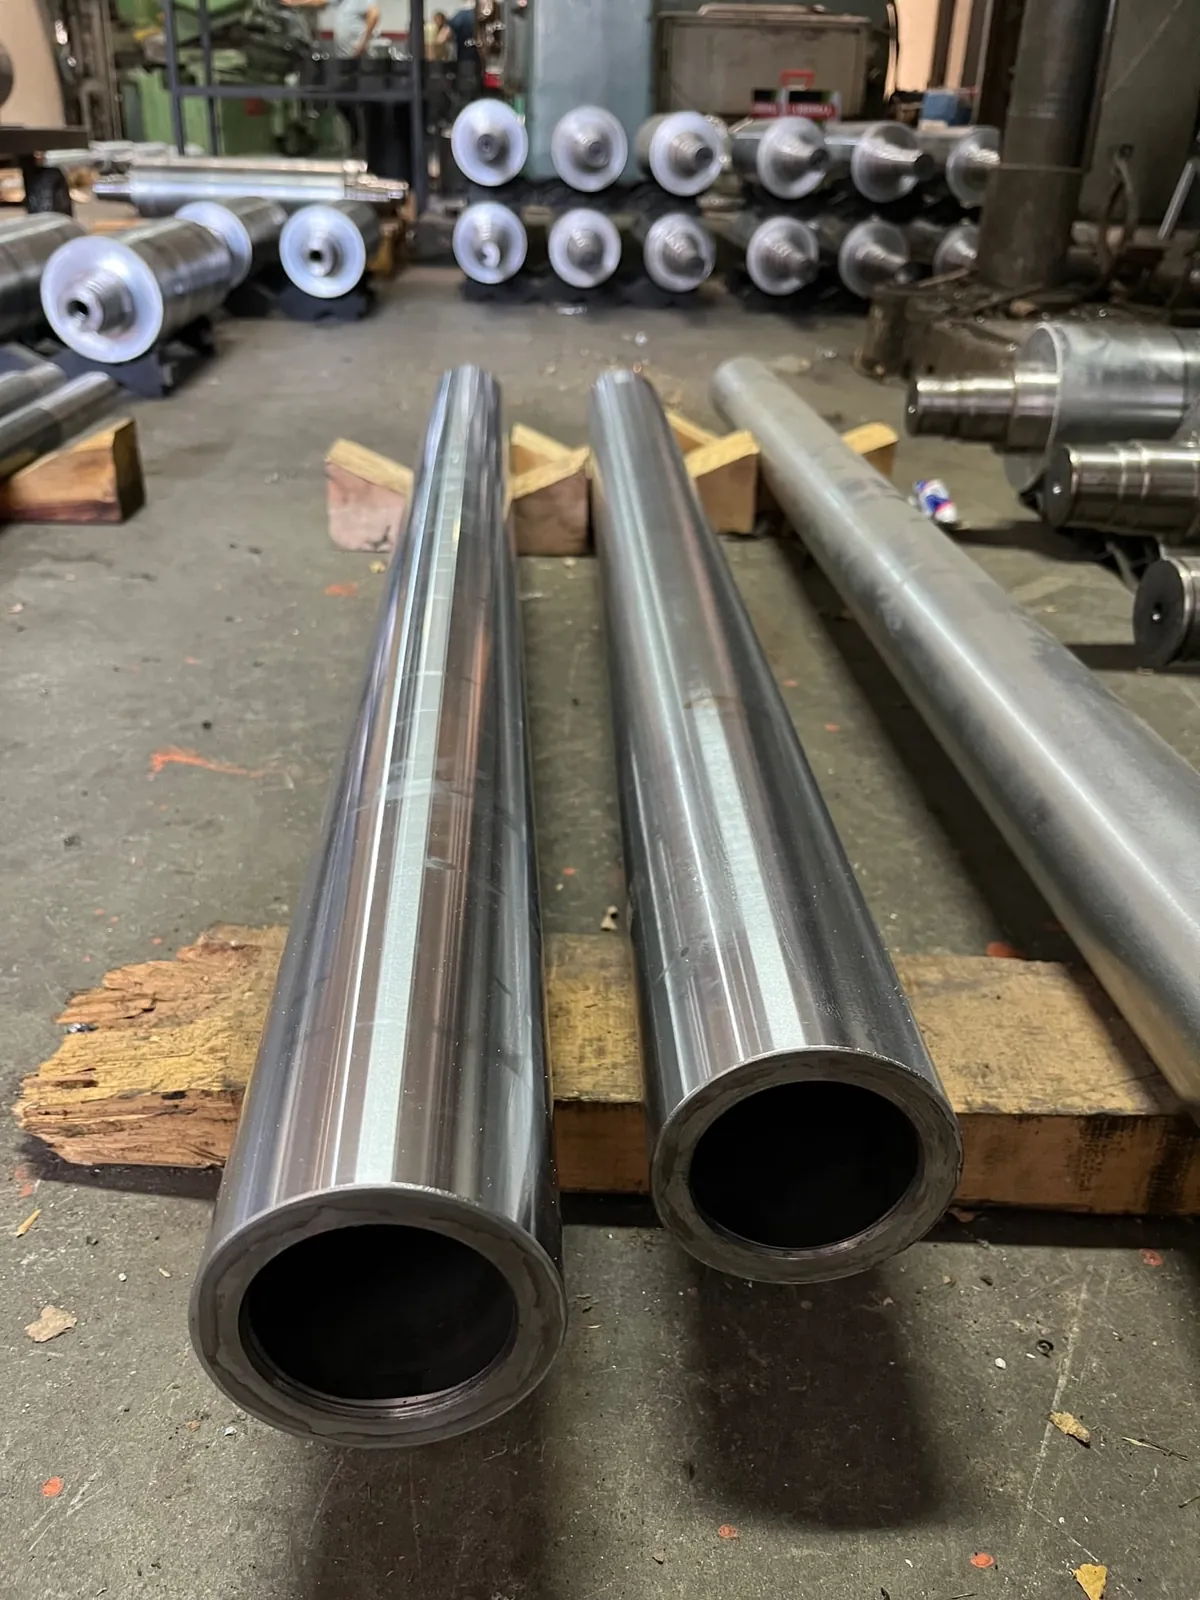
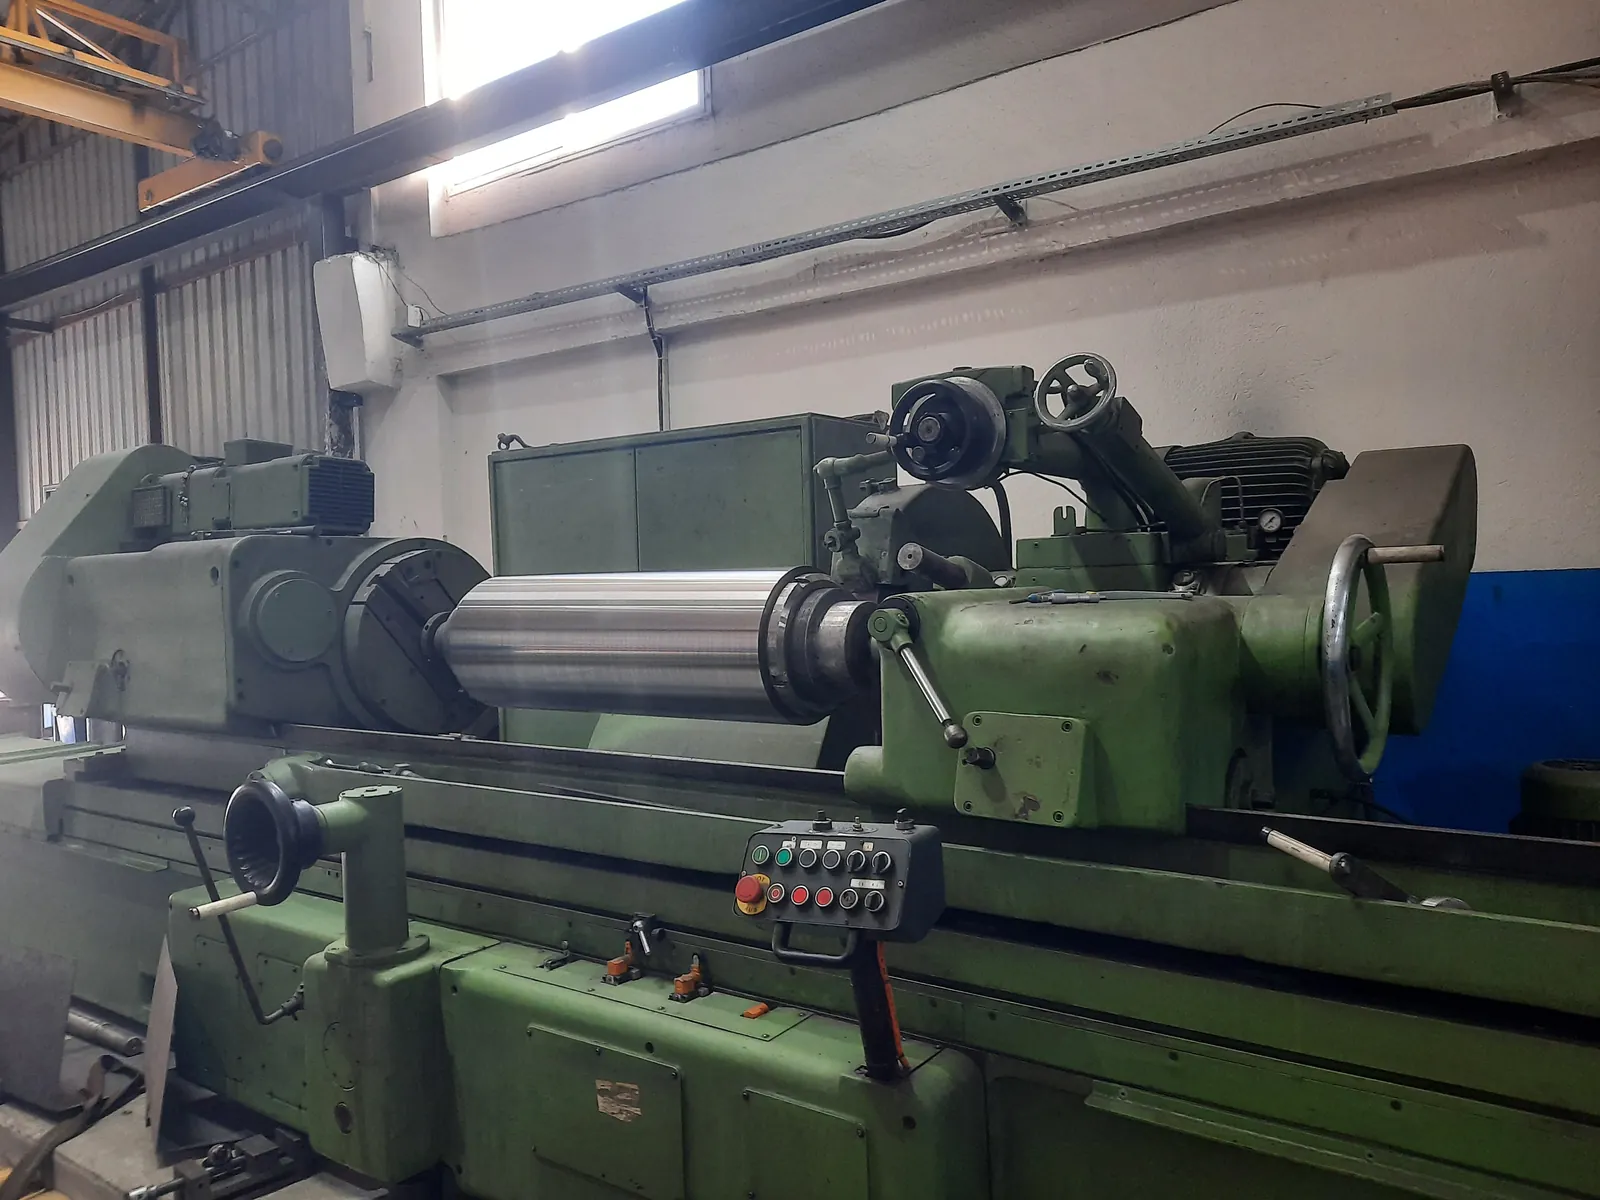
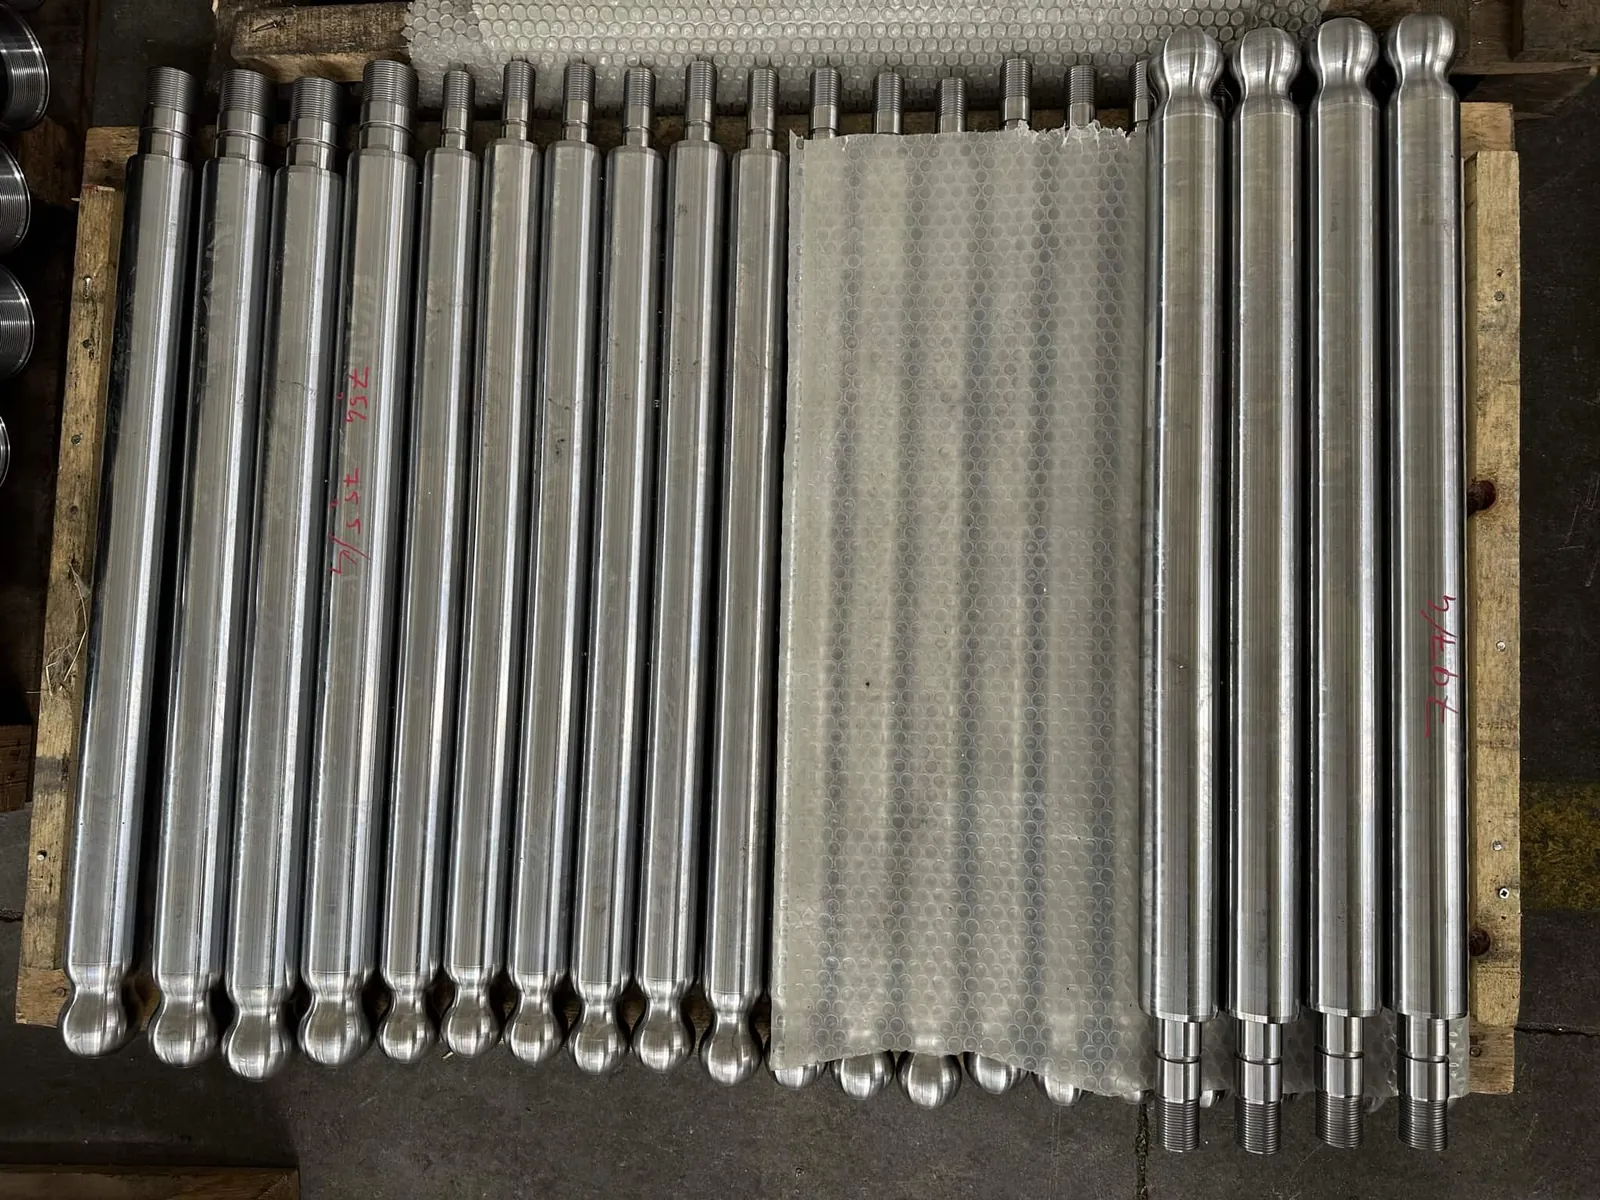
Ground and Chrome-Plated Rolls and Rods
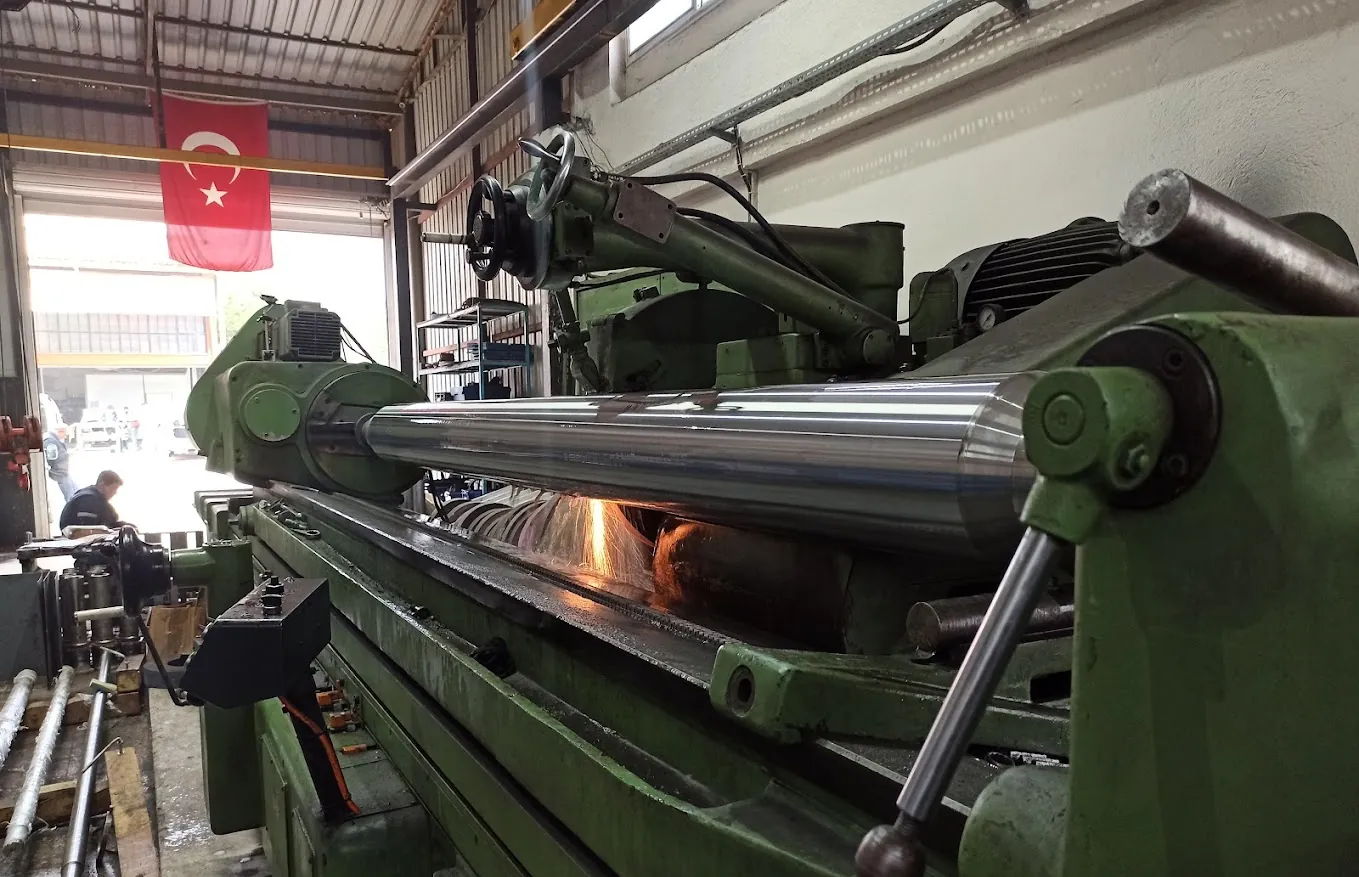
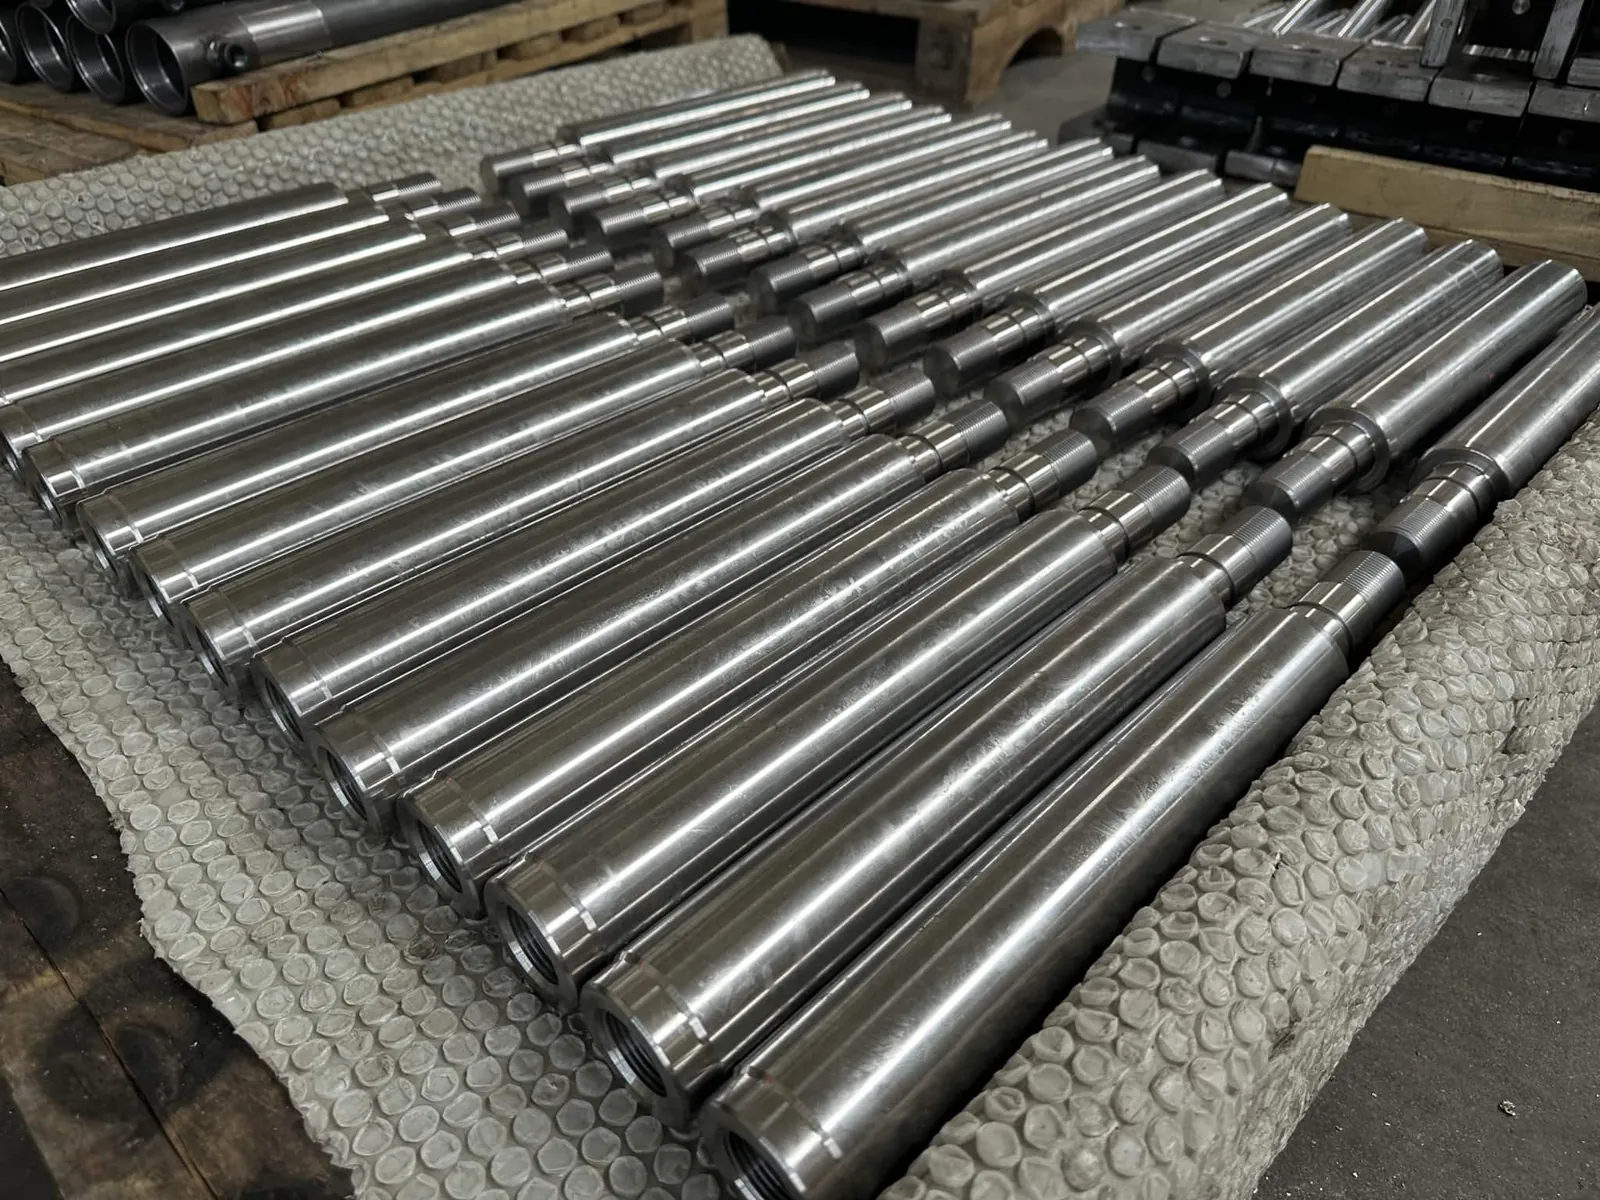
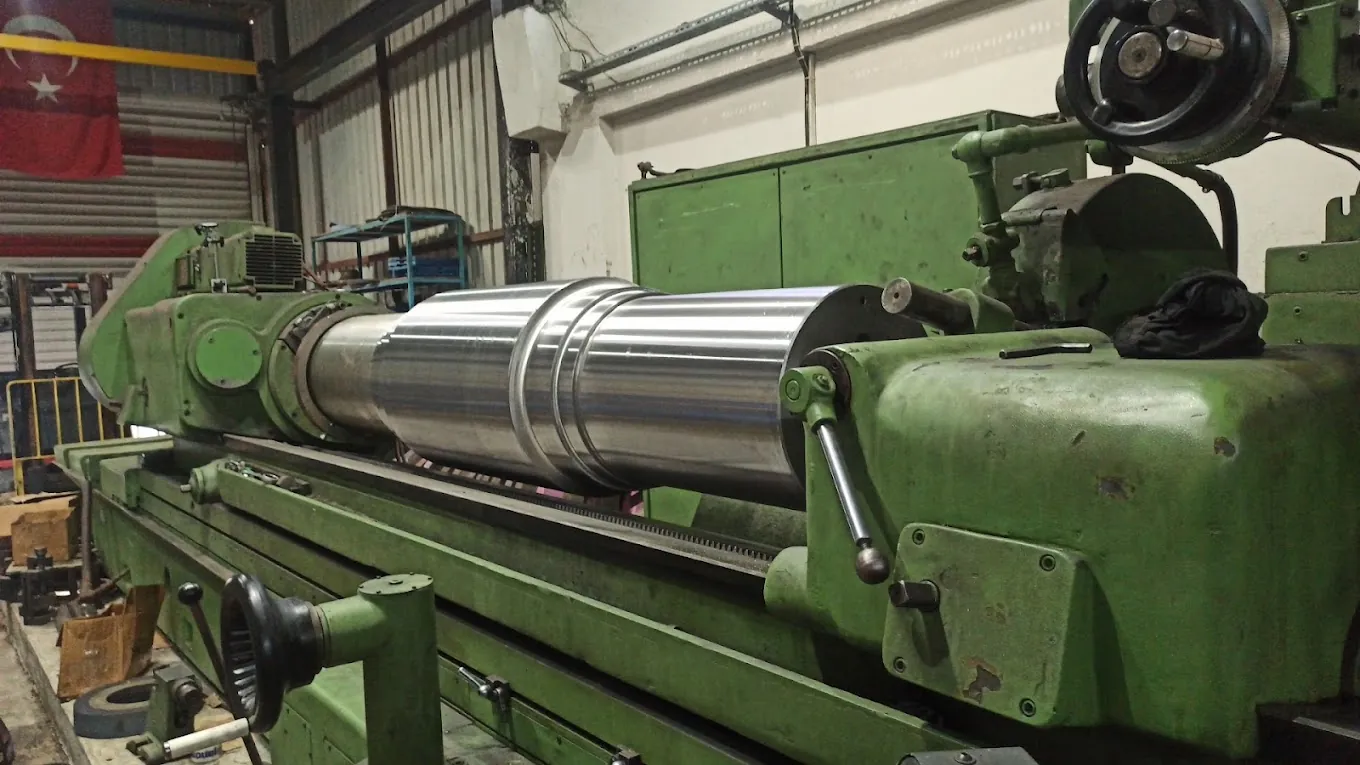
A Hard, Smooth, Corrosion-Resistant Roll Surface
Hard chrome is an electroplated layer of chromium on the steel surface of a roll. It is much harder than the base steel, has low friction, resists corrosion and can be polished to a very smooth finish. That makes it the standard surface for rolls that run against paper, film, textiles, rubber or metal strip, and for piston rods that run through seals.
- High surface hardness and wear resistance
- Corrosion resistance in wet and chemical environments
- Low friction and release properties
- Mirror, satin or matte finishes after grinding and polishing
- Can be stripped and renewed when worn, saving the roll body
How a Hard Chrome Roll Is Made
Pre-grinding
The roll body is ground to an undersize that leaves exactly the plating allowance.
Preparation
Areas that must not be plated are masked; the surface is cleaned and activated.
Plating
The roll is plated in our hard chrome tanks, with current matched to the surface area.
Finish-grinding
After plating, the roll is ground to final size, runout and surface finish.
Polishing
Where specified, the chrome is polished to the required gloss or roughness.
Inspection
Size, runout, surface finish and chrome layer are checked and documented.
Hard Chrome Plating Capacity
Our standard tanks cover rolls up to Ø1,300 mm × 1,500 mm and long rolls up to Ø900 mm × 5,000 mm, with rectifiers from 3,000 A to 25,000 A. Larger rolls up to Ø3,200 mm are plated on request. The full tank list is on our machine park page.
| Maximum diameter | Up to Ø3,200 mm |
|---|---|
| Standard tanks | Ø1,300 × 1,500 mm, Ø900 × 5,000 mm, Ø900 × 3,600 mm, Ø800 × 3,000 mm, Ø750 × 1,500 mm |
| Rectifiers | 3,000 A to 25,000 A |
| Stripping tank | 1,000 × 1,100 × 3,000 mm, for rechroming |
| Grinding | Before and after plating, 0.01 mm size and runout |
| Finish | Down to Ra 0.2 µm; polished on request |
| Parts | Rolls, shafts, piston rods, plungers, cylinders |
Where Hard Chrome Rolls Run
Paper & converting
Calender, press, guide and coating rolls.
Learn more →Film, printing & packaging
Chill, embossing, laminating and guide rolls.
Learn more →Steel & metal processing
Process, pinch and guide rolls for strip lines.
Learn more →Hydraulics
Chrome-plated piston rods and plungers.
Learn more →Food processing
Chrome rolls for dough, confectionery and food lines.
Learn more →Textile & rubber
Calender and process rolls for textile and rubber lines.
Questions About Hard Chrome Rolls
What size rolls can you hard chrome plate?
Up to Ø3,200 mm. Standard tanks take rolls up to Ø1,300 × 1,500 mm and long rolls up to Ø900 × 5,000 mm; larger rolls are plated on request.
Do you grind rolls before and after chrome plating?
Yes. Rolls are pre-ground to the plating allowance, plated, then finish-ground to final size, runout and surface finish.
Can you rechrome worn rolls?
Yes. We strip the old chrome in our stripping tank, regrind the base, replate and finish-grind the roll.
What surface finish can you achieve?
Ground surface finish down to Ra 0.2 µm, with polishing to higher gloss on request.
Do you chrome-plate piston rods?
Yes. We hard chrome plate and grind piston rods and plungers for hydraulic cylinders.
Hard Chrome Rolls From One Supplier: Grinding, Plating and Finishing
Hard chrome plating is never just plating. A good chrome roll depends on the grinding before the tank, the plating itself and the grinding and polishing afterwards. When these steps happen in different companies, the roll travels back and forth and nobody owns the final result. We run the whole sequence ourselves, on our own grinders and in our own chrome tanks.
New chrome rolls
We supply new hard chrome rolls built from scratch: shell or solid body, shafts and journals, plating and finishing. See large diameter rollers and press, calender and guide rolls for typical designs.
Rechroming worn rolls
Chrome wears, scratches and corrodes over time, but the roll underneath is usually still good. Rechroming strips the old layer, regrinds the base, replates and finish-grinds the roll, at a fraction of the cost of a new one. It is a core part of our roller repair and refurbishment service.
Chrome for hydraulics
The same tanks and grinders produce chrome-plated piston rods in series, and our bore honing machines finish the cylinder barrels they run in. Send your roll or rod drawing via the contact page.